
Featured Drill & Tap Processing Solutions
Core tooling solutions designed to maximize accuracy, cycle efficiency, and process stability in industrial tapping centers.

The Evolution of CNC Drill and Tap Processing
In modern metal cutting operations, drilling and thread tapping represent mission-critical stages that frequently serve as the final mechanical operations on high-value components. A modern tapping machine for CNC drill and tap processing is no longer merely a basic mechanical unit driven by geared spindles. Instead, it has transformed into an advanced precision mechatronics platform featuring ultra-responsive synchronous rigid servo drives, adaptive high-speed peck cycles, and micron-level position feedback.
Historically, threading operations suffered from significant bottlenecks caused by pitch mismatch, spindle reversal delays, and frequent tool breakage from uneven chip load. Modern tapping machine systems integrate high-torque direct-drive spindles with dynamic synchronization to lock axial feed rates precisely with rotational velocity. This technological advancement eliminates thread pitch distortion and prevents catastrophic tool failure even when operating at surface speeds exceeding 60 meters per minute in tough alloys.
- Sub-millisecond spindle orientation and seamless rapid forward-reverse reversal
- Dynamic pitch matching preventing axial distortion on ultra-fine thread geometries
- Direct integration with solid carbide internal-cooling drill and tap assemblies
Industrial Demands Across Critical Sectors
How advanced CNC tapping machines and precision tooling resolve complex manufacturing challenges across global high-reliability industries.
EV Powertrains & Battery Trays
Lightweight automotive engineering demands the mass drilling and high-speed tapping of hundreds of M4 to M10 threaded holes in thin-walled, extruded aluminum battery structural trays and transmission cases. In these environments, tapping machines must deliver high acceleration rates (exceeding 1.5G) and dependable chip evacuation to completely avoid burr formation and thread striping.
Aerospace Superalloys
Machining Inconel 718, Titanium Ti-6Al-4V, and high-temperature nickel alloys presents extreme work-hardening challenges. Specialized CNC drill and tap centers leverage rigid synchronous tapping with through-spindle high-pressure cutting fluid delivery (up to 70 Bar) and torque monitoring to tap deep blind holes without catastrophic tap shear.
3C Electronics & Enclosures
For smartphones, laptops, and precision telecommunication frames, small-hole tapping (M0.8 to M2.5) demands exceptionally delicate touch sensing, instant spindle deceleration, and micro-concentric runout tooling. Even minimal vibration or backlash can ruin micro-threads in premium anodized aluminum alloy housings.
Key Technological Trends in Drill & Tap Systems
The synergy of AI intelligence, sensorized machine spindles, and advanced cutting tool geometry.
AI Adaptive Torque Monitoring
Contemporary tapping machine units incorporate AI-assisted spindle load analytics that evaluate instantaneous current draw signatures during every millisecond of thread engagement. If tool wear or swarf clogging causes a micro-spike in cutting resistance, the system autonomously adapts feed speed, triggers an instantaneous peck retract, or flags predictive tool replacement.
High-Torque Synchronous Spindles
Eliminating intermediate belt or planetary gear backlash, direct-drive integrated motor spindles provide rapid acceleration up to 24,000 RPM for solid carbide micro-drilling, immediately decelerating and orienting for ultra-precise thread tapping cycles. This drastically shortens non-cutting cycle times across multi-hole components.
Advanced Through-Tool Coolant
Modern tapping processes rely heavily on cryogenic or high-pressure micro-lubrication (MQL) delivered straight through the tool holder and tapping flute. This internal thermal regulation rapidly dissipates friction-induced heat, extends tap durability up to 300%, and forces compacted swarf away from blind hole bottoms.
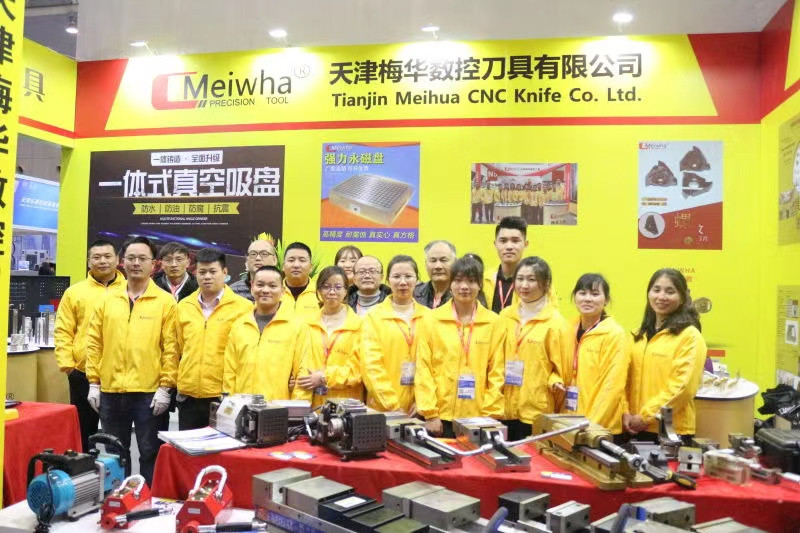
Tianjin MeiWha Precision Machinery Co., Ltd.
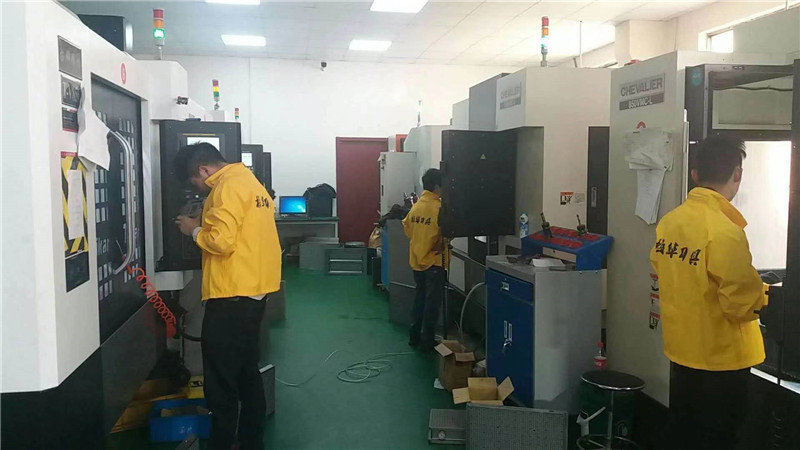
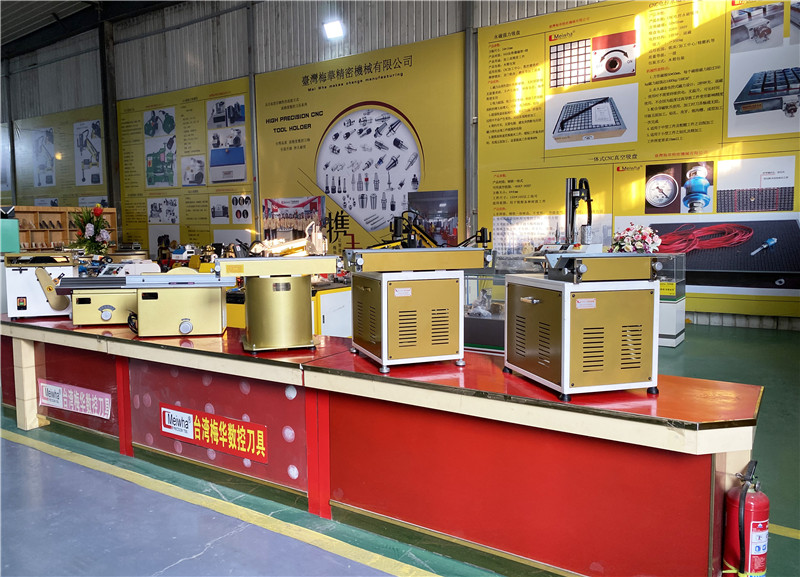
Tianjin MeiWha Precision Machinery Co.,Ltd was founded in June 2005. It is a professional manufactory which engaged in all kinds of NC cutting tools, include Milling tools, Cutting Tools, Turning Tools, Tool holder, End Mills, Taps, Drills, Tapping Machine, End Mill Grinder machine, Measuring tools, Machine tool accessories and other products.
Our standard tools meet the highest quality standards, which we have been able to prove a million times to satisfied customers since 2005. With our mature product portfolio we offer solutions for the tasks around drilling, milling, countersinking and reaming. With high commitment and ambition we continue to develop and optimize our solid carbide line. The excellent technical properties as well as the availability which can be viewed online offer our customers and partners the best conditions for optimizing their processes.
Our company is located in Jingzhong Industrial park, Dongli District, Tianjin, covering an area of more than 5000 square meters, with 1500 square meters of modern office space. Branches, direct stores, subordinate branch agents or special distributors are arranged in various regions to form outlet distribution services. At the same time, Meiwha products export include Dubai, The United Arab Emirates, Switzerland, France, South Africa, India, The Philippines, Thailand and so on.
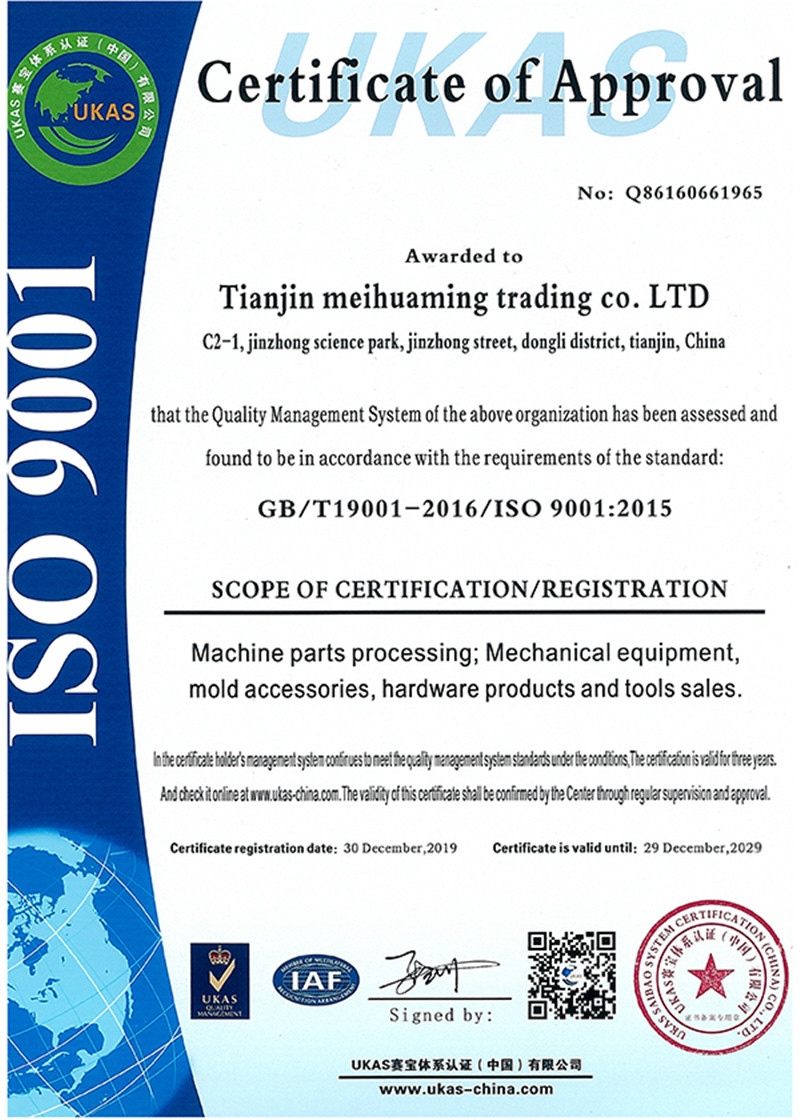
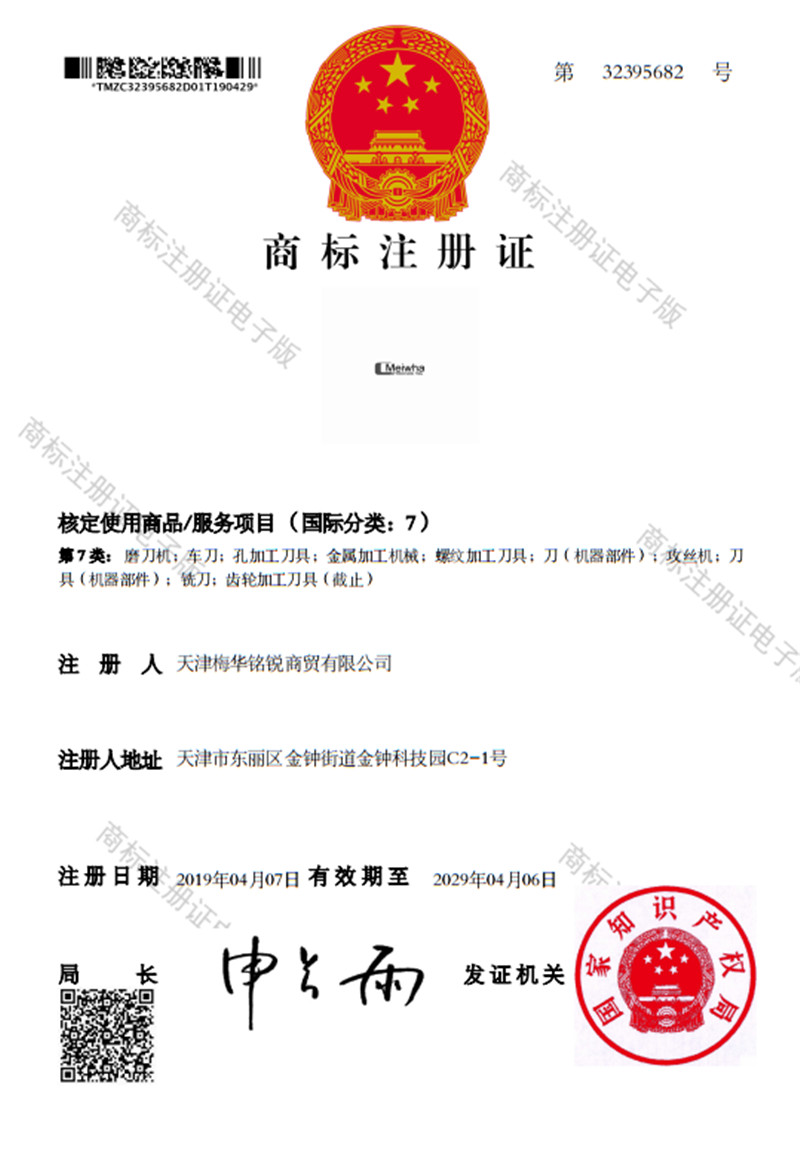
Our Advantages & Recognized Qualifications
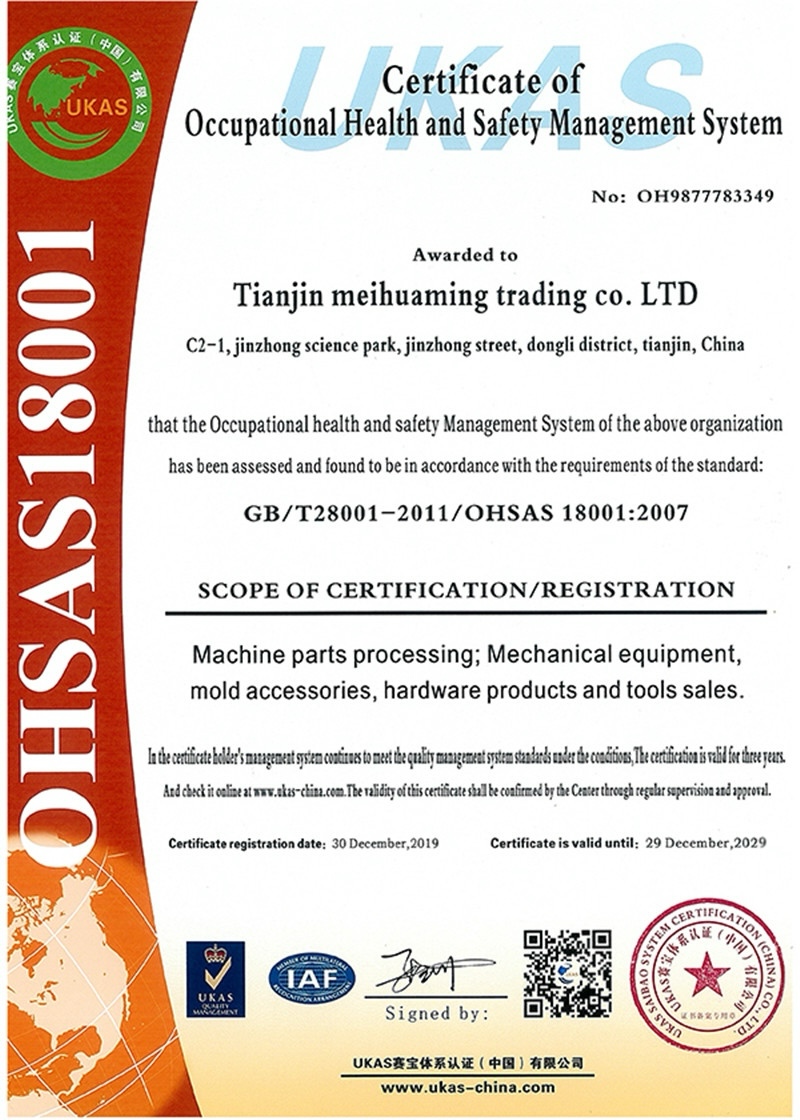
The company combines industry advantages, integrates product resources, and inherits all customer-oriented business concepts, only provides customers with the right products, and provides customers with one-stop procurement services. At the same time, with excellent product quality, precise delivery time, reasonable and competitive prices, it has won the approval of the industry and the support of our customers. It has established long-term strategic cooperation with many domestic and foreign research institutes and enterprises, such as Tianjin Jinhang Institute of Physics and Beijing Fangshan Bridge 14th Bureau. The company will further rely on its own advantages and strong strength, exert a better good brand effect, adhere to the quality policy of "providing customers with satisfactory products with continuous improvement in management and technology", and strive to provide better products and services to new and old customers at local market and abroad.
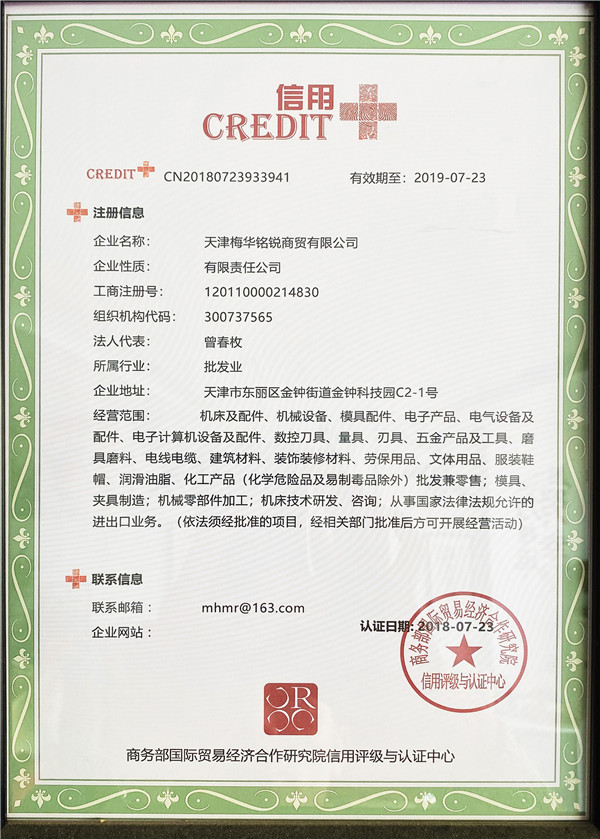
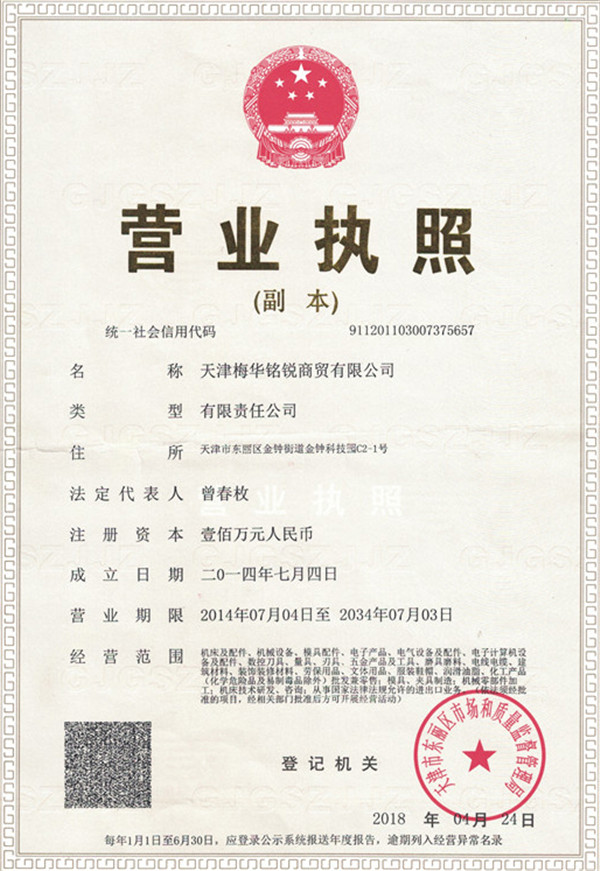
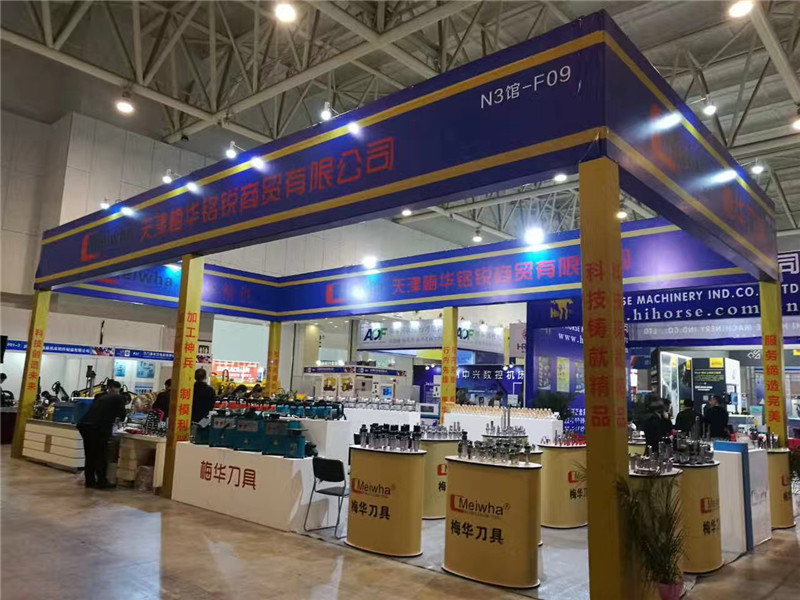
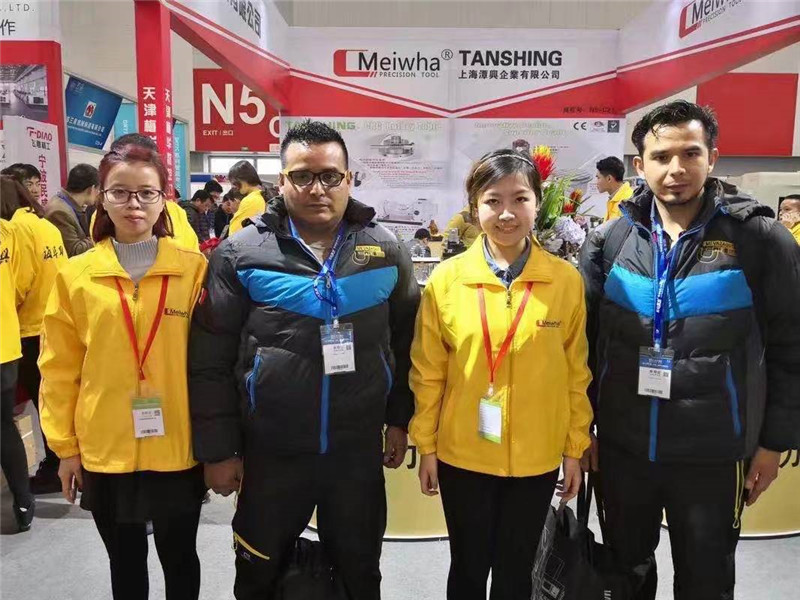
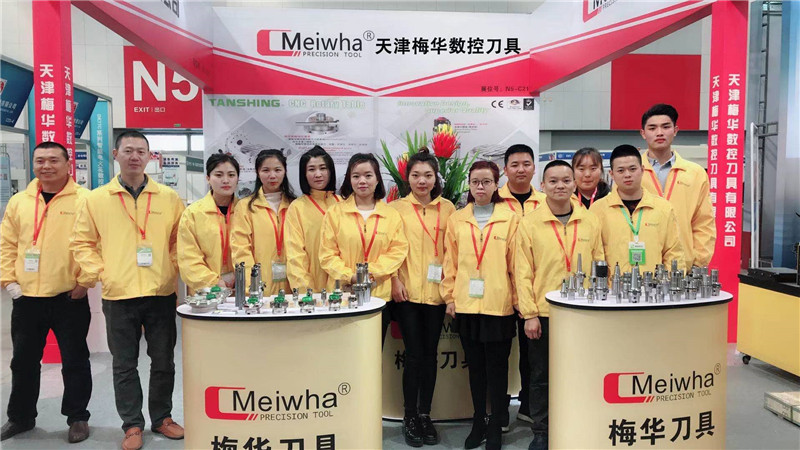
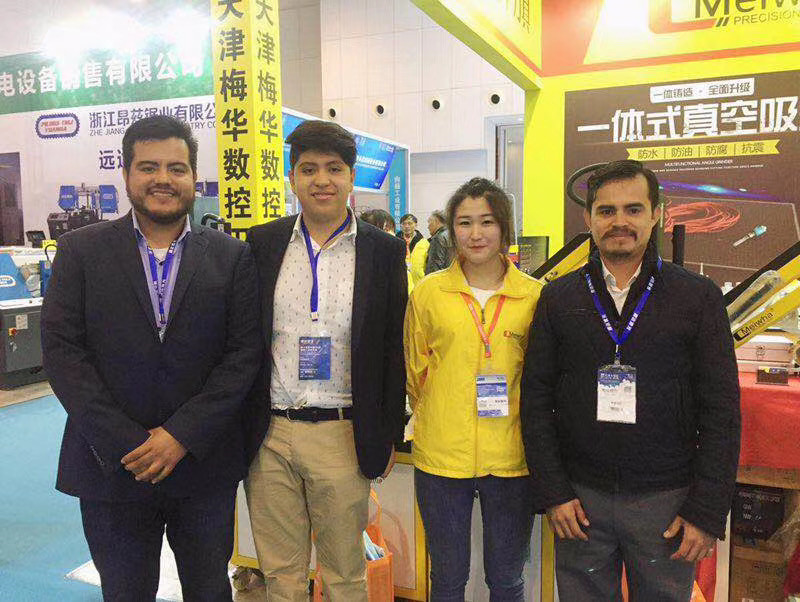
International Trade Exhibitions
Showcasing state-of-the-art cutting tools, tapping fixtures, and CNC processing systems to global manufacturing leaders.
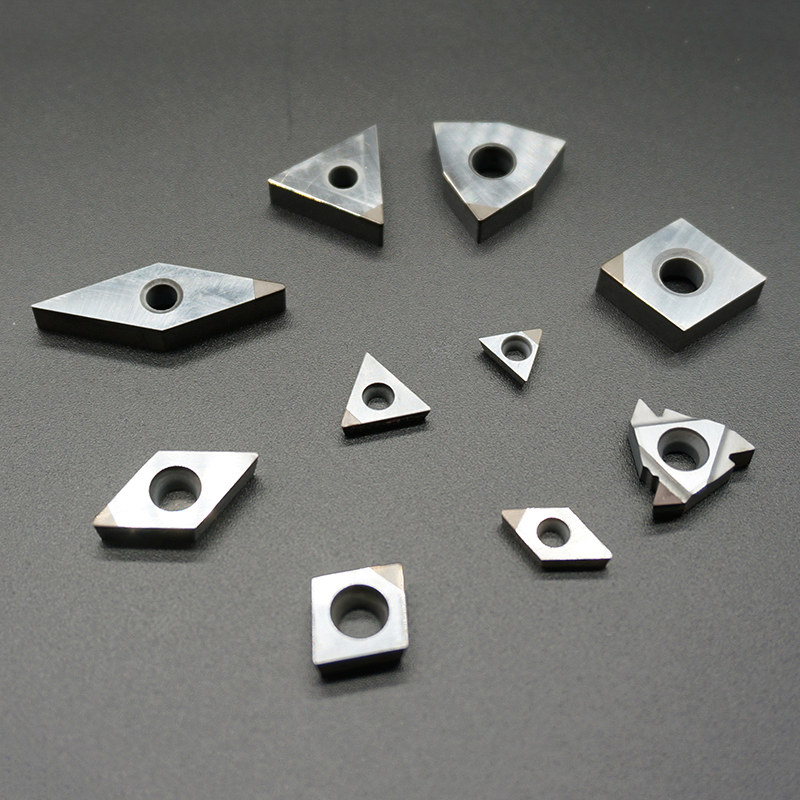
Engineered Tooling & Inserts Portfolio
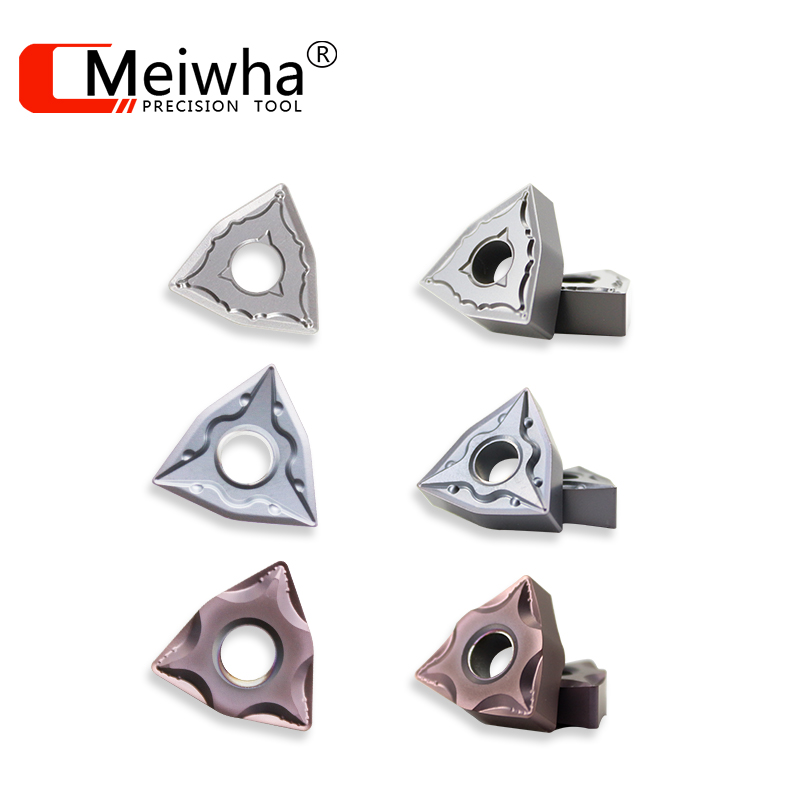
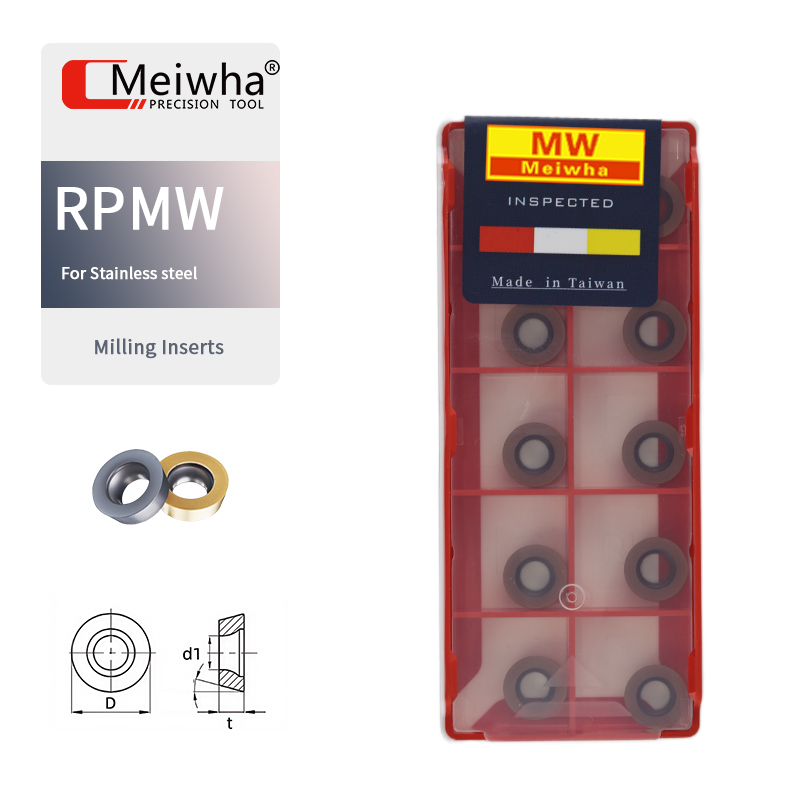
Complementary high-performance inserts, cleaner attachments, and cutting materials engineered for unified drill and tap centers.
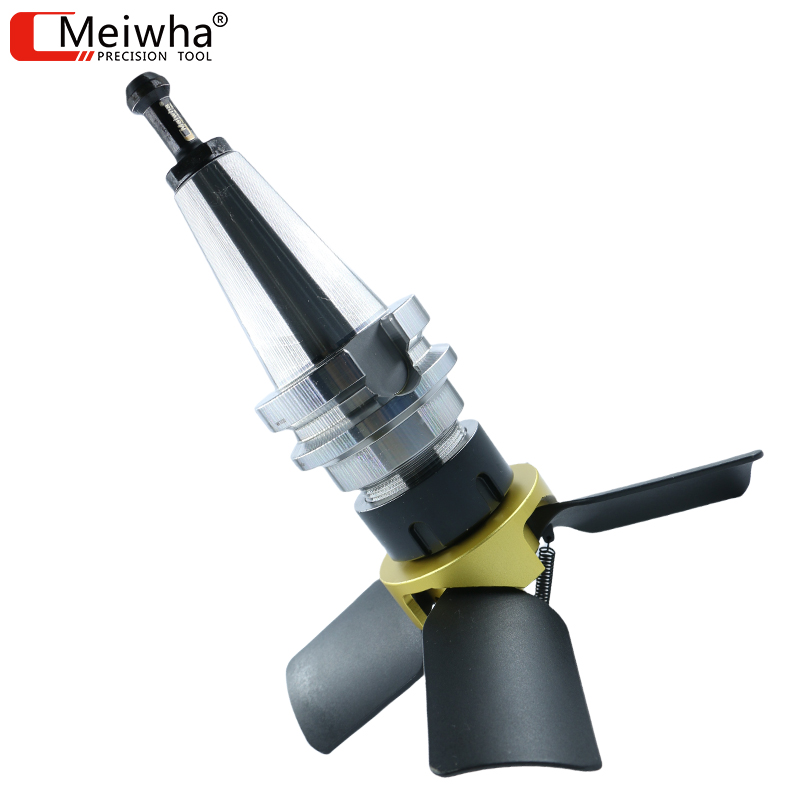
Featured Drill & Tap Machine Tool Holders
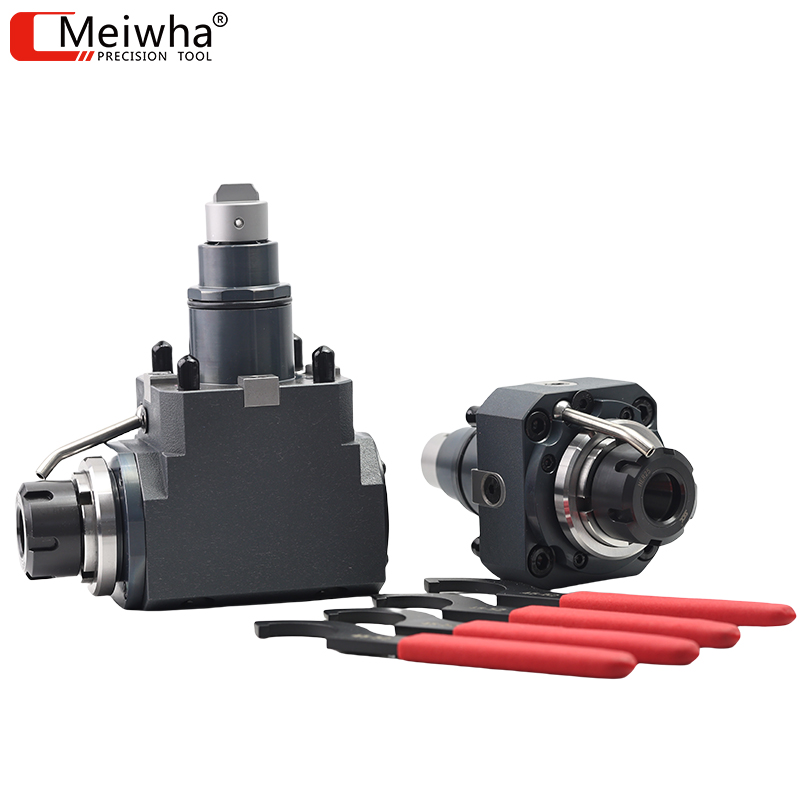
Top-tier spindle clamping systems, shrink-fit extension rods, and driven heads ensuring zero radial slippage and minimum runout.


Achieving Peak Quality in CNC Drill and Tap Operations
Key operational parameters for engineering workshops striving for zero-defect threading output.
Pre-Hole Sizing and Chamfer Accuracy
Thread stripping and tap fractures are predominantly triggered by improper pre-hole drilling diameters. Maintaining precise hole tolerance before running the tapping machine ensures uniform chip load distribution across every chamfered cutting teeth. Employing high-rigidity solid carbide drills minimizes diameter variation, while dedicated chamfer tools like the MW-800R prepare lead surfaces that eliminate burrs and protect delicate tap entries.
Concentricity and Toolholder Selection
Runout deviation above 0.005mm severely impairs tap wear life and causes pitch flank deviation. Implementing high-precision shrink-fit tool holders or specialized synchro tapping chucks absorbs micro-axial deviations and preserves perfect center alignment between the spindle axis and hole centerlines, dramatically improving thread finish and dimensional conformity across high-volume production cycles.


-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China