
Precision High-Speed Cutting Tool Solutions
Engineered for extreme RPM applications, superior holding torque, and supreme tool rigidity
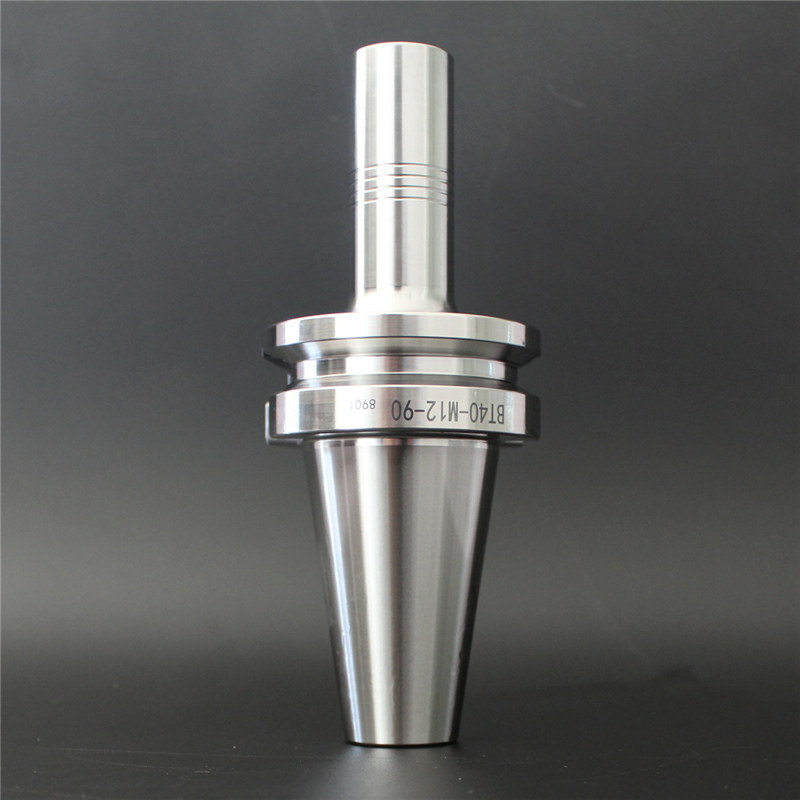
Industrial Landscape: The Evolution of CNC Shrink Fit Tool Holders in HSC
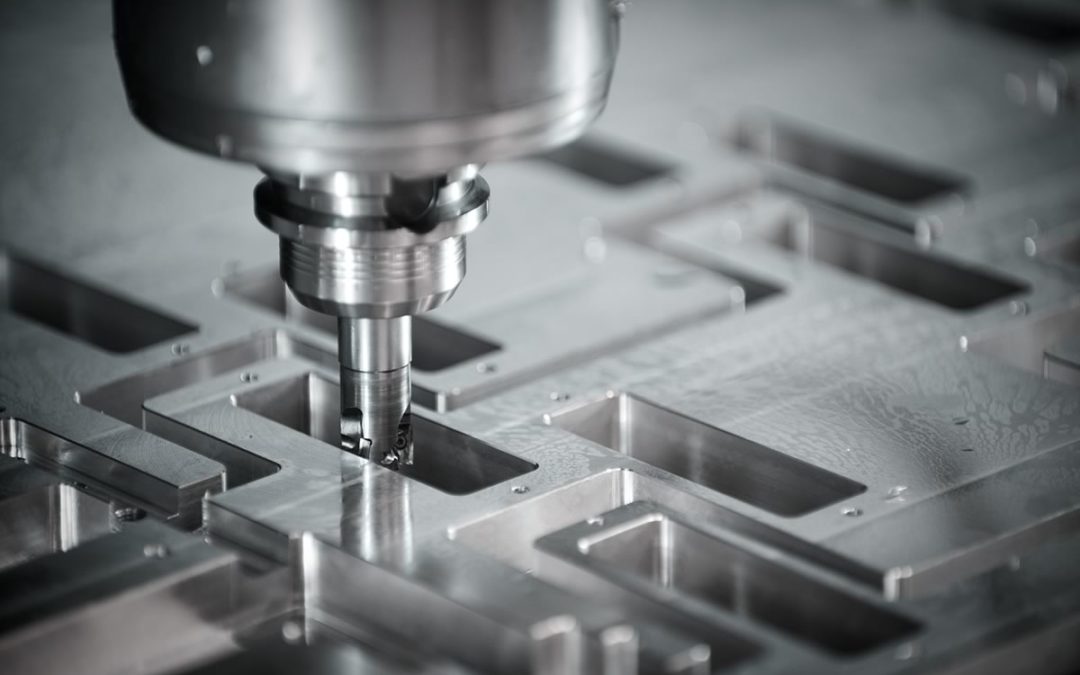
In contemporary manufacturing, the demand for High-Speed Cutting (HSC) and High-Performance Cutting (HPC) has surged dramatically. Modern machine tools consistently operate at spindle speeds exceeding 20,000 to 45,000 RPM, working with difficult-to-machine alloys like titanium, Inconel, hardened die steels, and reinforced composites. In this demanding operational theater, the connection interface between the machine spindle and the cutting tool is critical. Traditional clamping mechanisms, such as collet chucks or side-lock Weldon holders, often introduce geometric eccentricities, high radial runout, and asymmetrical mass distributions that trigger catastrophic harmonic vibration at ultra-high rotational velocities.
A CNC shrink fit tool holder solves these engineering bottlenecks through thermal expansion principles. Utilizing high-frequency induction heating units, the bore of the toolholder expands within seconds to receive the cutting tool shank. Upon cooling, the symmetrical hoop stress produces a 360-degree uniform grip along the entire bore contact area. This seamless coupling delivers unmatched clamping torque, balanced mass distribution, and runout precision within 3 microns (0.003mm). Consequently, shrink fit technology has established itself as the premier clamping mechanism for high-speed finish milling, deep cavity micro-machining, and complex 5-axis aerospace contouring.
≤0.003mm Ultra-Precision Runout
Full 360-degree symmetrical contraction provides unmatched concentricity, minimizing chip load variability across every cutter flute.
Superior Dynamic Balancing
Factory balanced to G2.5 at 25,000 to 30,000 RPM, protecting spindle bearings from cyclic radial chatter and premature wear.
Slim Profile & Deep Reach
Streamlined nose contours eliminate bulky nuts and collet collars, facilitating high-speed 5-axis clearance in deep mold cavities.
Engineering Mechanics & Technological Superiority in HSC Applications
Dynamic stability during high-speed cutting dictates cutting edge life and surface integrity. At high rotational velocities, centrifugal forces tend to open traditional collet slots, significantly decreasing holding force and permitting microscopic tool micro-slippage. In contrast, thermal shrink fit chucks rely on high-grade hot-working tool steels possessing superior thermal recovery resilience, high yield strength, and anti-fatigue endurance. The gripping pressure generated by thermo-contraction can exceed 1000 N·m of clamping force, firmly locking solid carbide end mills in place.
Furthermore, the uniform material geometry dampens harmonic resonance. Radial runout of less than 0.003mm ensures uniform wear distribution across cutting edges. This delivers up to a 200% to 300% extension in tool life, drastically improves Ra surface finish, and eliminates secondary polishing in precision mold and die operations.
| Performance Metrics | CNC Shrink Fit Tool Holder | Precision ER Collet Chuck | Hydraulic Expansion Chuck |
|---|---|---|---|
| Runout Accuracy (T.I.R. at 3xD) | < 0.003 mm (0.0001") | 0.008 – 0.015 mm | < 0.003 mm |
| Clamping Force / Torque | Extremely High (Uniform 360°) | Moderate to Low | High |
| Interference Profile / Clearance | Slim / Ultra-Thin Contour | Bulky (Clamping Nut Required) | Bulky (Internal Fluid Chamber) |
| Balancing Capability | G2.5 up to 30,000+ RPM | G6.3 / G2.5 (Limited to <15,000 RPM) | G2.5 up to 20,000 RPM |
| Bending Rigidity | Maximum Solid Monoblock | Multi-Component Assembly Loss | Moderate (Internal Bladder) |
Key Industry Application Scenarios
1. Aerospace Blisk & Turbine Impeller Machining
Aerospace blisks and complex structural impellers demand 5-axis continuous trajectory milling of tough titanium (Ti-6Al-4V) and nickel-base superalloys. The ultra-slim contours of shrink fit tool holders allow maximum accessibility into tight blade channels without machine head collisions, maintaining structural stiffness throughout full-depth trochoidal milling passes.
2. Precision Die & Mold Manufacturing
Hardened tool steels exceeding 55 to 65 HRC require micro-end mills operating at rotational speeds upwards of 30,000 RPM. Any radial deflection instantly causes tool chipping and surface deviations. Shrink fit tool holders ensure continuous edge tracking, generating mirror-like surface finishes (Ra < 0.2 µm) directly from CNC finishing cycles.
3. Automotive & Medical Component Production
In high-throughput automotive production lines and orthopedic implant manufacturing (e.g., cobalt-chrome knee joints and titanium bone plates), process repeatability and rapid cycle times are paramount. Shrink fit setups achieve fast tool changeouts in seconds via automatic induction units, ensuring dimensional repeatability across high-volume production batches.
About MeiWha Precision Machinery
Over 18 years of pioneering excellence in CNC tool manufacturing, research, and global distribution
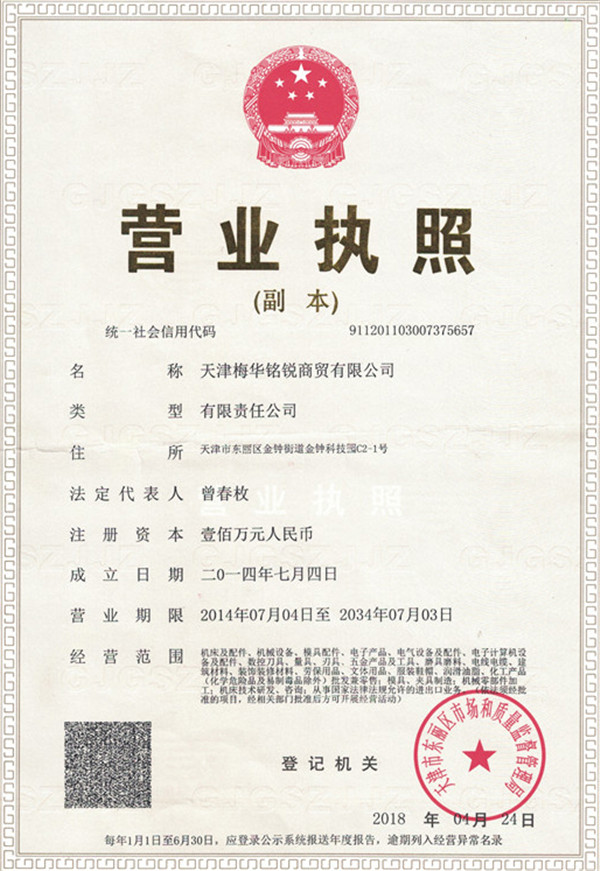
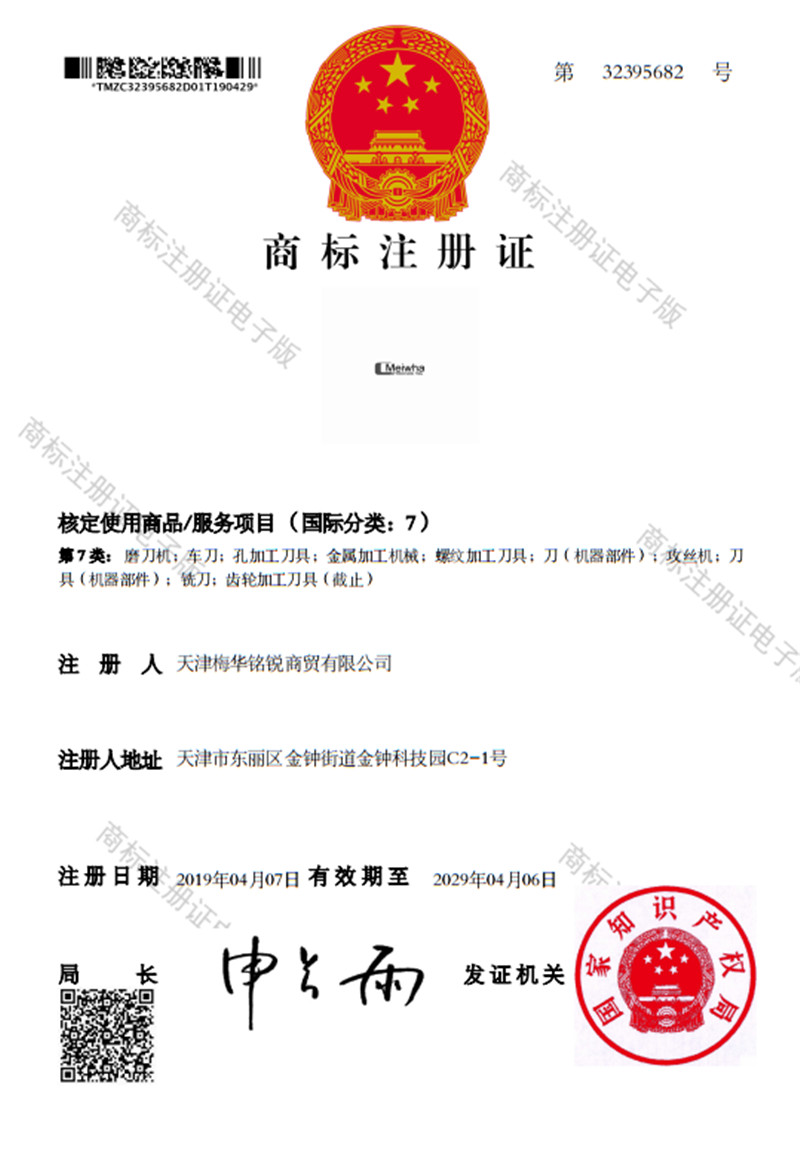
Tianjin MeiWha Precision Machinery Co., Ltd.
Tianjin MeiWha Precision Machinery Co.,Ltd was founded in June 2005. It is a professional manufactory which engaged in all kinds of NC cutting tools, include Milling tools, Cutting Tools, Turning Tools, Tool holder, End Mills, Taps, Drills, Tapping Machine, End Mill Grinder machine, Measuring tools, Machine tool accessories and other products.
Our standard tools meet the highest quality standards, which we have been able to prove a million times to satisfied customers since 2005. With our mature product portfolio we offer solutions for the tasks around drilling, milling, countersinking and reaming. With high commitment and ambition we continue to develop and optimize our solid carbide line. The excellent technical properties as well as the availability which can be viewed online offer our customers and partners the best conditions for optimizing their processes.
The company combines industry advantages, integrates product resources, and inherits all customer-oriented business concepts, only provides customers with the right products, and provides customers with one-stop procurement services. At the same time, with excellent product quality, precise delivery time, reasonable and competitive prices, it has won the approval of the industry and the support of our customers. It has established long-term strategic cooperation with many domestic and foreign research institutes and enterprises, such as Tianjin Jinhang Institute of Physics and Beijing Fangshan Bridge 14th Bureau. The company will with further rely on its own advantages and strong strength, exert a better good brand effect, adhere to the quality policy of "providing customers with satisfactory products with continuous improvement in management and technology", and strive to provide better products and services to new and old customers at local market and abroad.
Global Presence & Infrastructure
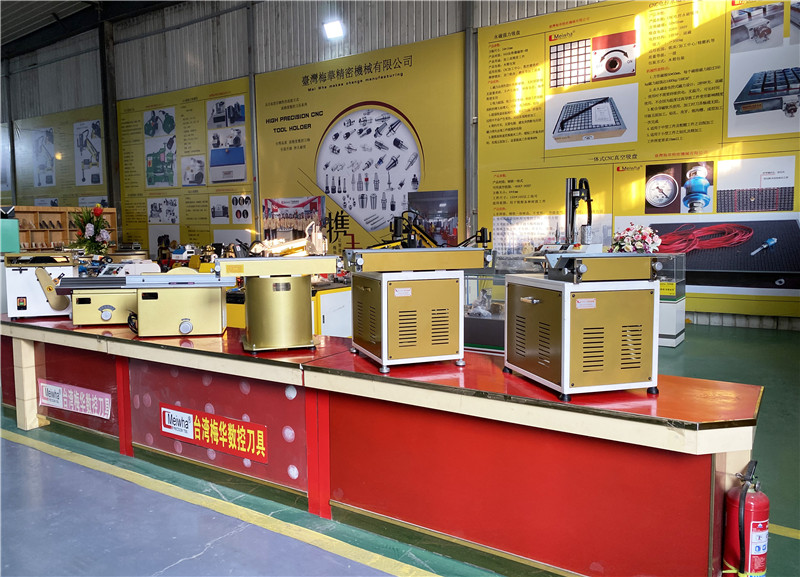
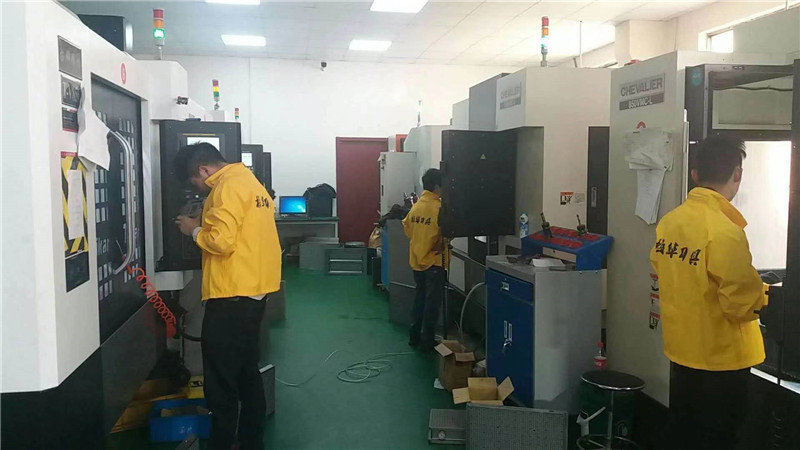
Our company is located in Jingzhong Industrial park, Dongli District, Tianjin, covering an area of more than 5000 square meters, with 1500 square meters of modern office space. Branches, direct stores, subordinate branch agents or special distributors are arranged in various regions to form outlet distribution services. At same time, MeiWha products export include Dubai, The United Arab Emirates, Switzerland, France, South Africa, India, The Philippines, Thailand and so on.
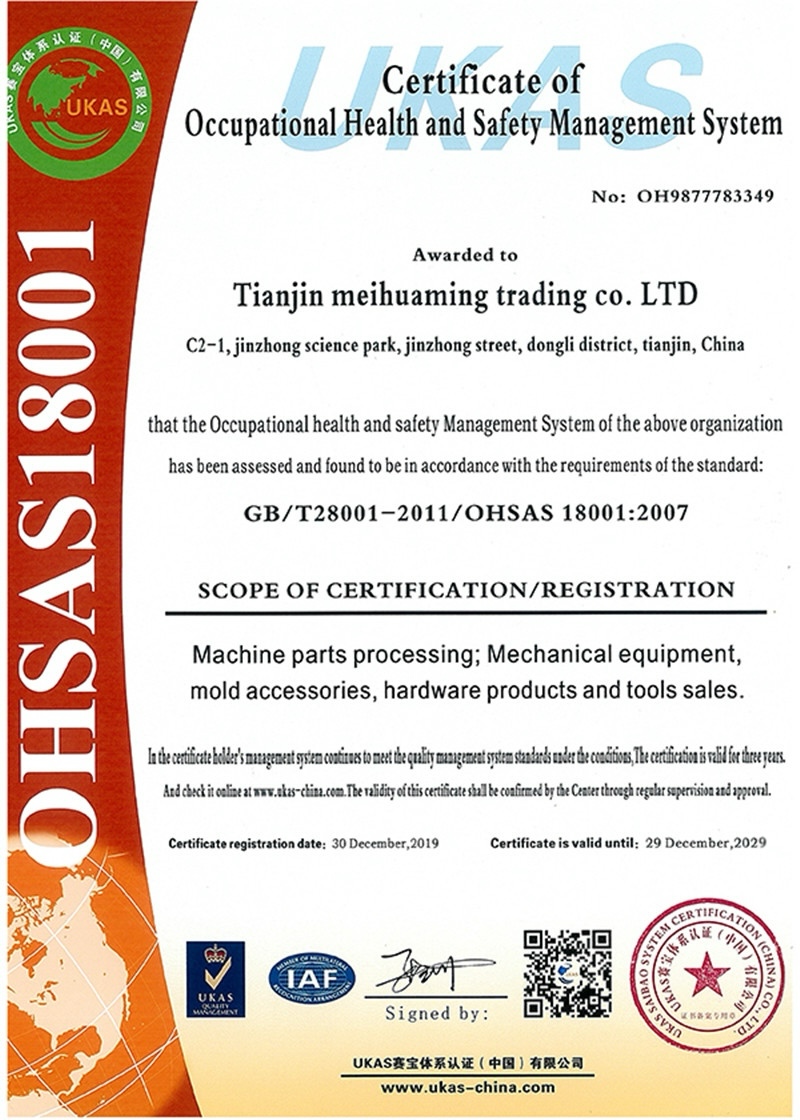
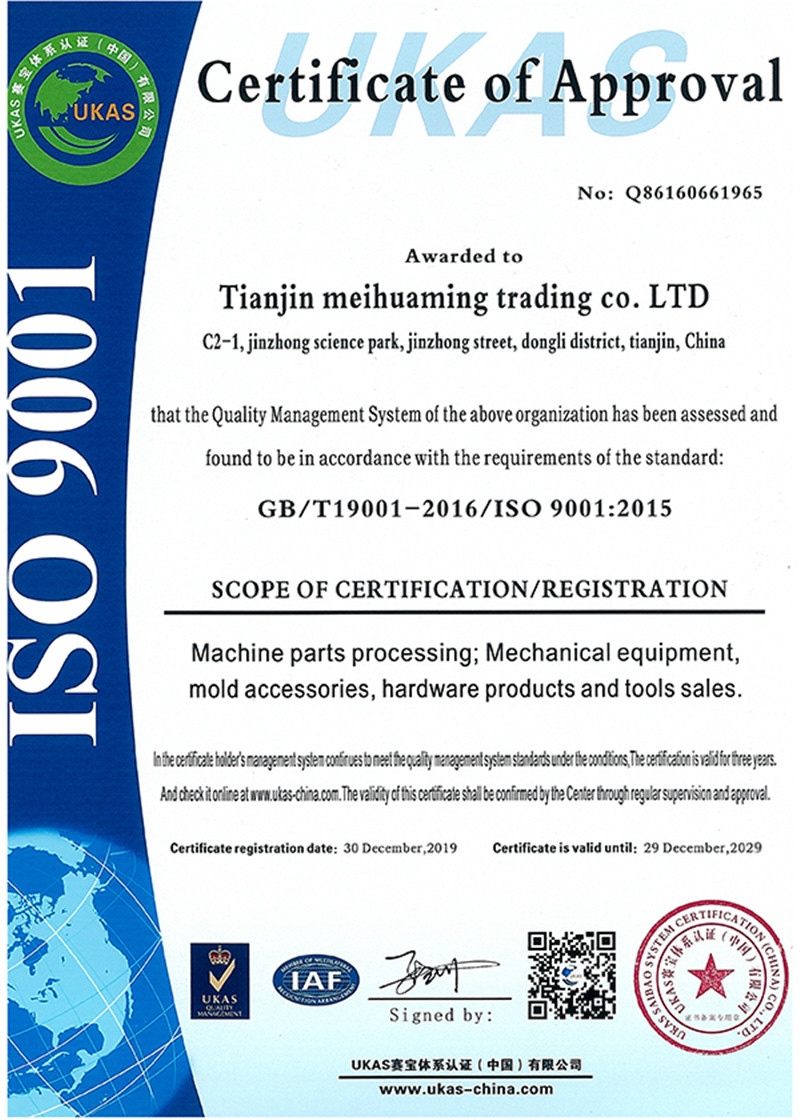
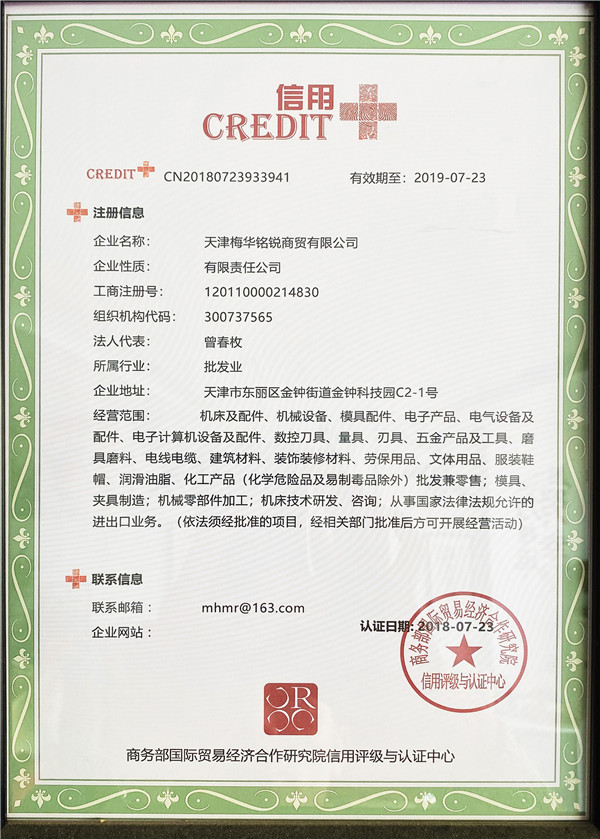
Enterprise Honors & Certifications
MeiWha Global Exhibitions & Industry Exchanges
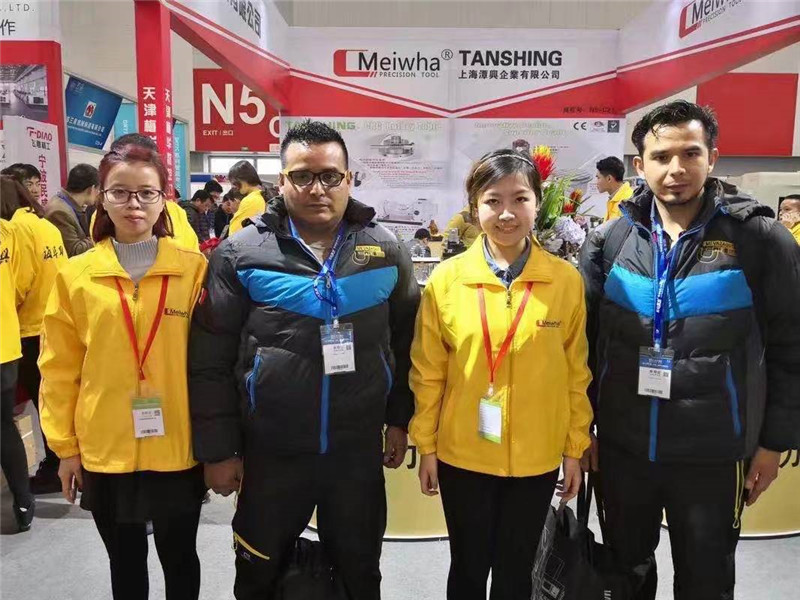
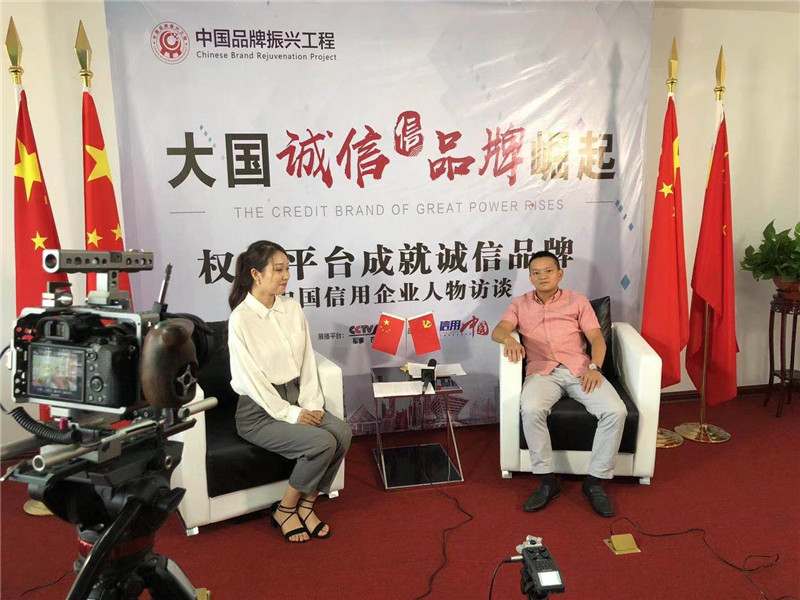
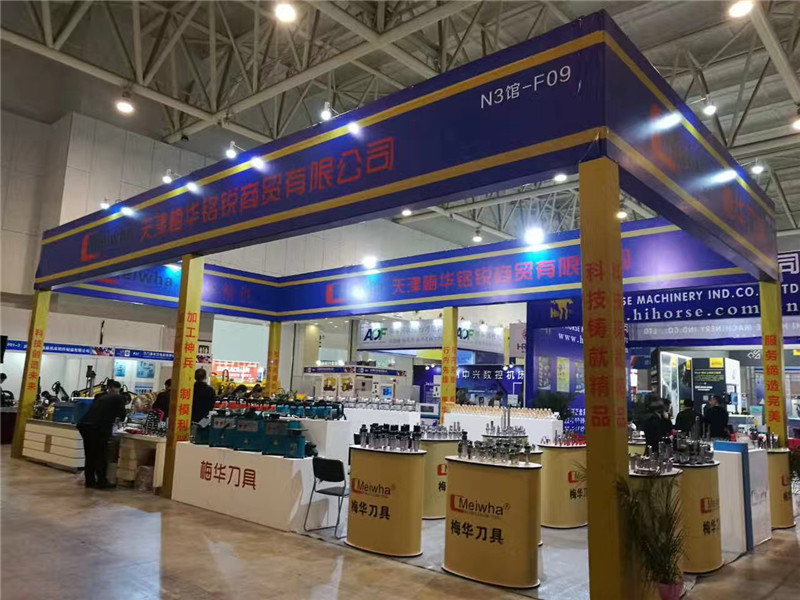
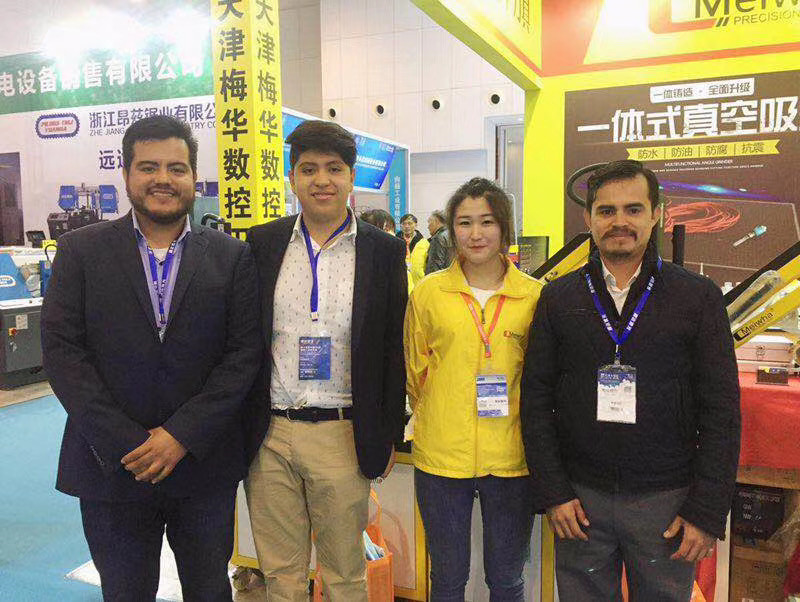
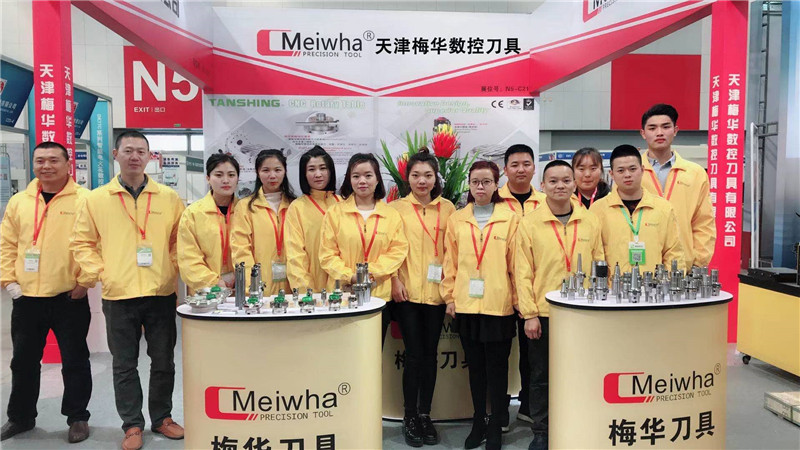
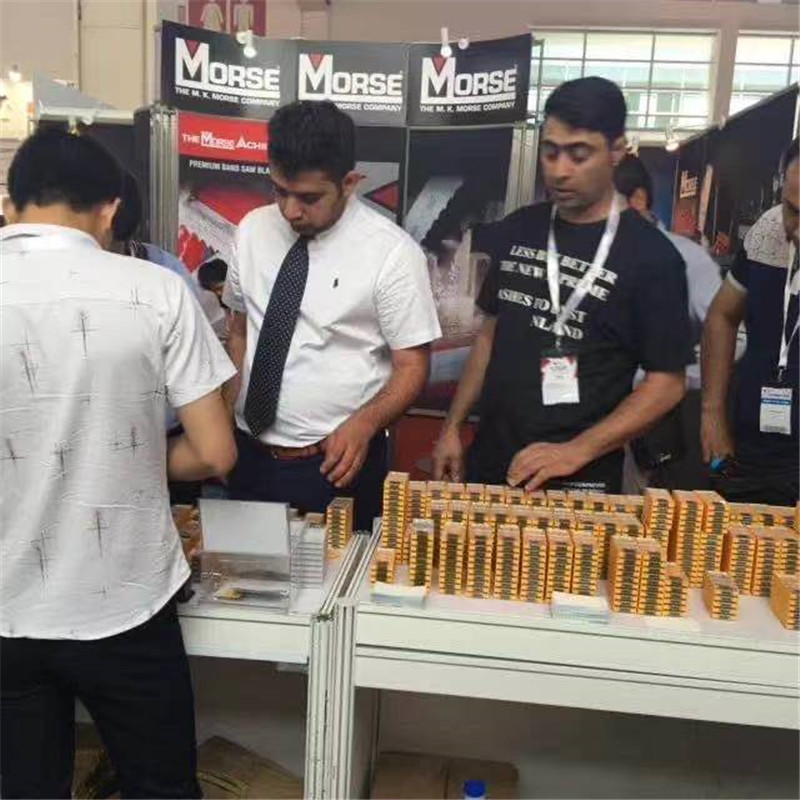
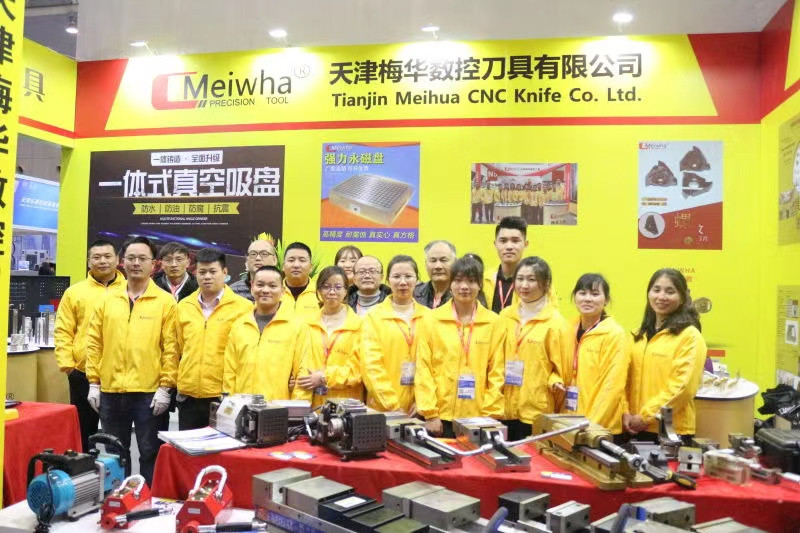
Demonstrating our technological achievements on global stages, MeiWha regularly participates in premier machine tool and manufacturing expos worldwide. Our technical specialists collaborate with machining professionals worldwide to demonstrate real-time high-speed machining using advanced shrink-fit tool holders, high-feed cutters, and specialized CNC accessory tooling systems.
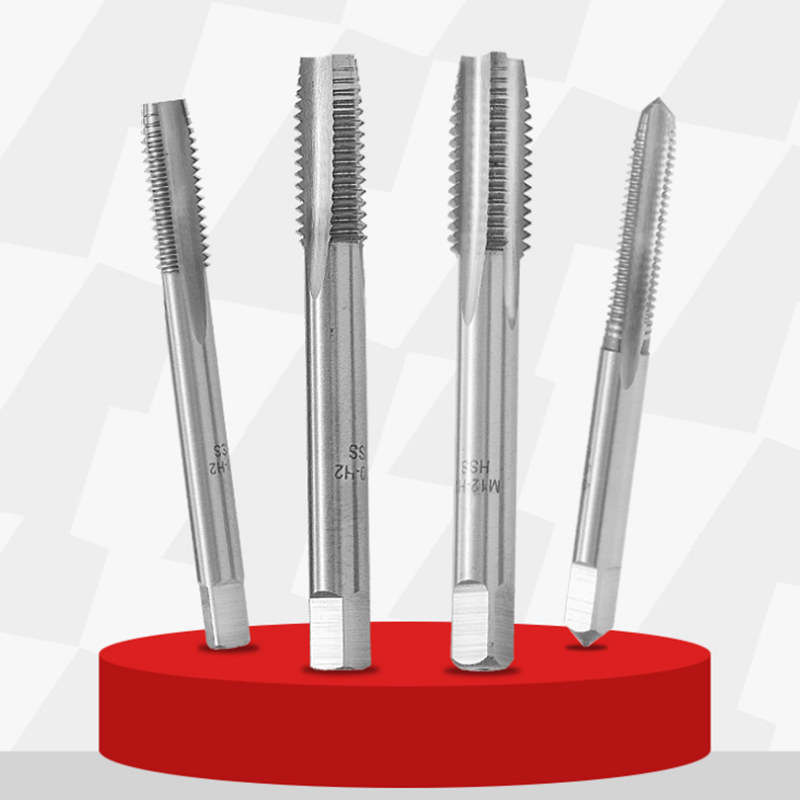
Comprehensive Tooling Portfolio for High Speed Machining
Explore our full spectrum of CNC holders, indexable tools, maintenance units, and specialized accessories




-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China