
Precision Drilling Clamping & Stabilization Systems
Maximizing deep hole boring and heavy drill engagement demands unyielding rigidity from the spindle taper down to the workpiece base. Explore our core workholding and centering solutions calibrated for high-thrust metal drilling environments.
The Imperative of Thermal Clamping in Modern Metal Drilling
Modern heavy industrial manufacturing—spanning aerospace turbine construction, power generation rotor forgings, maritime drive shafts, and structural mining equipment—faces unprecedented challenges in holemaking operations. The transition to hyper-tough workpiece materials, such as heat-resistant superalloys (HRSA), Inconel 718, Titanium Ti-6Al-4V, and high-tensile armor steels like HARDOX, has exposed the fundamental mechanical limitations of legacy tool holding interfaces.
When driving solid carbide or indexable insert drills with aspect ratios exceeding 5×D, 8×D, or even 12×D into tough metallurgical matrices, the cutting forces ($F_z$ feed force and $M_c$ cutting torque) rise exponentially. Traditional mechanical toolholders, notably ER collet chucks and side-lock Weldon flat holders, introduce micro-deflections and asymmetric runout. This imbalance leads to premature chisel edge micro-chipping, harmonic chatter, asymmetric hole taper, and catastrophic tool failure.
Thermal Shrinkage: 360° Symmetrical Grip
Induction shrink fit tool holding leverages thermal expansion dynamics to generate seamless, uniform hoop stress around the entire circumference of the cutting tool shank. When cooled, the bore contracts, producing up to 1,200 Nm of continuous radial grip force without mechanical collet gaps, setscrews, or wedge nuts.
Result: True concentric clamping, rotational runout under 0.003mm (3 microns), and harmonic dampening unachievable with mechanical locking systems.
Sub-3-Micron Runout ($T.I.R.$)
Excessive Total Indicated Runout in heavy drilling accelerates non-uniform flute wear. By holding concentricity within 0.003mm at 3×D overhang, shrink fit holders ensure both cutting lips engage the material at identical shear angles, extending drill life by 200% to 300%.
Harmonic Vibration Attenuation
The solid monolithic geometry of heat-shrink holders eliminates loose internal parts, sliding tapers, and threaded nuts. This homogeneous steel structure absorbs resonant peak vibrations, suppressing micro-chatter during aggressive feed entries in deep cavities.
Ultra-High Torque Transmission
Unlike hydraulic chucks susceptible to high-temperature oil thinning, shrink fit systems maintain uninterrupted, friction-welded grip levels across thermal cycles. This prevents tool slippage or pull-out under heavy chip-load drilling surges.
Comparative Analysis: Shrink Fit vs. Conventional Clamping in Heavy Drilling
In heavy-duty metal drilling, selecting the proper tooling interface directly dictates part accuracy, cycle times, spindle bearing longevity, and recurring carbide expenditure. Below is a detailed engineering comparison of shrink fit holders against legacy toolholding architectures under high-thrust metal drilling stresses.
| Performance Metric | Induction Shrink Fit Chuck | Side-Lock Weldon Flat | Precision ER Collet Chuck | Hydraulic Expansion Chuck |
|---|---|---|---|---|
| Total Runout ($T.I.R.$ at 3D) | < 0.003 mm (High Precision) | 0.012 – 0.025 mm | 0.008 – 0.015 mm | < 0.004 mm |
| Clamping Torque Capacity | Extreme (up to 1200+ Nm) | High (Mechanical Positive Stop) | Moderate to Low (Risk of Slip) | High (Degrades with Heat) |
| Dynamic Balance ($G2.5$) | Up to 25,000 – 40,000 RPM | Poor (< 6,000 RPM) | Moderate (< 12,000 RPM) | Good (< 15,000 RPM) |
| Nose Clearance & Profile | Slim 3° / 4.5° Deep Access | Bulky Set-Screw Body | Bulky Clamping Nut | Relatively Thick Body |
| High-Pressure Coolant Capability | Hermetic Seal up to 100 Bar | Leakage through Set-Screw | Requires Costly Sealed Collets | Hermetic Seal (Temp Limits) |
| Radial Rigidity & Deflection | Highest (Integral Steel Shell) | Asymmetrical / Off-Center | Subject to Micro-Gaps | Medium (Fluid Damping) |
Thermal Fatigue & Advanced Hot-Working Steels
A primary technical consideration in heavy duty drilling with shrink fit systems is holder longevity through repetitive thermal cycles. Premium shrink fit holders are forged from specialized hot-working tool steels (such as modified AISI H13 or proprietary nickel-chromium-molybdenum alloy matrices) treated with anti-oxidation nitro-carburizing coatings.
These metallurgical formulations prevent tempering softening during rapid high-frequency induction heating (300°C–340°C), retaining full clamping modulus through more than 5,000 expansion-shrinkage cycles without tensile decay or bore warping.
High-Pressure Through-Spindle Coolant Dynamics
In deep-hole metal drilling (drilling through 200mm forged blocks or structural flanges), chip evacuation failure is the number one cause of sudden catastrophic tool breakage. The seamless shrink fit seal acts as a hermetic pressure boundary, channeling coolant directly through internal carbide drill passages at pressures exceeding 70 to 100 bar.
This high-velocity hydraulic stream instantly blasts chip curls out of the hole flutes, preventing re-cutting, galling, work-hardening, and localized thermal thermal fractures on carbide margins.
Tianjin MeiWha Precision Machinery Co., Ltd.
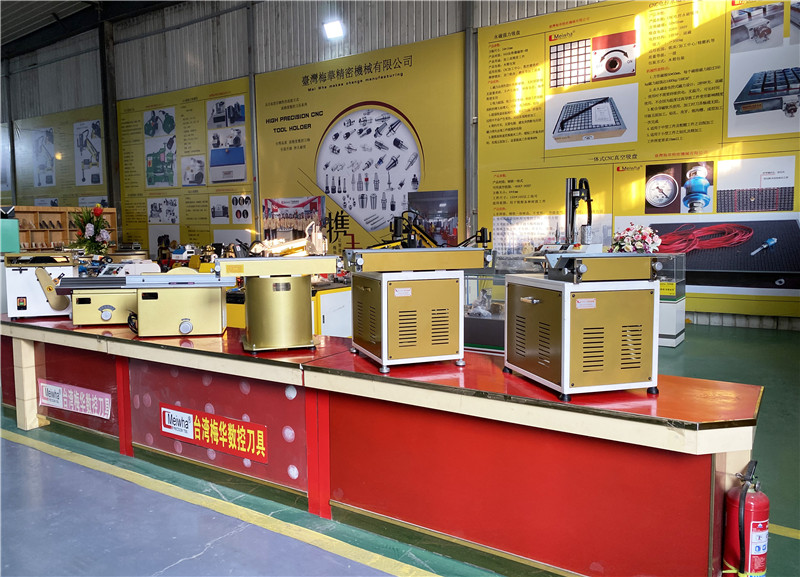
Tianjin MeiWha Precision Machinery Co.,Ltd was founded in June 2005. It is a professional manufactory which engaged in all kinds of NC cutting tools, include Milling tools, Cutting Tools, Turning Tools, Tool holder, End Mills, Taps, Drills, Tapping Machine, End Mill Grinder machine, Measuring tools, Machine tool accessories and other products.
Our Location: Our company is located in Jingzhong Industrial park, Dongli District, Tianjin, covering an area of more than 5000 square meters, with 1500 square meters of modern office space. Branches, direct stores, subordinate branch agents or special distributors are arranged in various regions to form outlet distribution services. At the same time, Meiwha products export include Dubai, The United Arab Emirates, Switzerland, France, South Africa, India, The Philippines, Thailand and so on.
Modern Production Facilities & Strict Quality Control
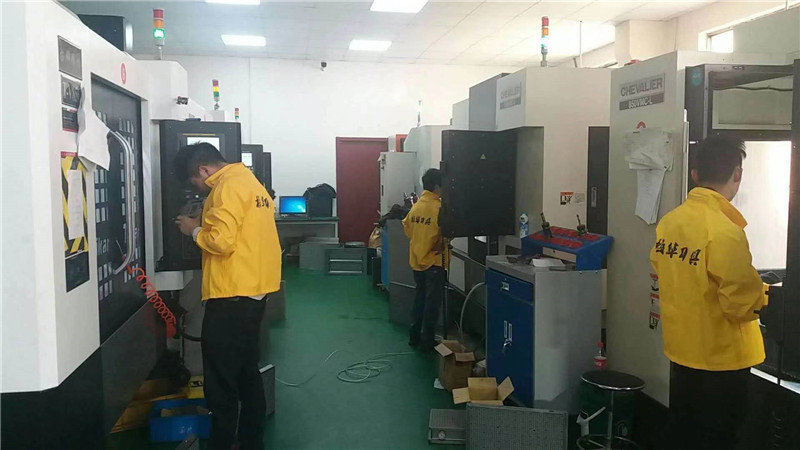
Our standard tools meet the highest quality standards, which we have been able to prove a million times to satisfied customers since 2005. With our mature product portfolio we offer solutions for the tasks around drilling, milling, countersinking and reaming. With high commitment and ambition we continue to develop and optimize our solid carbide line. The excellent technical properties as well as the availability which can be viewed online offer our customers and partners the best conditions for optimizing their processes.
Extreme Drilling Scenarios & Industry 4.0 Integration
As modern heavy industries adopt lean manufacturing principles, the intersection of thermal tooling holding and automated precision drilling opens unprecedented manufacturing capabilities. Discover how high-torque shrink fit toolholders redefine cycle productivity across rigorous metal cutting verticals.
1. Energy & Wind Power Flanges
Drilling hundreds of M36 and M42 bolt holes in forged 42CrMo4 wind turbine yaw rings requires uninterrupted 24/7 machining. Shrink fit holders eliminate drill walk and spindle vibration, preventing out-of-round hole ovality and safeguarding multimillion-dollar turbine forgings.
2. Aerospace Landing Gear & Engine Pylons
Deep-hole drilling in Ti-5553 and Inconel 718 produces intense cutting shear temperatures exceeding 900°C. Shrink fit holders ensure flawless concentricity, reducing radial force spikes on drill margins that typically trigger work-hardening and sub-surface micro-cracking.
3. Heavy Structural & Defense Fabrication
High-feed indexable drilling through thick ballistic armor steel plates requires massive axial thrust. Shrink fit toolholders withstand peak feed forces up to 25 kN without micro-slipping, ensuring consistent depth repeatability and hole perpendicularity.
Future Trends: AI-Enabled Tool Clamping & Thermal Diagnostics
The industrial toolholding landscape is rapidly evolving with Industry 4.0. Next-generation shrink fit systems are adopting automated RFID and QR-embedded data chips that interface directly with intelligent induction heaters. These smart heating units autonomously recognize the specific toolholder geometry, carbide grade, and shank diameter, delivering the exact frequency and induction coil duration needed down to the millisecond. This prevents accidental overheating, optimizes cycle times, and tracks the exact thermal cycle history of each toolholder to predict structural fatigue long before runout degradation occurs.
Our Advantages & Honors
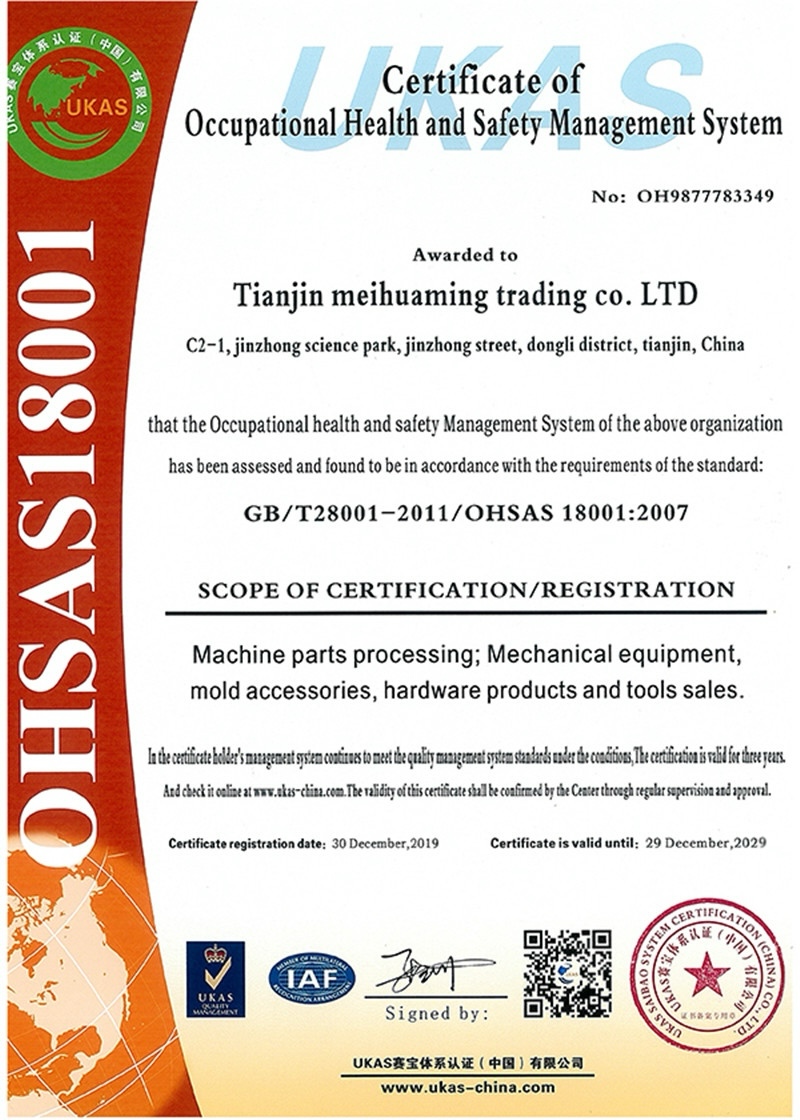
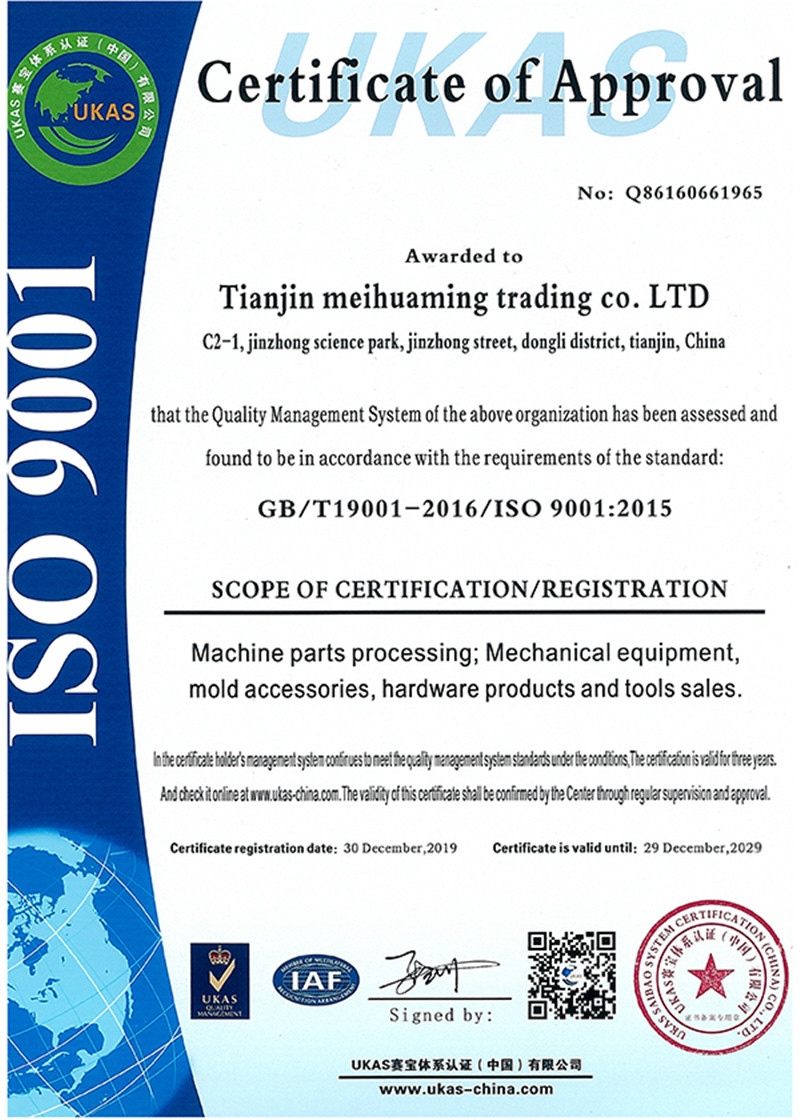
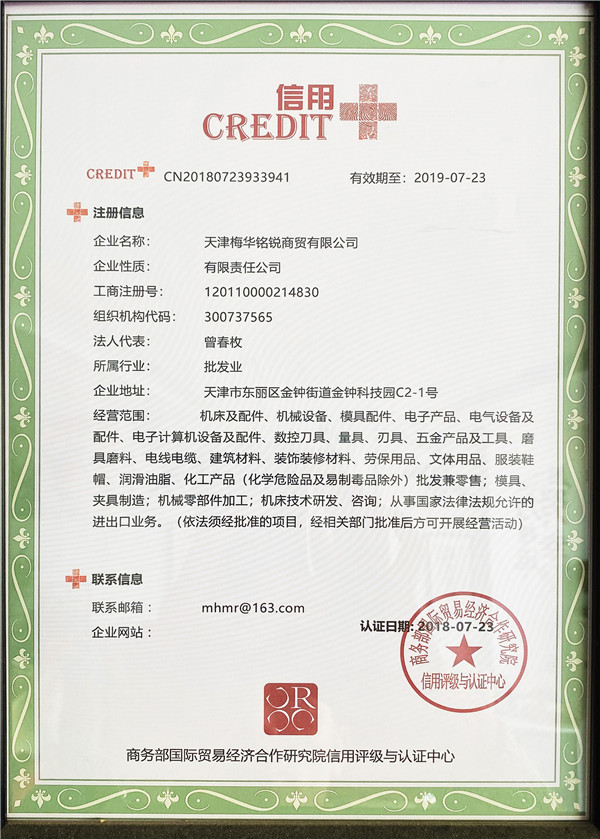
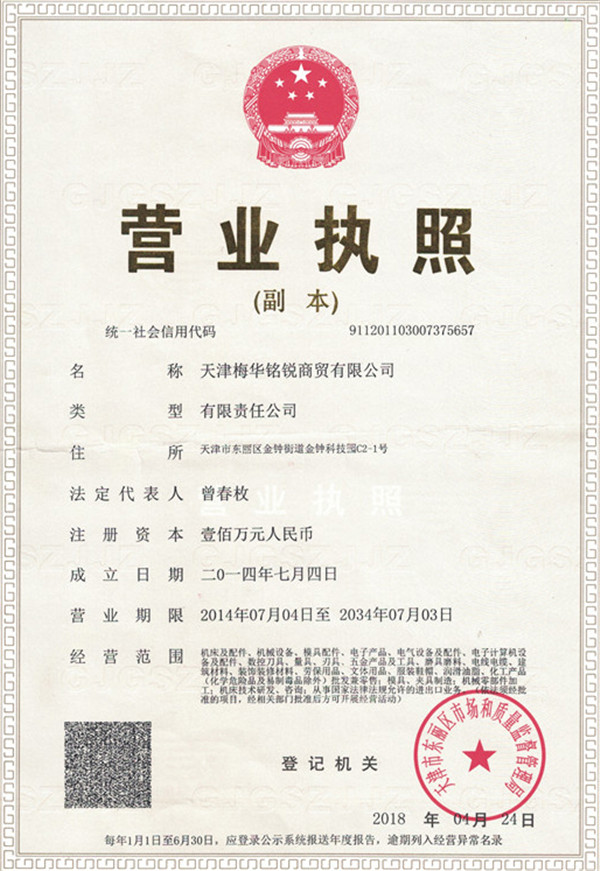
The company combines industry advantages, integrates product resources, and inherits all customer-oriented business concepts, only provides customers with the right products, and provides customers with one-stop procurement services. At the same time, with excellent product quality, precise delivery time, reasonable and competitive prices, it has won the approval of the industry and the support of our customers. It has established long-term strategic cooperation with many domestic and foreign research institutes and enterprises, such as Tianjin Jinhang Institute of Physics and Beijing Fangshan Bridge 14th Bureau. The company will further rely on its own advantages and strong strength, exert a better brand effect, adhere to the quality policy of "providing customers with satisfactory products with continuous improvement in management and technology", and strive to provide better products and services to new and old customers at local market and abroad.
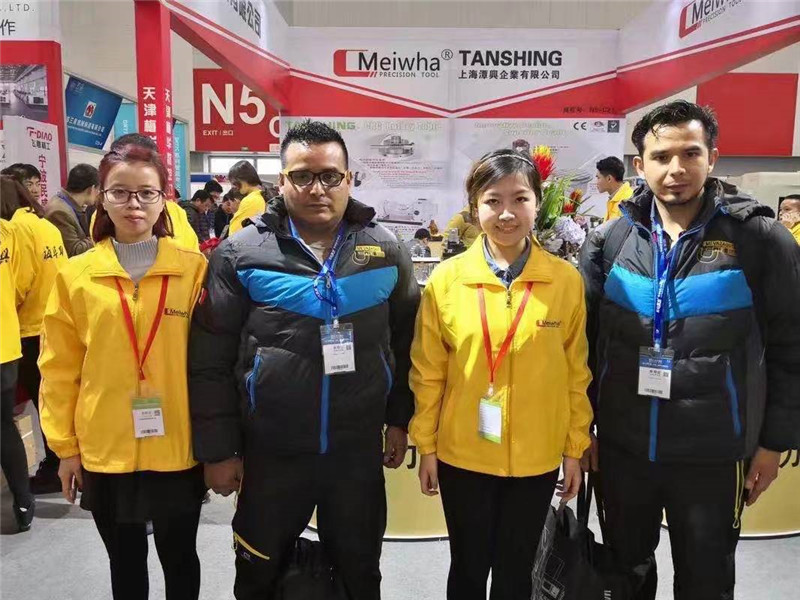
International Exhibitions & Industry Footprint
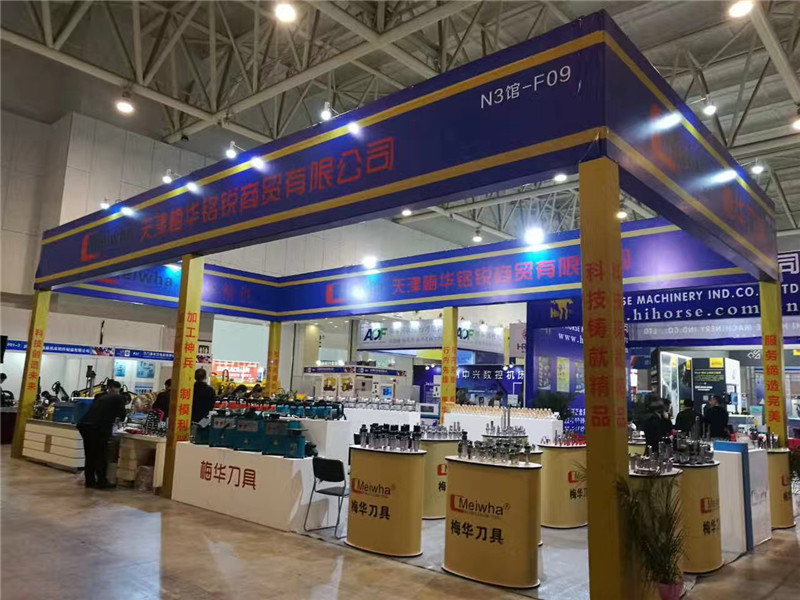
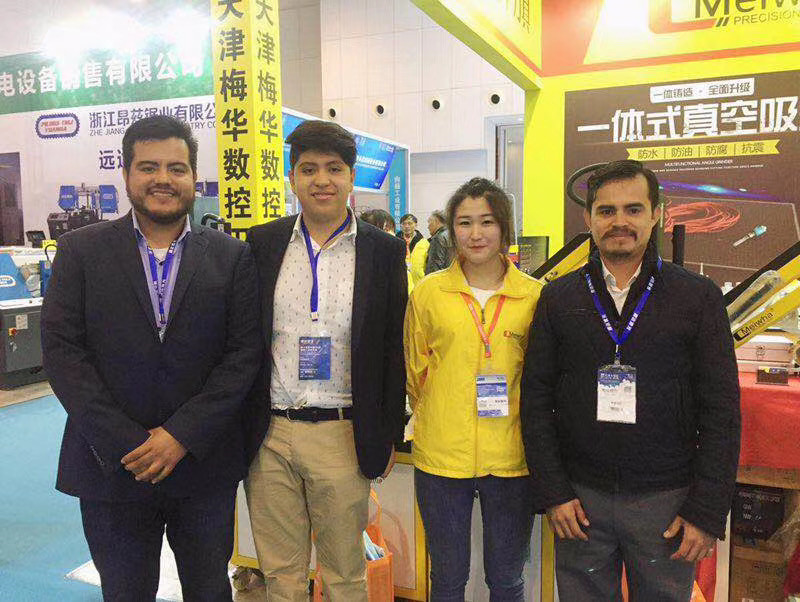
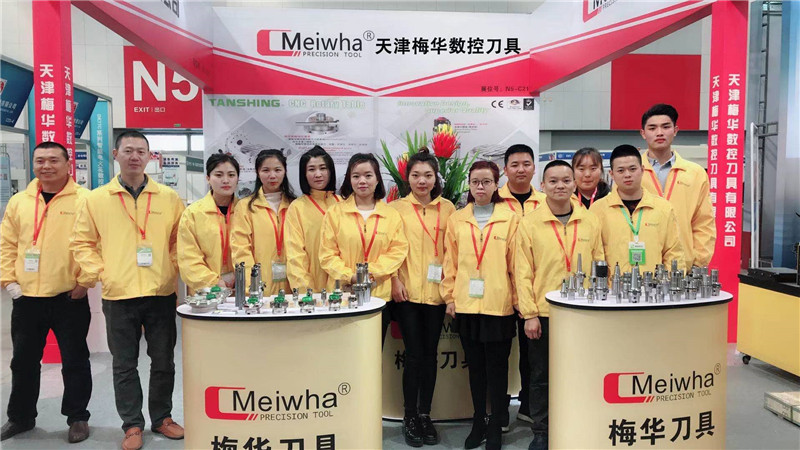
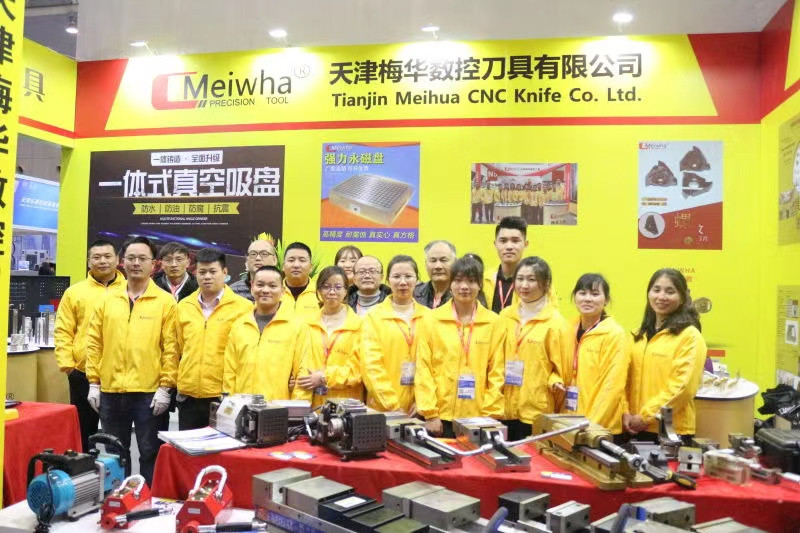
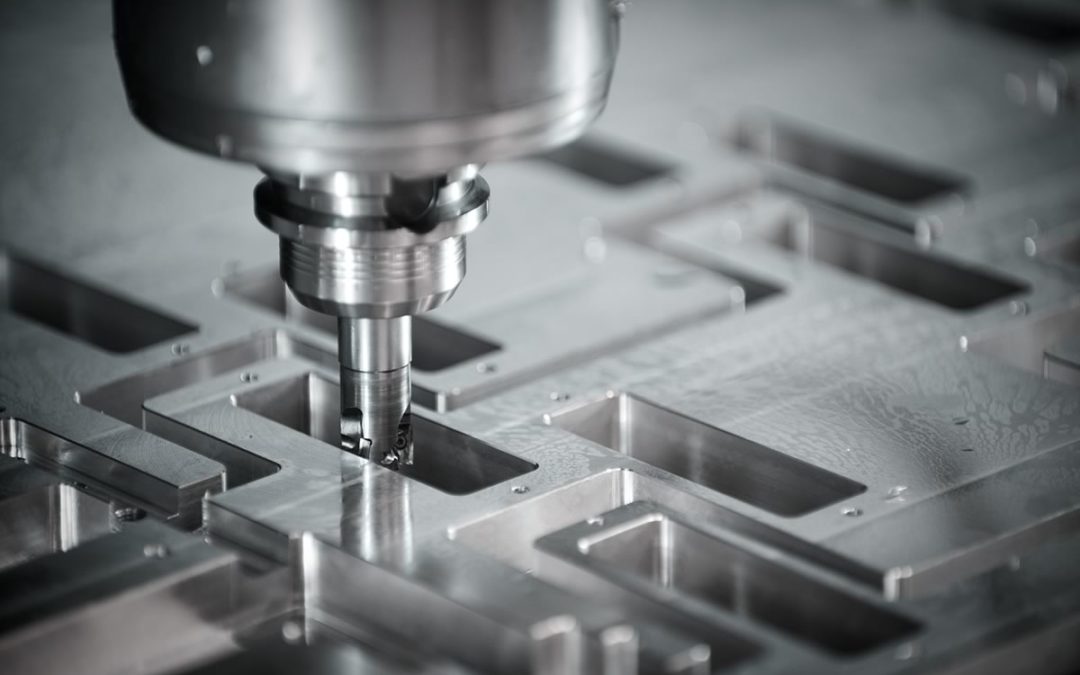
Tianjin MeiWha Precision Machinery showcases innovative CNC machining solutions and precision toolholder engineering at prominent industrial expos across Europe, the Middle East, Southeast Asia, and worldwide.
Associated High-Precision Tooling Categories:
 HSK(A)-GC High-Speed Powerful Holder
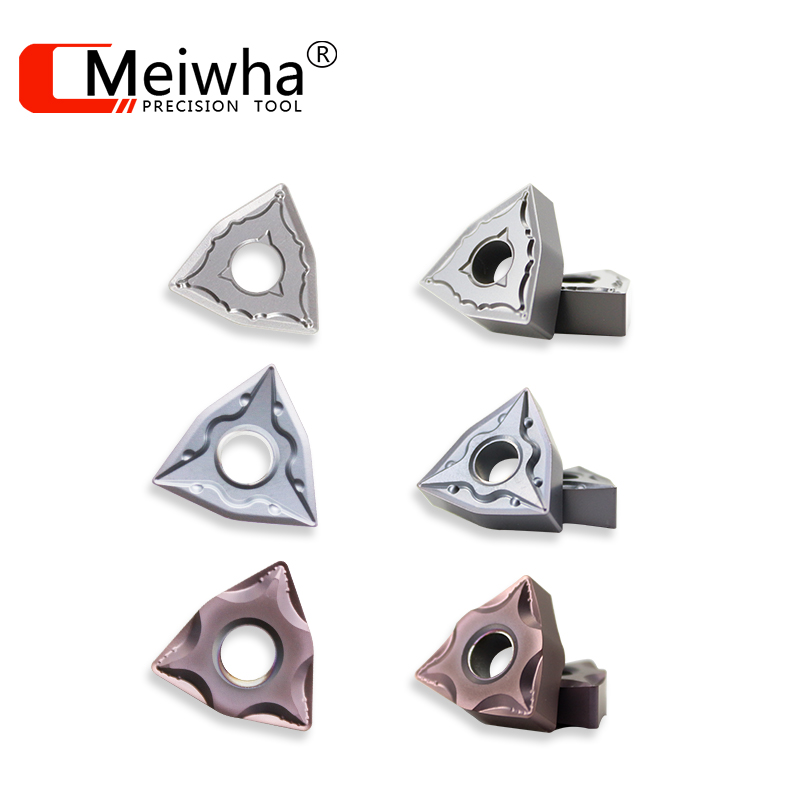 Cutting Tools For Aluminium & Copper
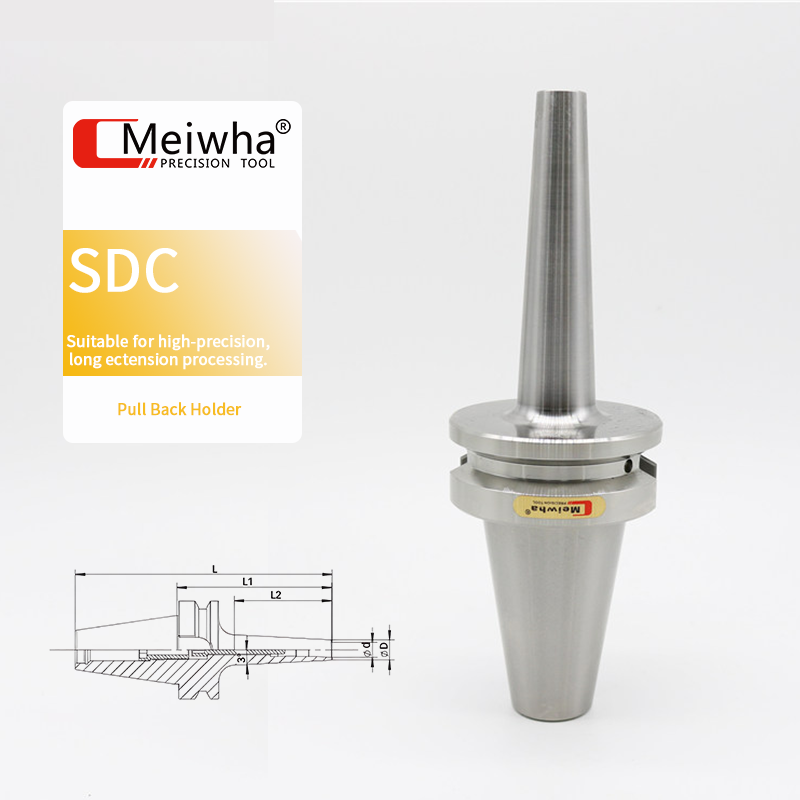 BT-SDC Back Pull Handle
Featured CNC Tool Holders & Machine Accessories
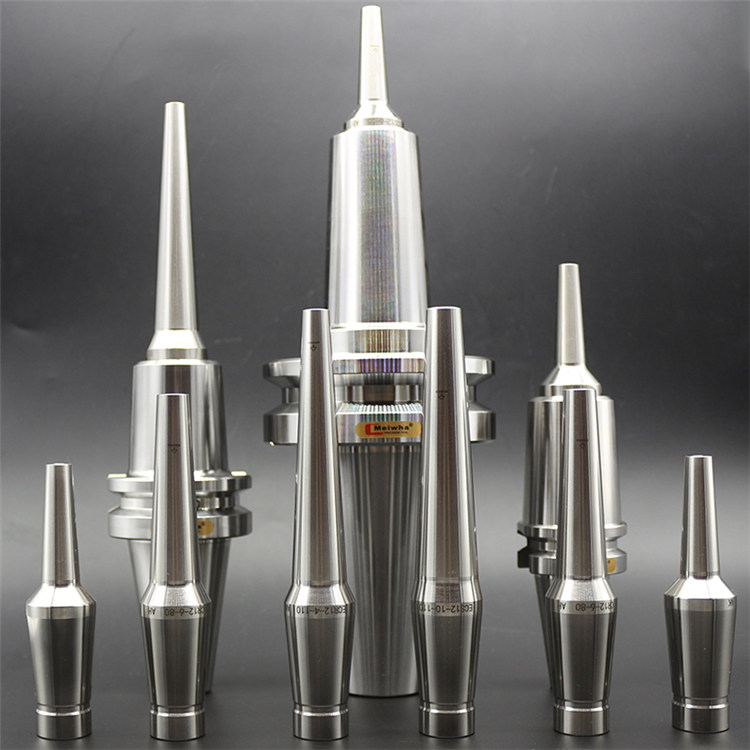
Discover our comprehensive collection of advanced thermal shrink extensions, through-spindle cooling holders, universal angle heads, and extreme-torque chucks engineered for metal drilling and heavy-duty milling applications.




-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China