
Featured CNC Drill & Tap Solutions
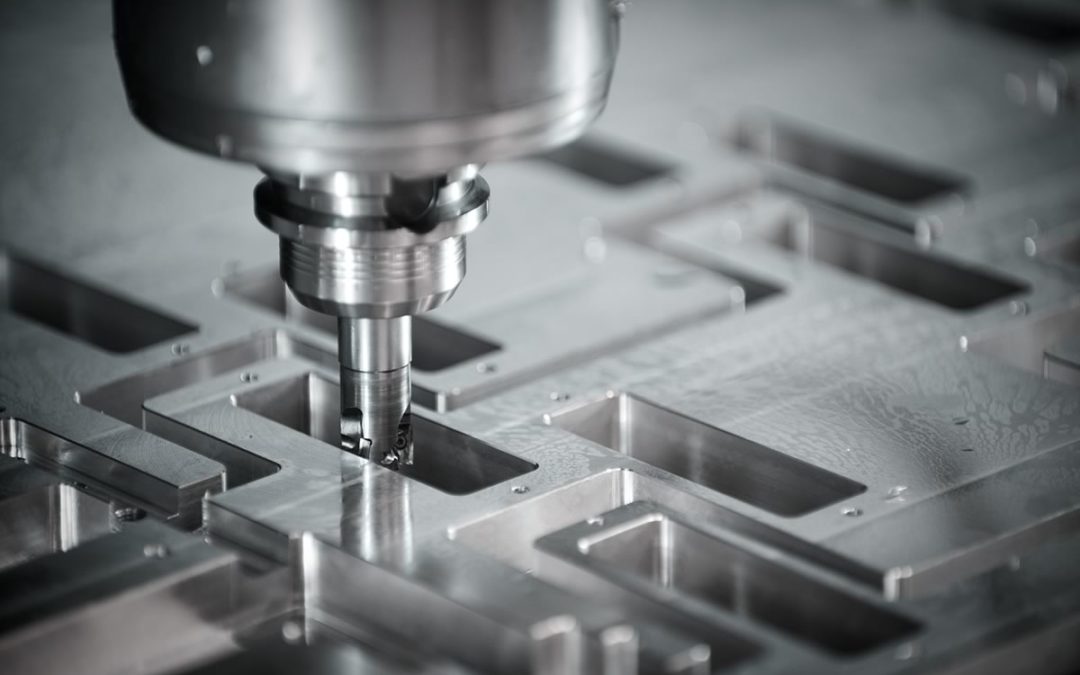
Engineered for uncompromising concentricity, exceptional torque transfer, and long-term dimensional repeatability in demanding production environments.
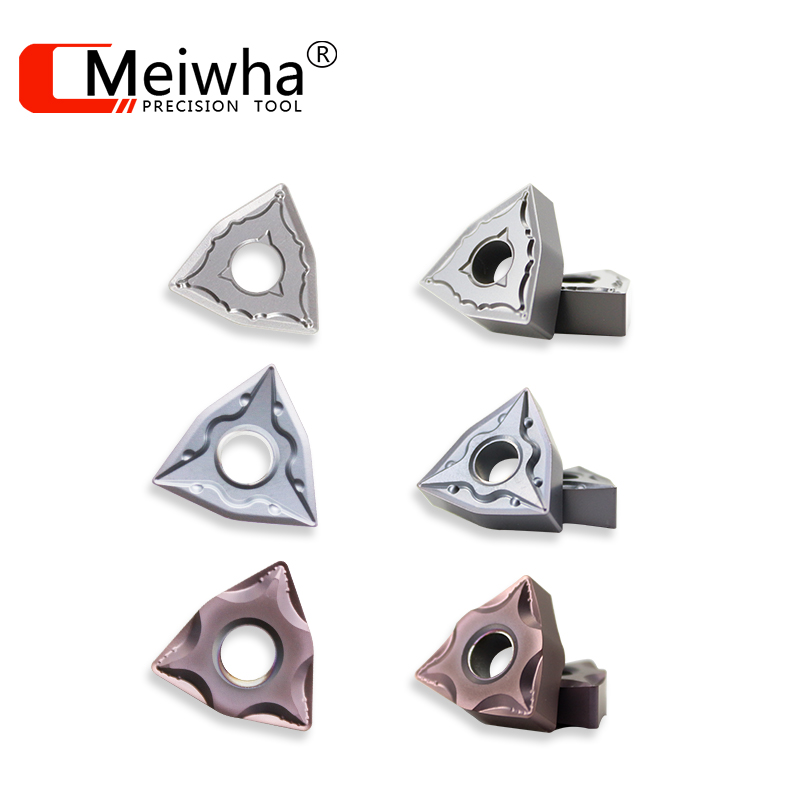
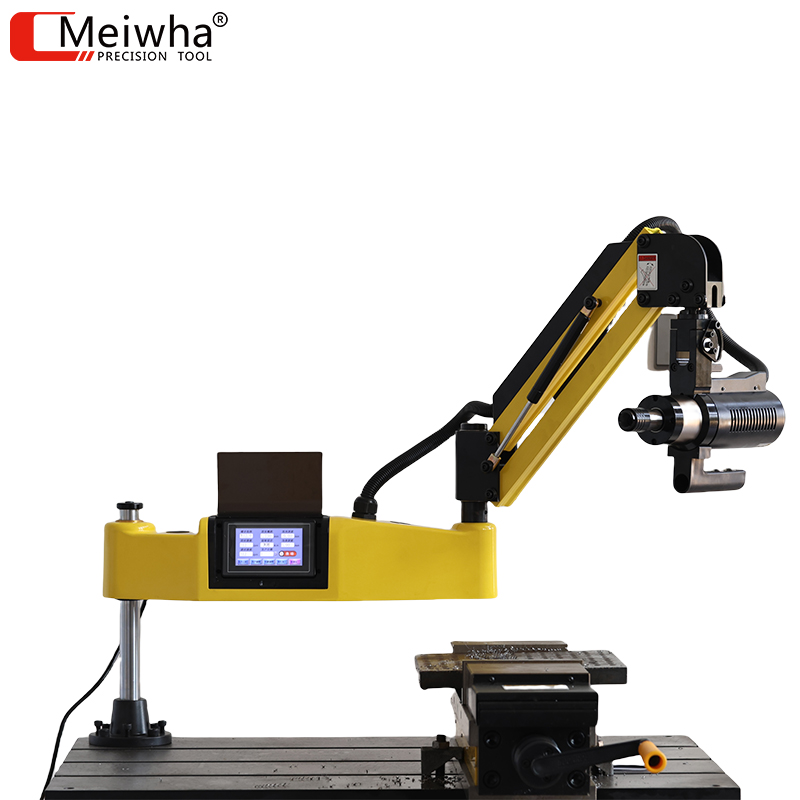
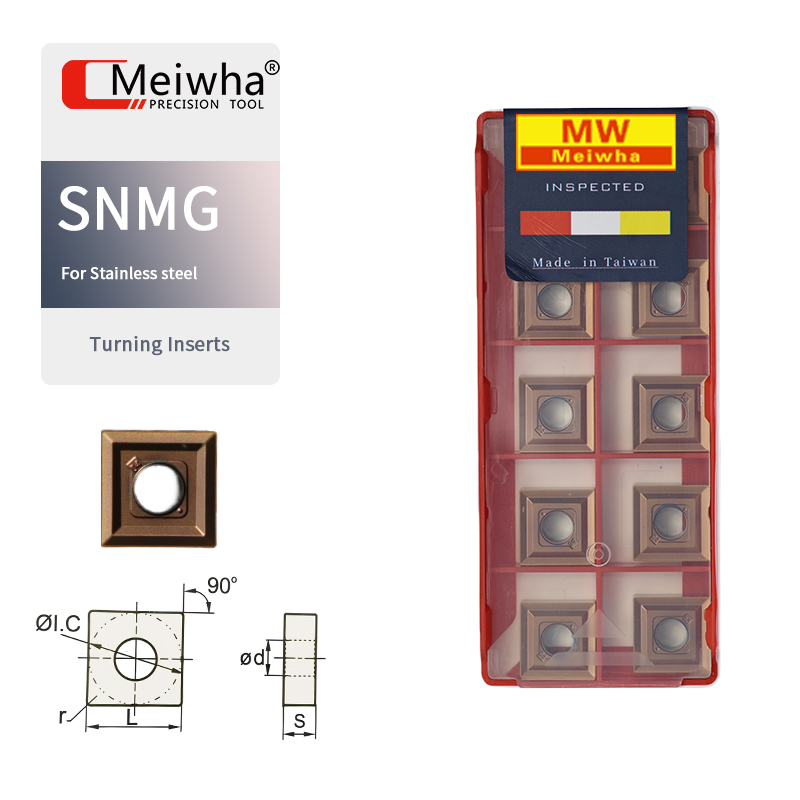
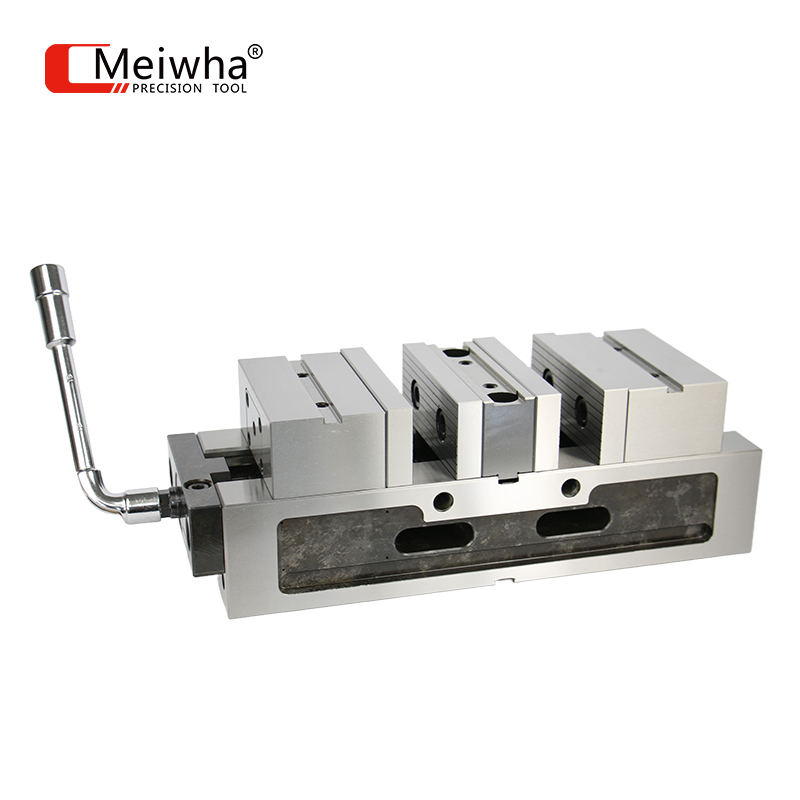
Industrial Status & Evolutionary Dynamics of Shrink Fit Toolholding in CNC Holemaking
In modern precision manufacturing, computerized numerical control (CNC) drilling and tapping operations represent a critical baseline for structural integrity, thread quality, and component reliability. The ongoing global transition toward high-strength alloys—such as titanium Ti-6Al-4V, nickel-based Inconel 718, precipitation-hardened stainless steels, and hypereutectic cast aluminum alloys—has driven conventional tool clamping systems beyond their mechanical thresholds. In high-speed drilling and synchronized rigid tapping cycles, radial deflection, microscopic fretting, centrifugal runout expansion, and torsional slippage directly precipitate premature tool fractures, torn threads, out-of-round bores, and disastrous part scrappage.
To overcome these systemic bottlenecks, **High Clamping Force Shrink Fit Toolholders** have transitioned from specialized mold and die milling into mainstream CNC drilling and tapping operations. By leveraging thermal induction physics, high clamping shrink fit toolholders deliver complete 360-degree cylindrical contact around solid carbide or high-speed steel tool shanks. The absence of mechanical collets, pressure rings, or driving balls eliminates intermediate mechanical tolerances, establishing exceptional structural rigidity. Current industrial data confirms that integrating high-rigidity shrink fit tooling reduces runout from standard collet values (≥ 0.010 mm) to less than 0.003 mm (3 microns) at 3x shank diameter overhang. This enables CNC machine centers to push cutting speeds and feed rates upwards by 35% to 50% without compromising thread profile accuracy or borehole roundness.
360° Cylindrical Gripping
Complete radial thermal compression eliminates concentricity gaps, evenly distributing stress along the tool shank and preventing tool pull-out or radial micro-slippage during peak cutting loads.
Harmonic Resonance Damping
The monolithic, symmetrical geometry of the shrink fit body minimizes chatter and dampens torsional vibration harmonics that typically ruin fine thread finishes during high-RPM reversals.
Streamlined Clearance Contour
Slim 3-degree and 4.5-degree external tapers offer deep cavity penetration, facilitating coolant access directly to the drill tip and tap flutes in complex structural engine casings.
Physics of Shrink Fit: Thermal Induction Mechanics & Clamping Dynamics
The operational principle of high clamping force shrink fit toolholding relies on controlled thermal expansion and subsequent contraction of premium tool steel alloys. The internal bore of the toolholder is precision-ground slightly smaller than the nominal cutting tool shank diameter (a controlled interference fit, typically engineered between 0.005 mm and 0.018 mm depending on the bore diameter). During tool change cycles, an induction heating coil applies high-frequency magnetic eddy currents to the holder’s outer nose section for 3 to 7 seconds. The steel nose expands uniformly, allowing the tool shank to enter seamlessly. As the holder is cooled down via pneumatic chilled air or liquid cooling adapters, the sleeve shrinks symmetrically around the tool shank.
The resultant interference pressure generates radial clamping forces exceeding 10,000 N and holding torque transmission ratings upwards of 350 Nm to 900 Nm for standard metric shank diameters (ø6 mm to ø25 mm). In drilling operations where axial thrust forces exceed several thousand Newtons and in tapping cycles where rapid spindle acceleration/deceleration induces dramatic angular momentum spikes, shrink fit toolholders maintain immutable axial position and zero backlash.
| Clamping System Type | Runout TIR (at 3D) | Clamping Torque Rating | High-Speed Balance (G2.5) | Interference Profile Clearance | Tool Life Impact |
|---|---|---|---|---|---|
| High Clamping Shrink Fit | ≤ 0.003 mm | Very High (> 380 Nm) | Up to 45,000 RPM | Slim / Exceptional Access | Baseline +200% to +300% |
| Standard ER Collet Chuck | 0.010 mm – 0.015 mm | Moderate (~120 Nm) | Up to 15,000 RPM | Bulky Collet Nut Interferences | Standard Reference (100%) |
| Precision Hydraulic Chuck | ≤ 0.004 mm | High (~240 Nm) | Up to 25,000 RPM | Moderate Outer Diameter | Baseline +150% to +180% |
| Side-Lock Weldon Holder | 0.015 mm – 0.025 mm | High (Mechanical Screw) | ≤ 8,000 RPM (Unbalanced) | Bulky Offset Design | Baseline -30% (Chipping Risk) |
Deep Dive Application Scenarios: Where High Clamping Force Shrink Fit Excels
1. Synchronized High-Speed Rigid Tapping in Automotive Aluminum Powertrain Blocks
In high-volume engine block and transmission case manufacturing, hundreds of blind threaded holes (M4 to M12) must be tapped within tight cycle time margins. Rigid tapping cycles require the CNC spindle to accelerate up to 4,000 RPM, reverse instantaneously at depth, and retract at matching spindle speeds. In mechanical chucks, microscopic rotational lag caused by collet deflection distorts thread flanks, leading to pitch error and thread gauge failures. High clamping force shrink fit toolholders ensure rigid unity between the tap shank and the spindle axis, producing aerospace-grade 6H/4H thread tolerances consistently across millions of parts.
2. Deep-Hole Micro-Drilling in Aerospace Turbine Vanes & Medical Titanium Implants
Drilling cooling channels or surgical bone anchor holes with micro-drills (ø0.5 mm to ø3.0 mm) requires extreme rotational concentricity. Any runout greater than 3 microns causes asymmetrical chip loading, resulting in immediate drill deviation, work hardening of the hole wall, or catastrophic tool rupture inside expensive components. Shrink fit extension rods and ultra-slim shrink holders ensure minimal runout, enabling clean chip evacuation through internal high-pressure coolant ducts and preventing unplanned downtime on multi-axis CNC machines.
3. Heavy Structural Steel & Bridge Truss Drilling
Processing massive structural plates with large-diameter carbide drills demands extreme radial torque and resistance to severe axial pushback forces. Standard mechanical chucks often suffer from tool creep or taper slipping under heavy feeds. Heavy-duty reinforced shrink fit holders provide the immense frictional grip required to penetrate thick alloy plates without tool withdrawal, safeguarding machine operators and tooling inventory.
Commercial Realities, Tool Life Economics & Future Technological Trends
From a plant financial perspective, adopting high clamping shrink fit technology yields substantial returns on investment (ROI). Although initial investments include induction heating machines and precision toolholders, the total cost of ownership (TCO) decreases rapidly. Due to sub-3-micron runout, cutting edges experience uniform wear rather than intermittent shock loading. As a result, solid carbide drills, thread mills, and taps consistently demonstrate 2x to 4x increases in operational lifespan before regrinding. Machine spindle bearings also benefit directly from balanced shrink fit assemblies, reducing expensive spindle rebuild intervals caused by eccentric chatter.
Looking ahead, Industry 4.0 integration is transforming shrink fit technology into an intelligent machining nexus. Emerging trends include RFID/QR data chip integration embedded directly into the toolholder body, logging thermal cycles, remaining tool life, and dynamic balancing parameters. Simultaneously, developments in anti-wear cryogenic coatings, internal multi-port through-spindle cooling channels, and localized metallurgy will further expand the application boundary of shrink fit tooling across global manufacturing sectors.
Tianjin MeiWha Precision Machinery Co., Ltd.
Leading innovator in advanced CNC cutting tools, toolholders, and industrial machining accessories since June 2005.
About Our Company & Global Reach
Tianjin MeiWha Precision Machinery Co., Ltd. was founded in June 2005. It is a professional manufacturer engaged in all kinds of NC cutting tools, including Milling tools, Cutting Tools, Turning Tools, Tool holders, End Mills, Taps, Drills, Tapping Machines, End Mill Grinder machines, Measuring tools, Machine tool accessories, and other precision products.
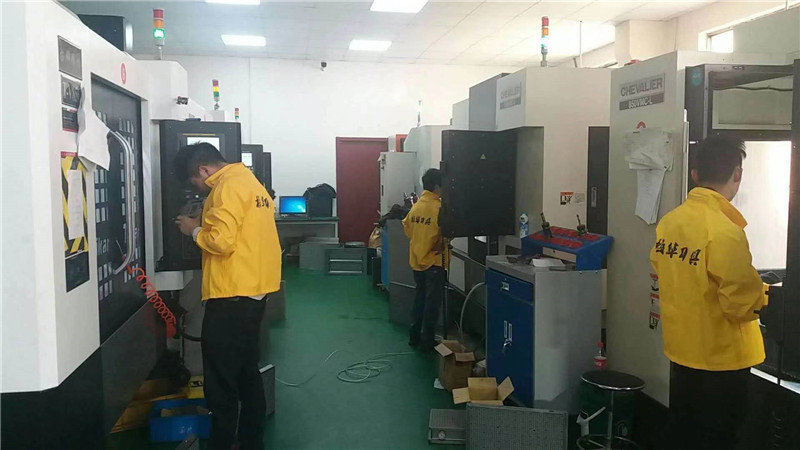
Our company is located in Jingzhong Industrial Park, Dongli District, Tianjin, covering an area of more than 5,000 square meters, with 1,500 square meters of modern office space. Branches, direct stores, subordinate branch agents, and special distributors are arranged across multiple regions to form seamless distribution services.
At the same time, Meiwha products are exported worldwide, including Dubai, The United Arab Emirates, Switzerland, France, South Africa, India, The Philippines, Thailand, and many other industrialized markets.
Our Quality & Manufacturing Excellence
Our standard tools meet the highest quality standards, which we have proven a million times to satisfied customers since 2005. With our mature product portfolio, we offer complete solutions for tasks surrounding drilling, milling, countersinking, and reaming.
With high commitment and ambition, we continue to develop and optimize our solid carbide lines. The excellent technical properties, strict dimensional quality verification, and online inventory transparency offer our customers and partners the best conditions for optimizing their CNC machining operations.
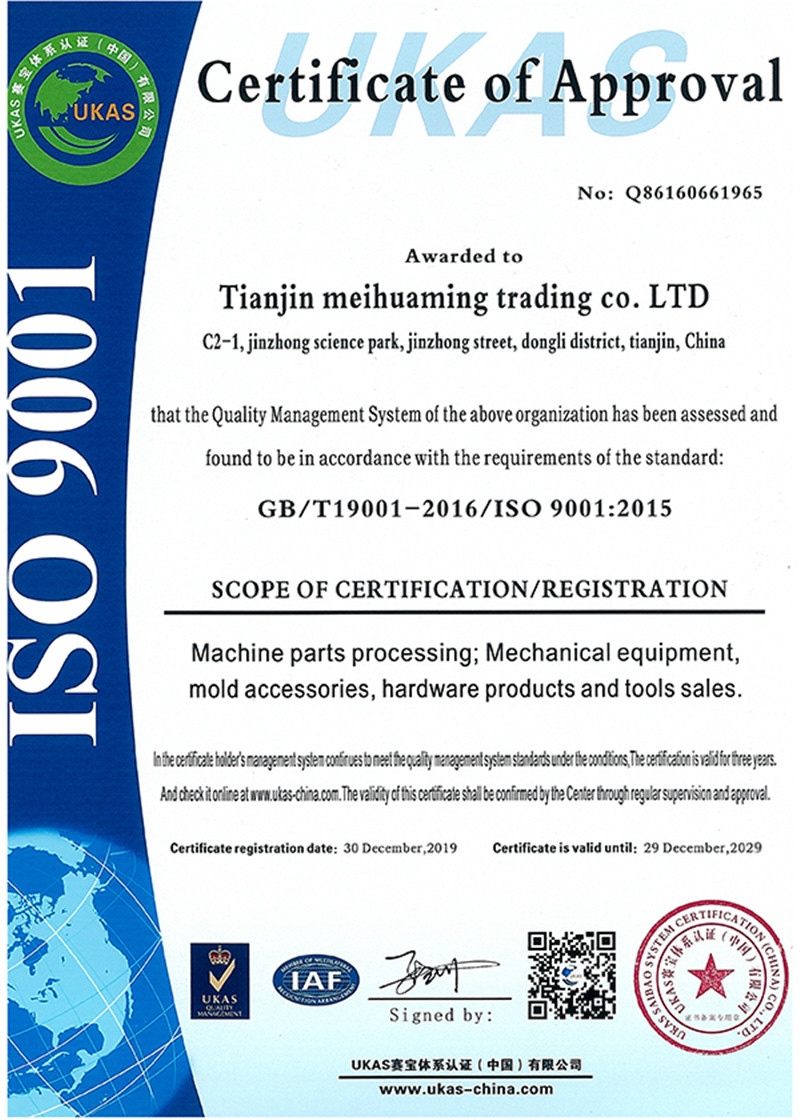
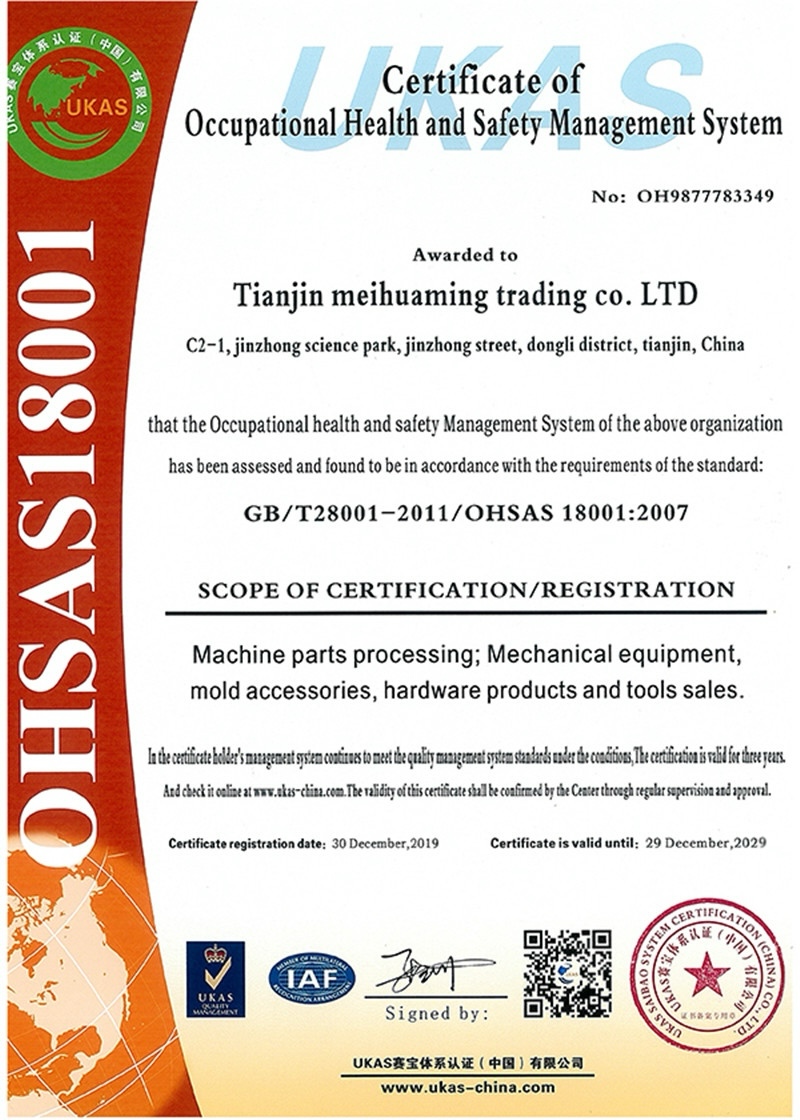
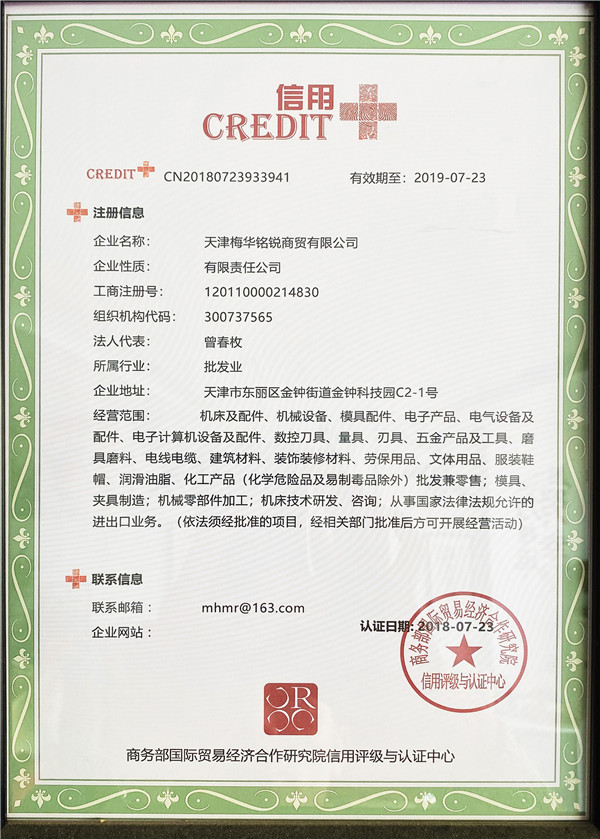
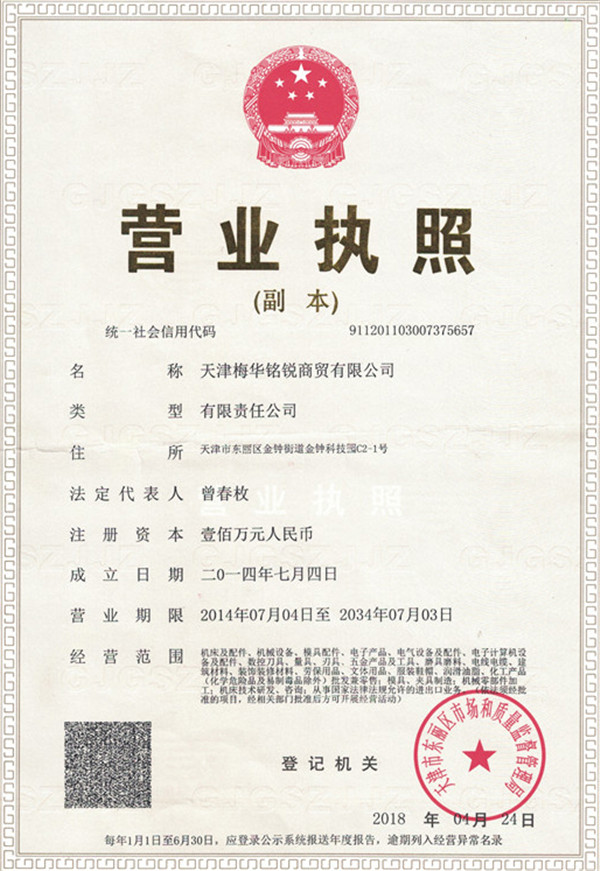
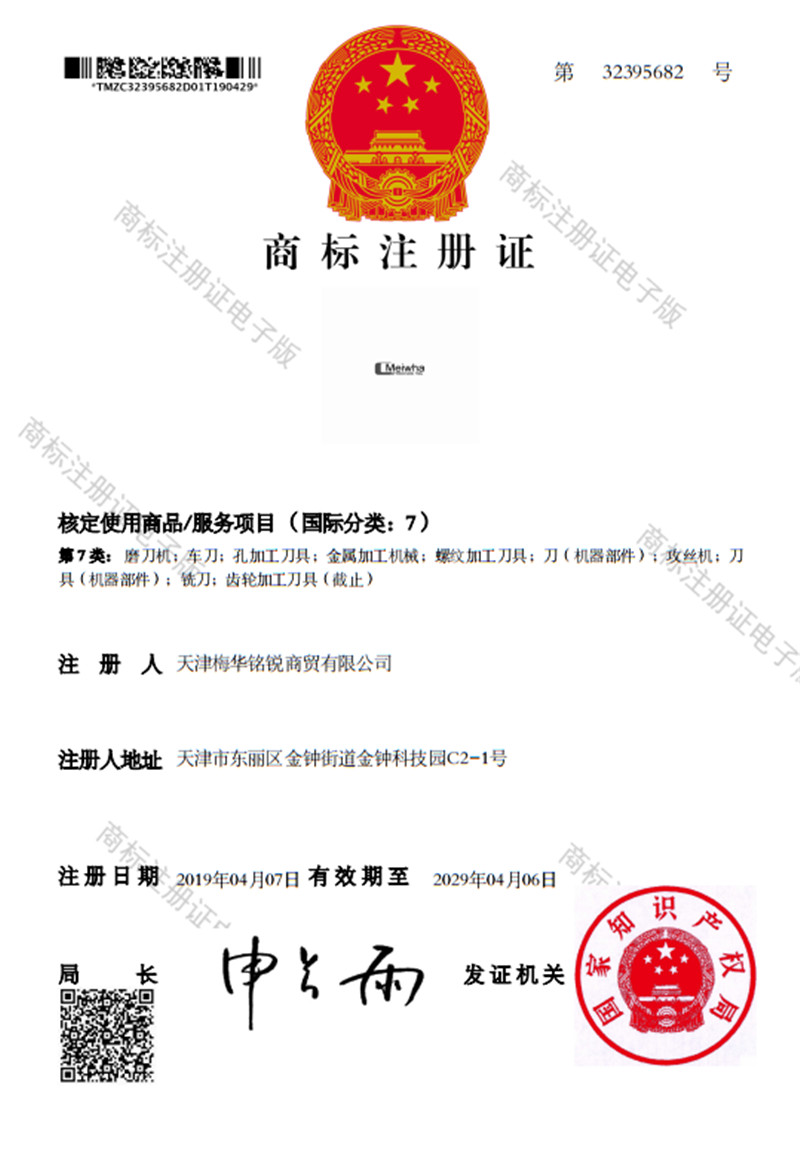
Recognized Certifications & Corporate Honors
Specialized Tooling & Workholding Systems
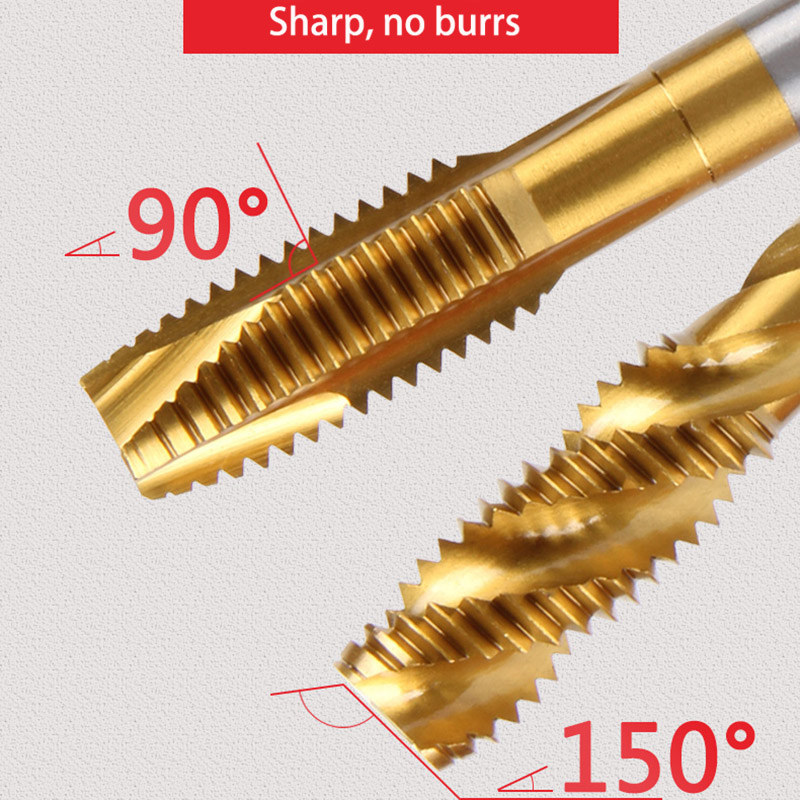
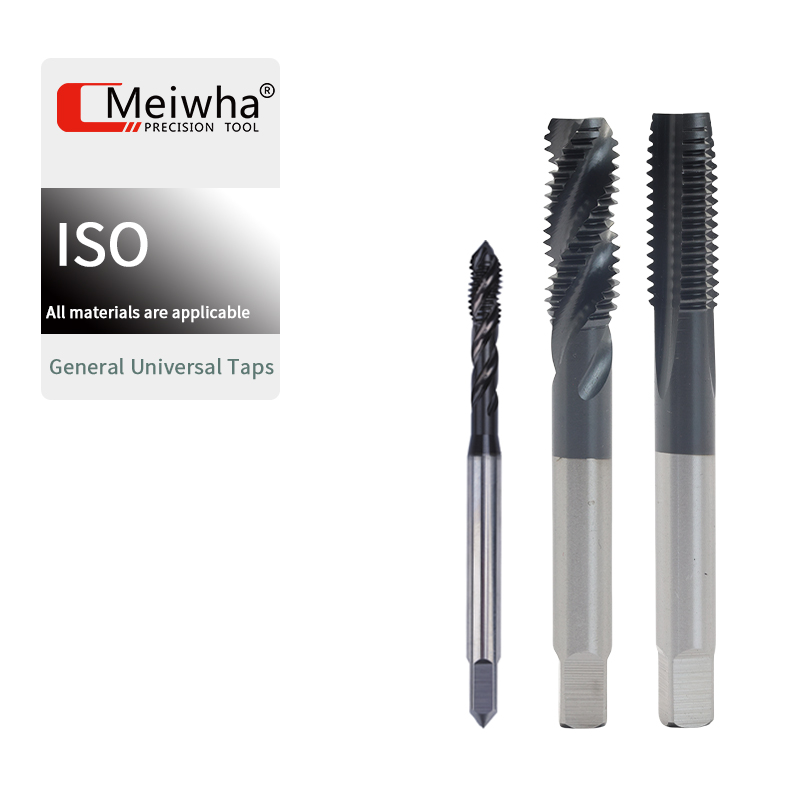
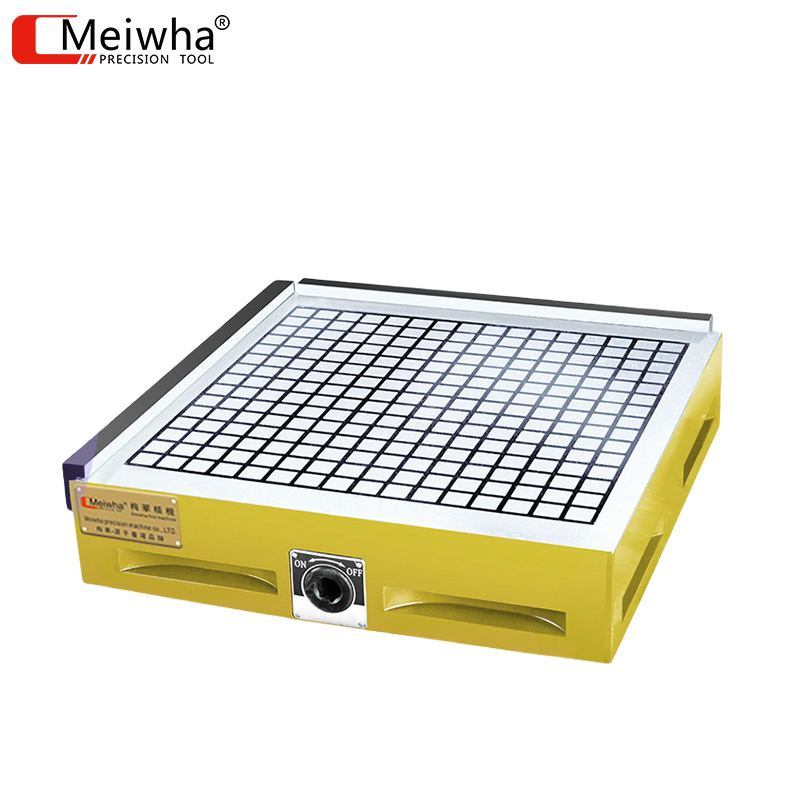
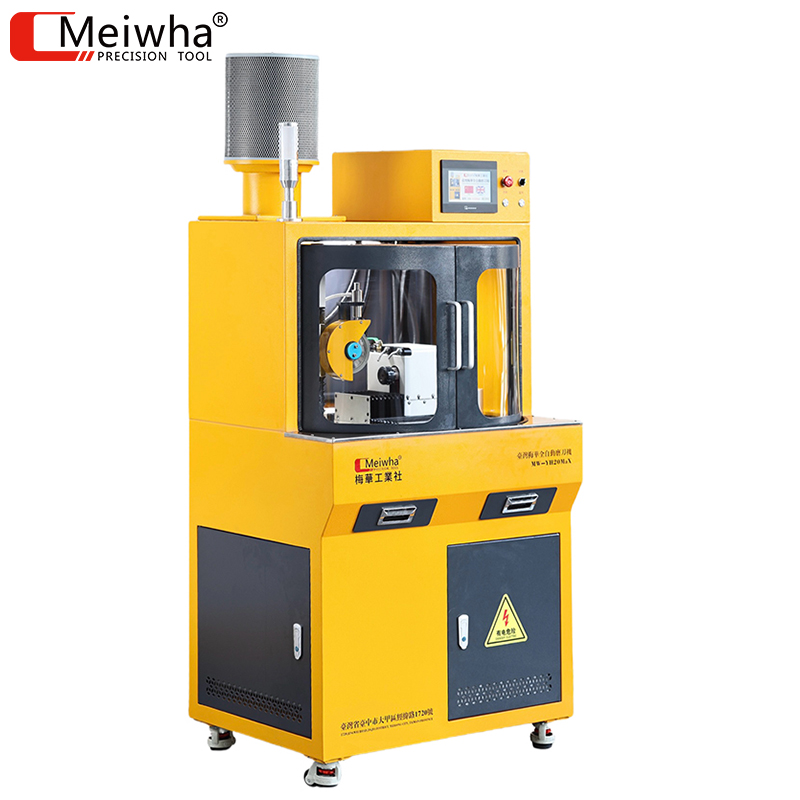
Complementing high-performance shrink fit clamping with premium taps, magnetic workholding chucks, and automatic tool grinding systems.
Our Core Advantages & Strategic Partnerships
The company combines industry advantages, integrates product resources, and adheres to customer-oriented business concepts. We provide customers with the right products and comprehensive one-stop procurement services. At the same time, with excellent product quality, precise delivery times, and reasonable, competitive pricing, MeiWha has won widespread industry approval and continuous customer loyalty.
We have established long-term strategic cooperation with many domestic and foreign research institutes and leading enterprises, such as the Tianjin Jinhang Institute of Physics and Beijing Fangshan Bridge 14th Bureau.
The company continuously relies on its strong technical reserves and manufacturing discipline, adhering to our core quality policy: "Providing customers with satisfactory products through continuous improvement in management and technology."
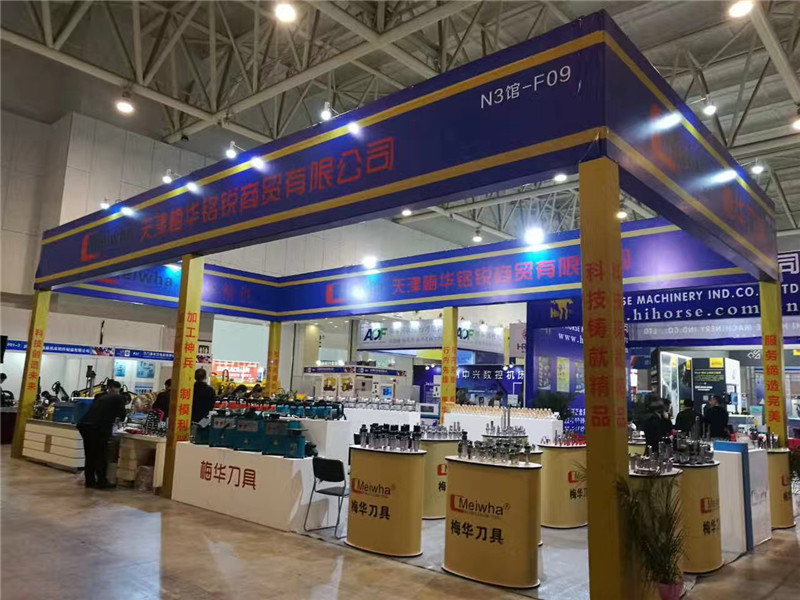
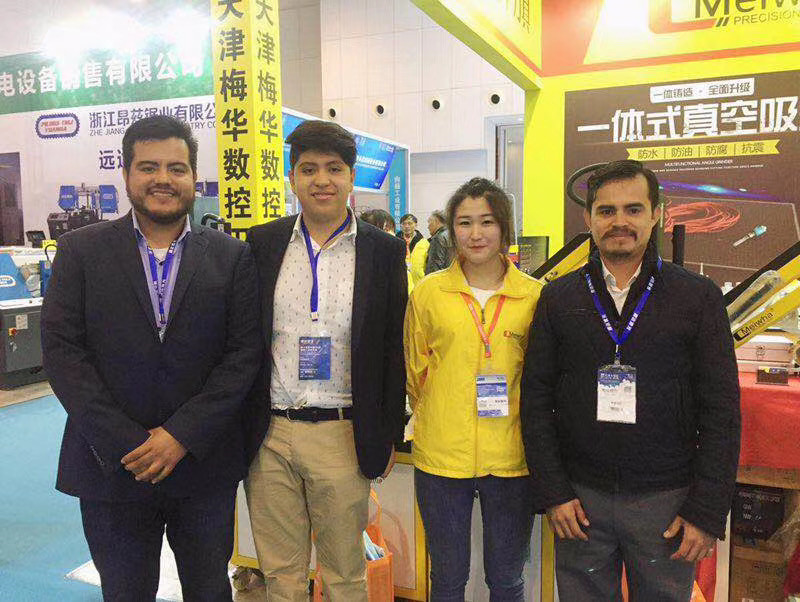
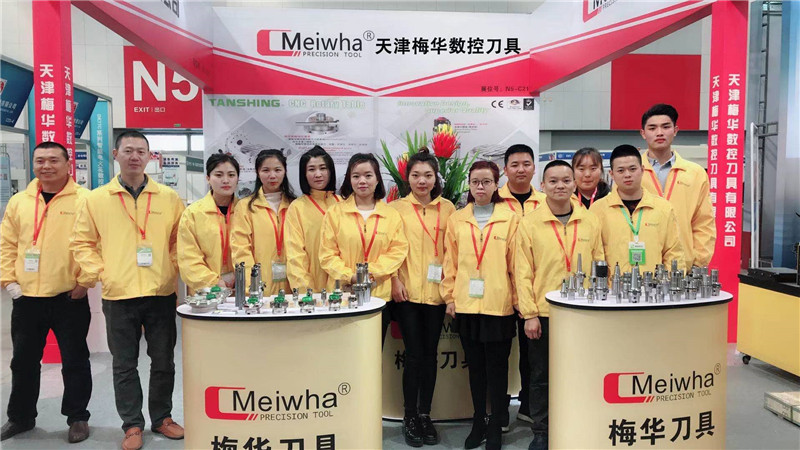
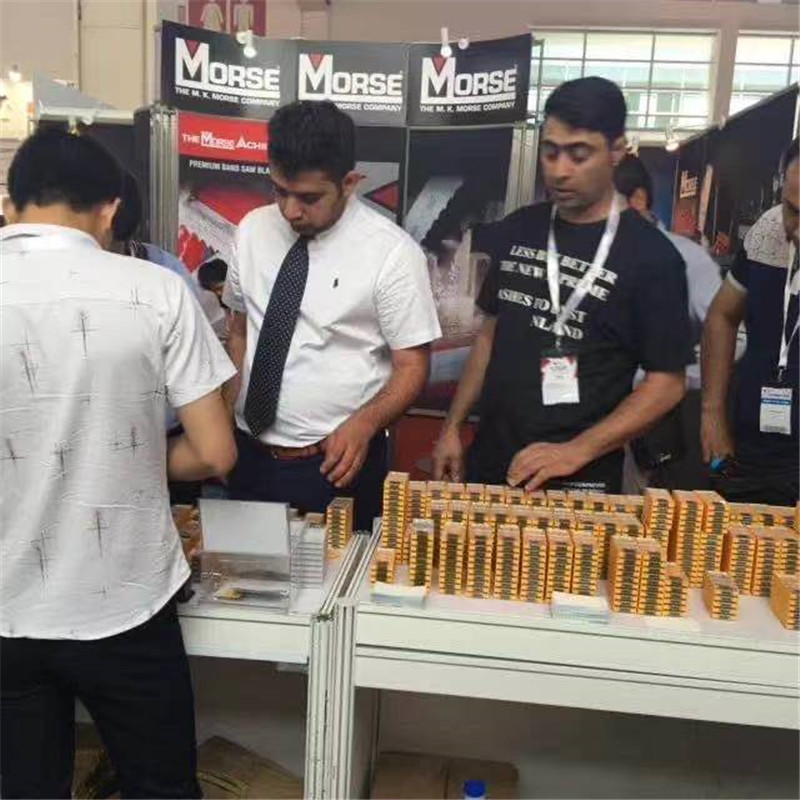
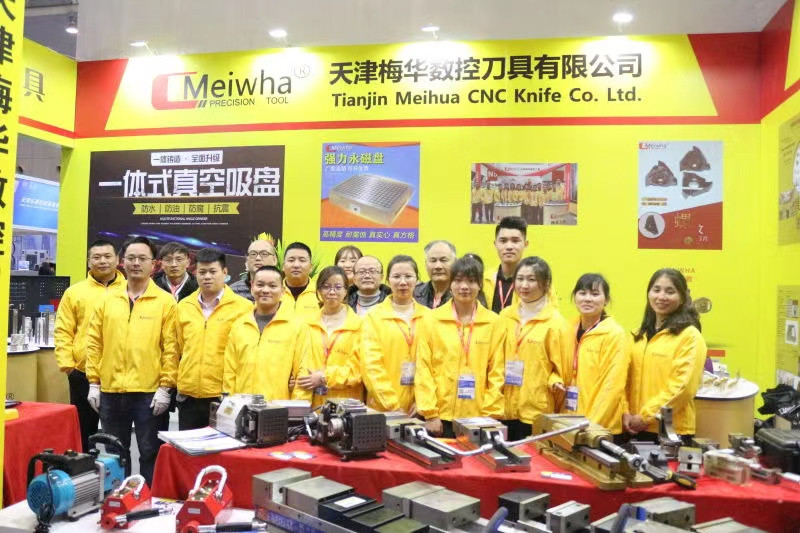
International Industry Exhibitions
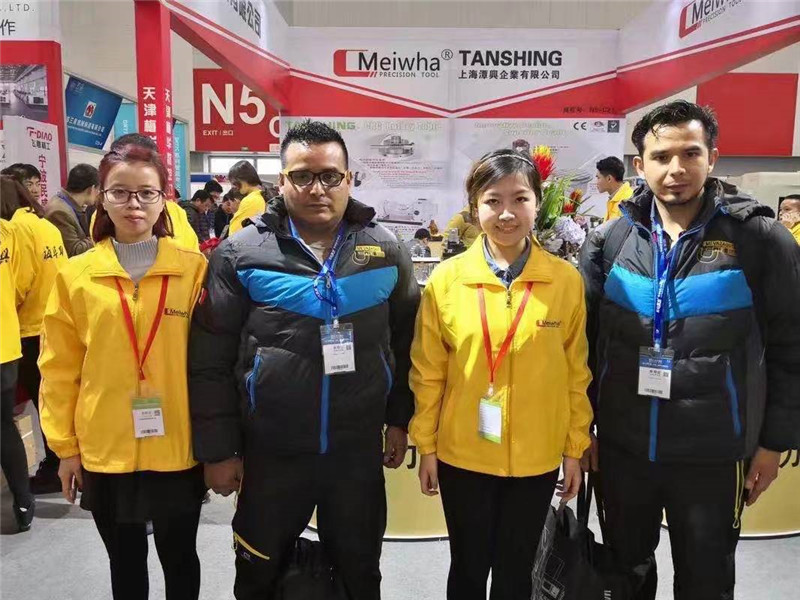
Showcasing cutting-edge CNC drilling, tapping, and shrink fit toolholding systems at major industrial expos worldwide.
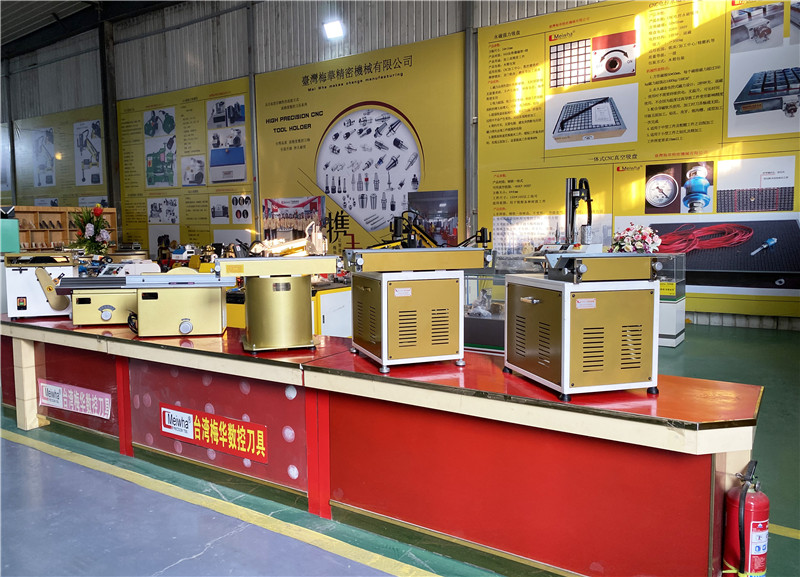
High Clamping Toolholder & Accessory Series
Explore our complete range of high-rigidity shrink fit extension rods, cooling holders, driven units, and dynamic angle heads engineered for CNC drill and tap perfection.




-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China