
Featured Precision Equipment For Induction Shrinkage Workflows
Engineered to complement high-speed HSK63A clamping cycles, modern machining centers, and automated setup cells.
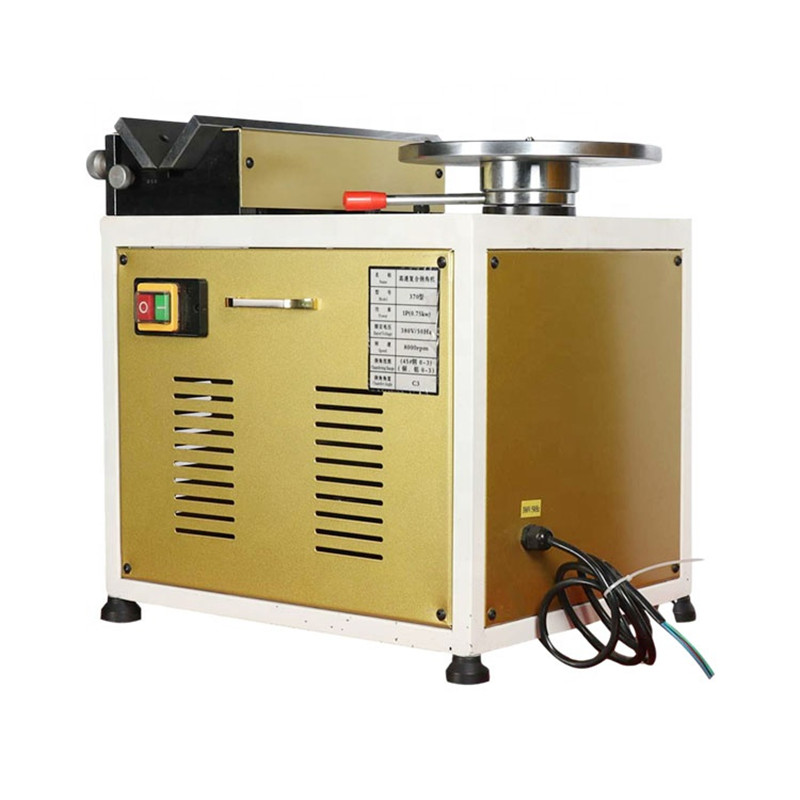
HSK63A Tool Holder Shrinkers: Evolution, Dynamics & Industrial Application
Analyzing high-frequency induction heating mechanisms and micron-grade clamping stability across aerospace, mold manufacturing, and electric mobility.
Eddy Current Optimization
Controlled electromagnetic field concentration heating the holder bore symmetrically in 3 to 6 seconds without microstructural annealing.
Sub-3-Micron Runout
Monolithic 360-degree radial clamping pressure providing uniform holding force and minimizing chatter at 24,000+ RPM spindle speeds.
Closed-Loop Thermal Control
Contactless infrared pyrometry and automated liquid cooling integration guarding tooling life through strictly managed thermal cycling.
1. Industrial Landscape: The Rise of Induction Tool Shrinkage
Modern CNC machining environments are undergoing a massive transition driven by the necessity for extreme rotational speeds, unyielding tool rigidity, and maximum operational productivity. Traditional tool holding systems—such as mechanical collet chucks, hydraulic expansion units, and set-screw side-lock systems—frequently face operational boundaries when exposed to centrifugal loads upwards of 20,000 RPM. In these intense processing environments, traditional systems exhibit tool deflection, clamping runout, and micro-slippage. The emergence of the HSK63A tool holder shrinker for induction tool shrinkage represents a decisive technological pivot. Utilizing local thermal expansion via high-frequency alternating electromagnetic fields, induction shrinkage allows operators to achieve a true interference fit between the solid carbide shank and the inner bore of an HSK-A63 toolholder. This process produces holding torques unreachable by mechanical levers and achieves dynamic balancing metrics certified up to G2.5 balance grades at rotational speeds approaching 25,000 to 30,000 RPM.
From a commercial viewpoint, contemporary manufacturing facilities across North America, Europe, and Asia are transitioning from pneumatic or resistance heating units to automated, multi-coil induction shrink platforms. High-power induction shrinkage units minimize tool change downtime from several minutes to under thirty seconds, integrating rapid air-quenching or liquid emulsion cooling collars. Consequently, spindle uptime rises substantially, eliminating human indexing errors and preserving tool setup consistency across shifts.
2. Mechanical Precision: Why HSK63A Outclasses Competing Interfaces
The HSK63A (Hohl-Schaft-Kegel DIN 69893-1) spindle taper standard has cemented itself as the international benchmark for high-speed machining centers. Its architectural brilliance lies in simultaneous dual-face contact combined with a short, hollow 1:10 taper taper design. Unlike solid steep-taper interfaces (such as conventional BT40 or CAT40 holders), which may pull deeper into the spindle under intense centrifugal force, the hollow HSK shank expands naturally under spindle rotation, maintaining uniform radial and axial positioning accuracy at all times.
When combined with induction shrinkage technology, the HSK63A interface eliminates external moving components—such as clamping nuts, drive pins, or retention knobs. The resultant uniform cross-section reduces windage resistance, lowers operational acoustic noise, and dramatically improves torsional rigidity. Machining operations executing aggressive trochoidal roughing or five-axis deep-pocket pocketing witness substantial gains in tool life—often extending cutting edge longevity by 200% to 300%—because radial runout tolerances are maintained below 0.003 mm (0.00012 inches) at 3xD overhang distances.
3. Deep-Dive Application Profiles
The technical deployment of the HSK63A tool holder shrinker spans demanding production sectors where machining failure yields severe scrap costs:
Aerospace Monolithic Milling: Machining thin-walled titanium alloy (Ti-6Al-4V) and Inconel structural spars requires minimal harmonic chatter. The monolithic slim profiles of shrink-fit HSK63A extensions facilitate deep access into structural cavities without compromising radial stiffness, drastically diminishing chatter marks and tool breakage.
Automotive & EV Stamping Molds: Large stamping dies and aluminum transmission housings require extensive 5-axis ball-nose surfacing. The consistent radial clamp of an induction-shrunk carbide toolholder guarantees seamless surface finishes (Ra < 0.2 µm), nearly eliminating labor-intensive manual polishing stages.
Medical Implant & Orthopedics: In the milling of cobalt-chrome knee joints and PEEK bone plates, micro-tools cannot tolerate runout errors. Induction shrinkage units furnish sub-micron repeatability across small bore sizes (Ø3mm to Ø6mm), ensuring critical geometric accuracy.
4. Future Trajectories: AI Integration and Smart Induction Systems
The convergence of Industry 4.0 and machine tool accessory engineering is rapidly transforming induction tool shrinkers into intelligent, networked devices. Modern HSK63A shrinker machines now leverage AI-assisted heating parameter libraries and optical tool recognition cameras. By scanning the external silhouette or reading an integrated RFID data chip embedded within the HSK63A holder, intelligent shrink stations automatically dial in the exact induction frequency, coil position, target temperature (generally 280°C–320°C), and liquid cooling dwell time. This fully automates the cycle, preventing operator-induced overheating, protecting the metallurgical integrity of the specialized tool steel, and ensuring indefinitely repeatable shrink-unshrink cycles.
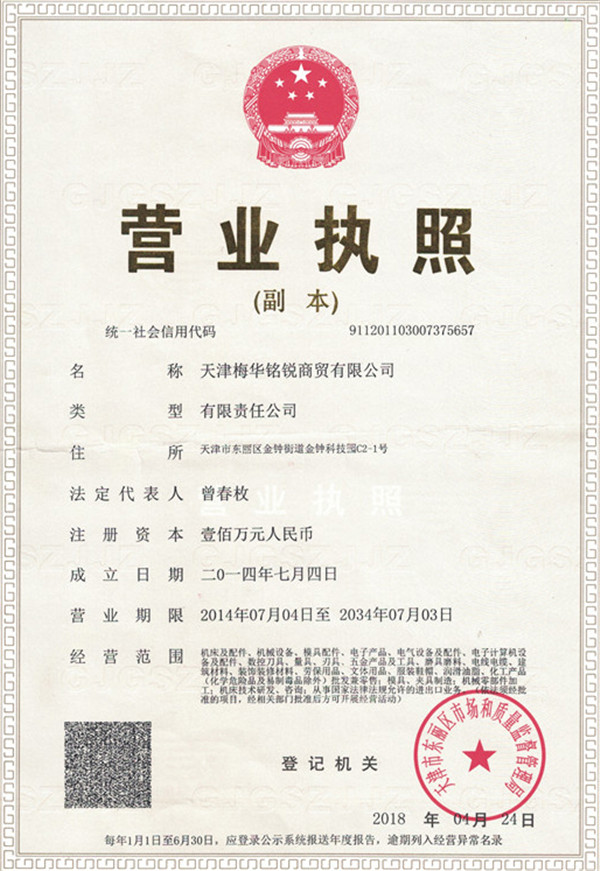
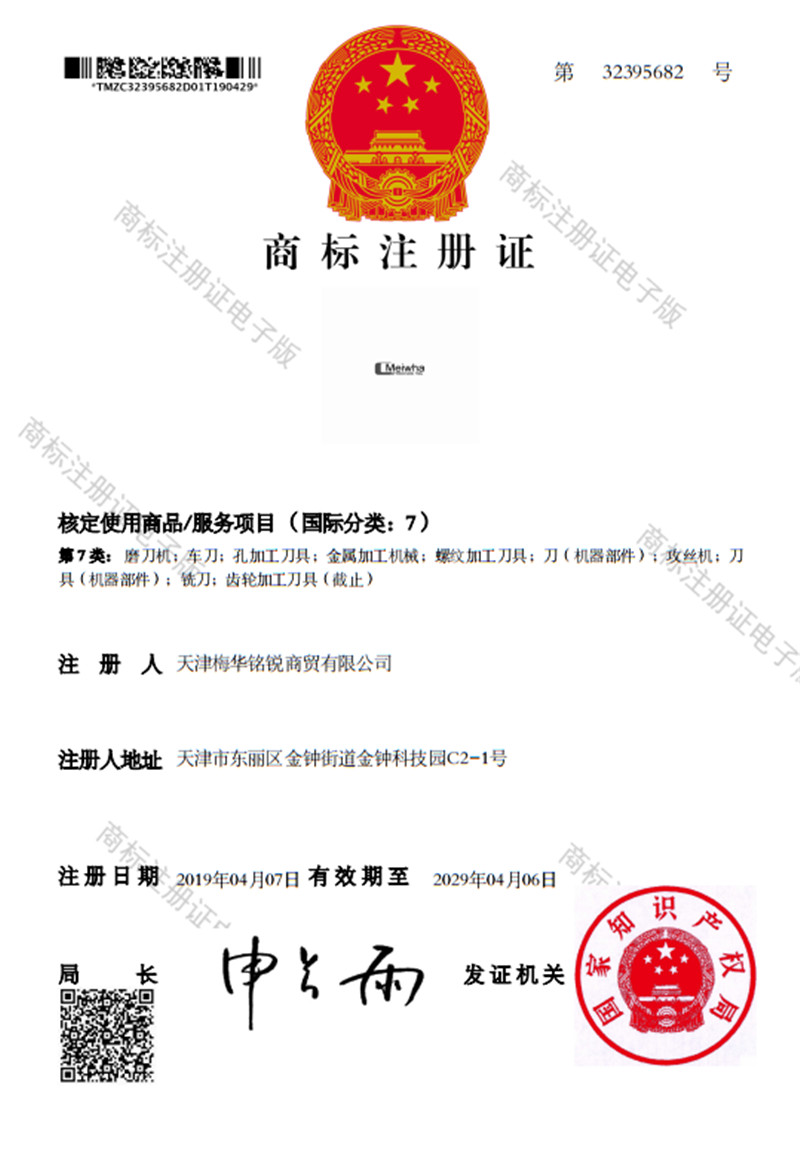
Tianjin MeiWha Precision Machinery Co., Ltd.
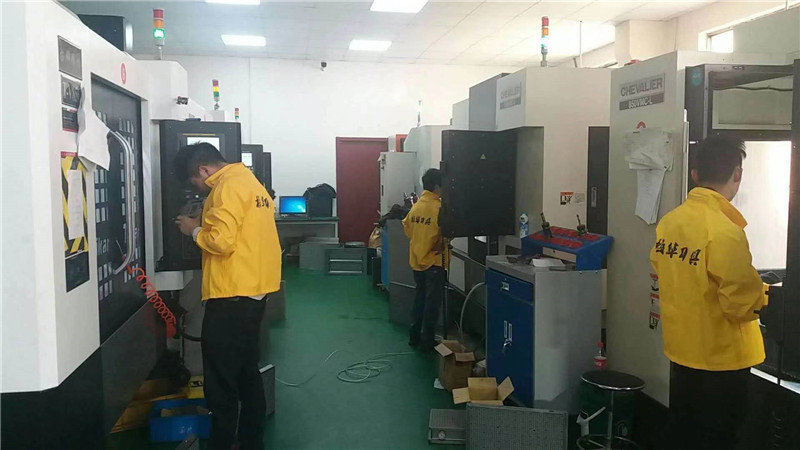
Tianjin MeiWha Precision Machinery Co., Ltd was founded in June 2005. It is a professional manufactory engaged in all kinds of NC cutting tools, including Milling tools, Cutting Tools, Turning Tools, Tool holders, End Mills, Taps, Drills, Tapping Machines, End Mill Grinder machines, Measuring tools, Machine tool accessories, and other industrial products.
Combining industry advantages, our enterprise integrates deep manufacturing resources and adheres to a customer-oriented approach, providing end-to-end tooling procurement and bespoke machining solutions globally.
Global Location & Export Presence
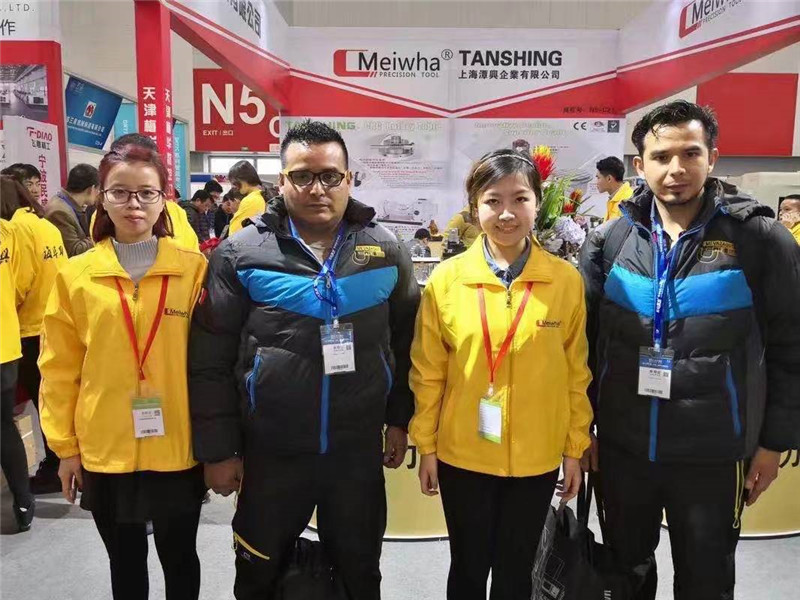
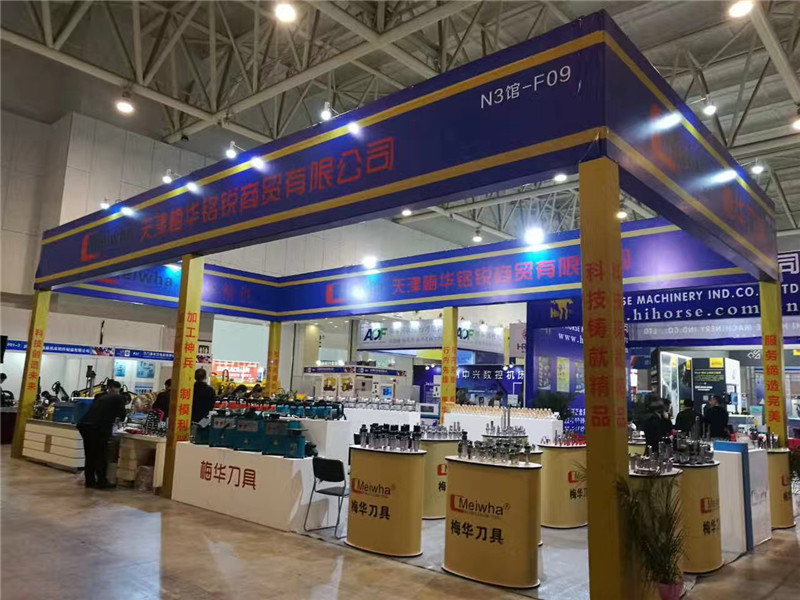
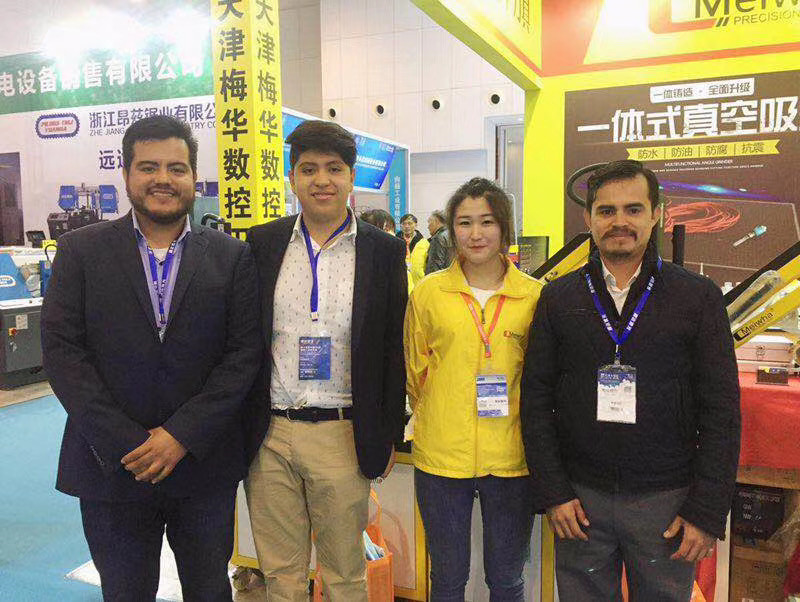
Our company is located in Jingzhong Industrial park, Dongli District, Tianjin, covering an area of more than 5,000 square meters, with 1,500 square meters of modern office space. Branches, direct stores, subordinate branch agents, or specialized distributors are arranged across domestic and international markets. MeiWha products are widely exported to Dubai, The United Arab Emirates, Switzerland, France, South Africa, India, The Philippines, Thailand, and across Europe and the Americas.
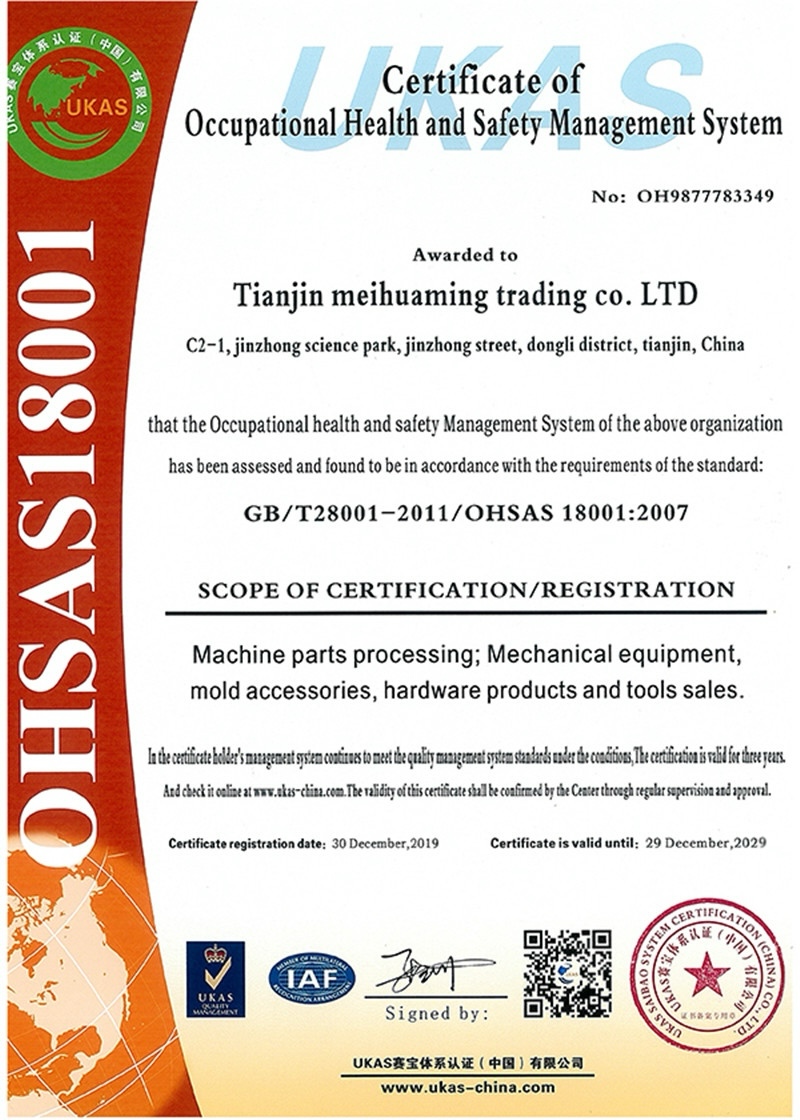
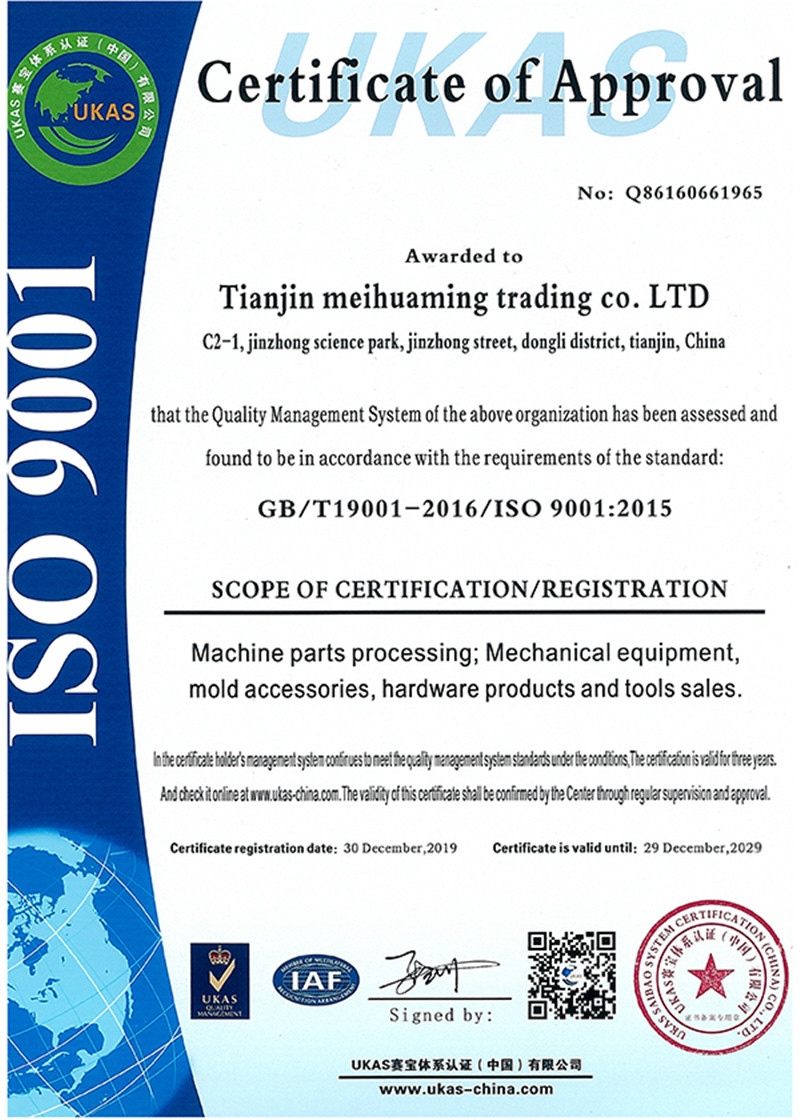
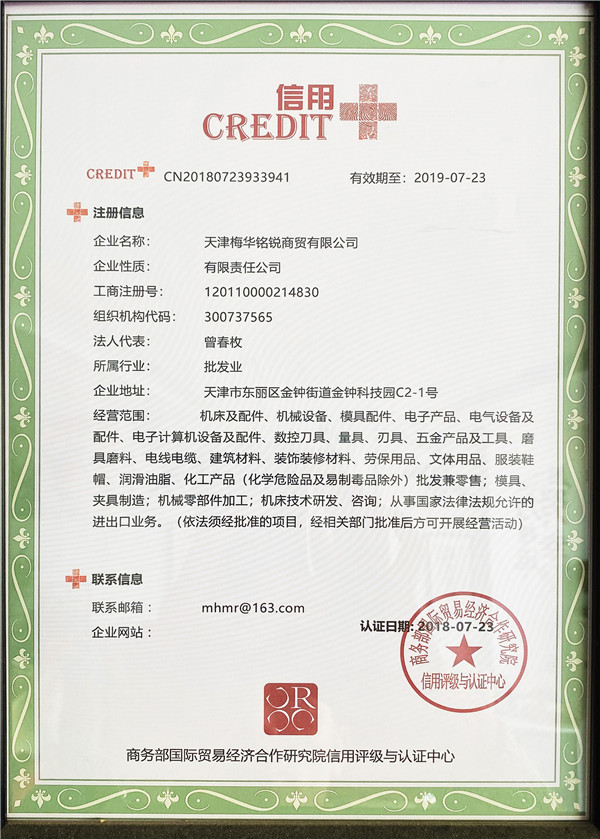
Uncompromising Quality Standards
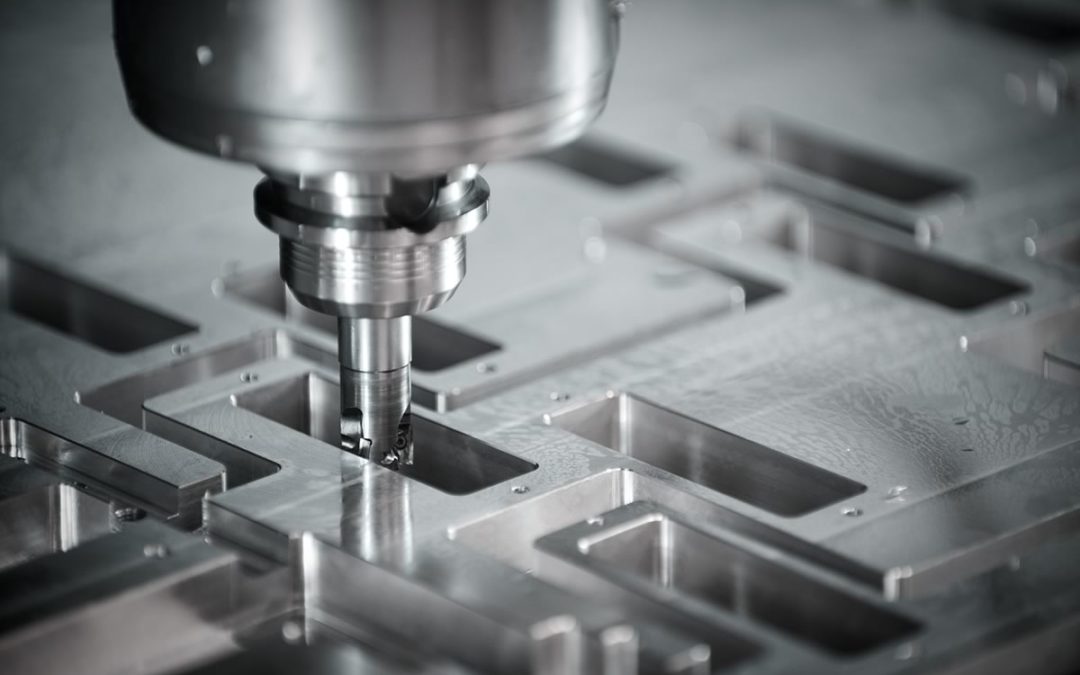
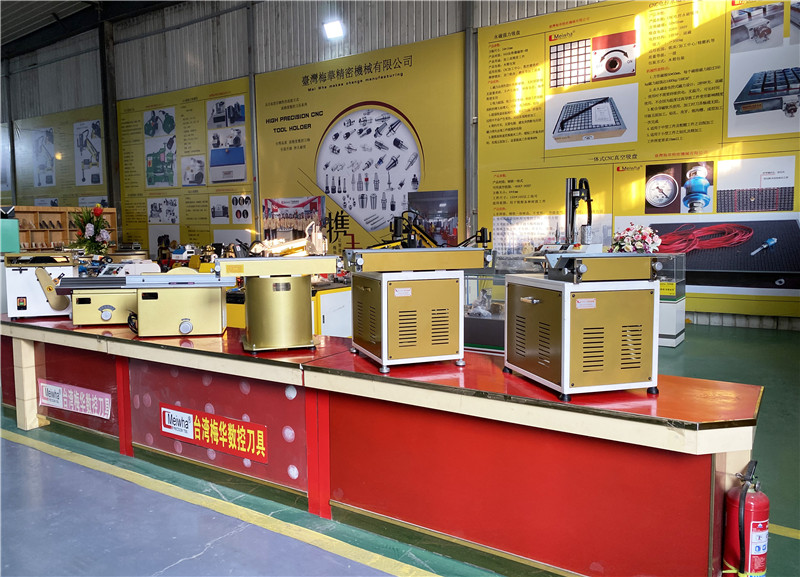
Our standard tools meet the highest quality standards, which we have proven millions of times to satisfied customers since 2005. With our mature product portfolio, we deliver comprehensive solutions for drilling, milling, countersinking, and reaming. We continuously optimize our solid carbide lines and shrink-fit tool accessories to ensure exceptional concentricity, structural durability, and peak machining availability.
International Exhibitions & Strategic Cooperation
Establishing strategic industrial alliances with prominent research institutes including Tianjin Jinhang Institute of Physics and Beijing Fangshan Bridge 14th Bureau.
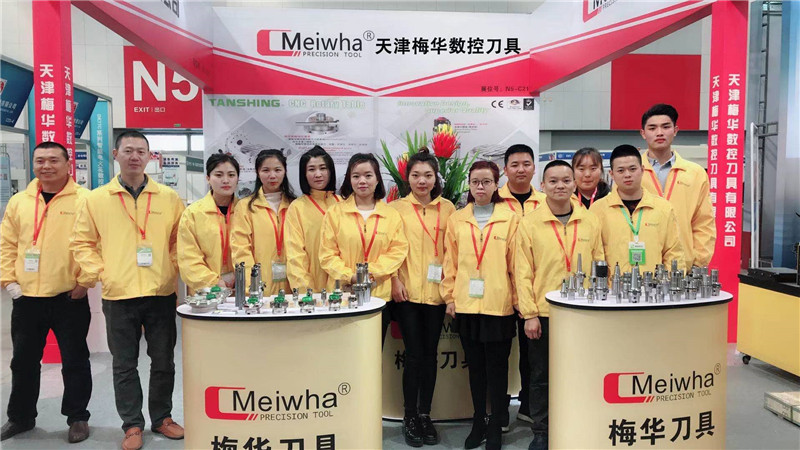
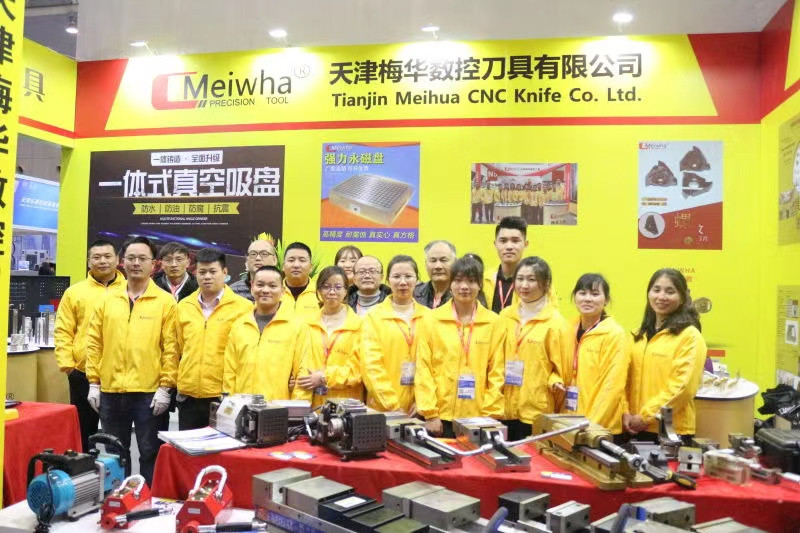
OUR LATEST TOOLING PRODUCTS
Explore our flagship high-precision tooling catalog, engineered for CNC centers and high-speed shrink systems.


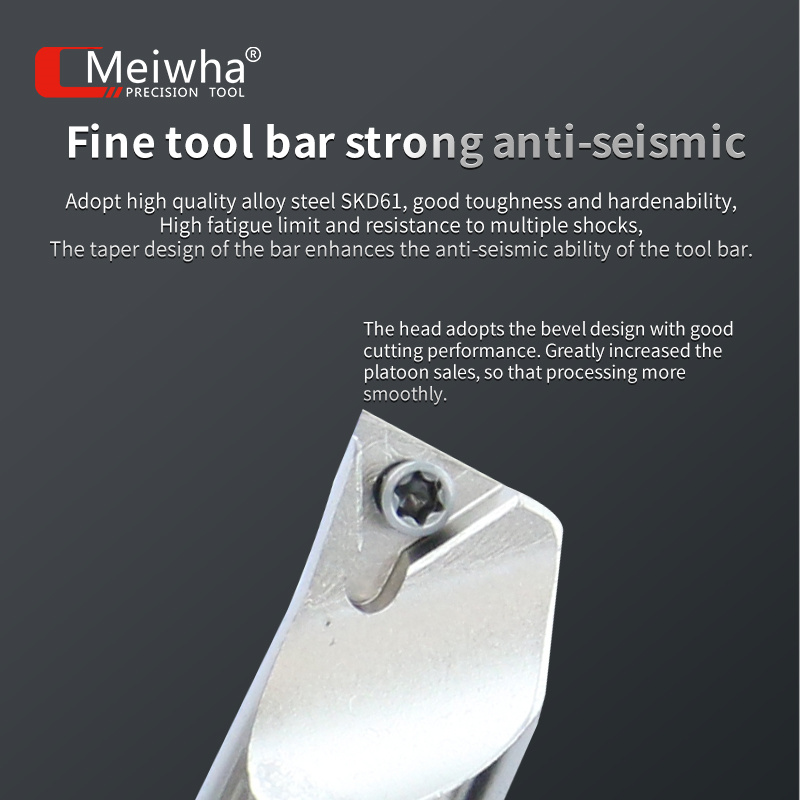 H•BOR Micro-Finishing Fine Boring Set
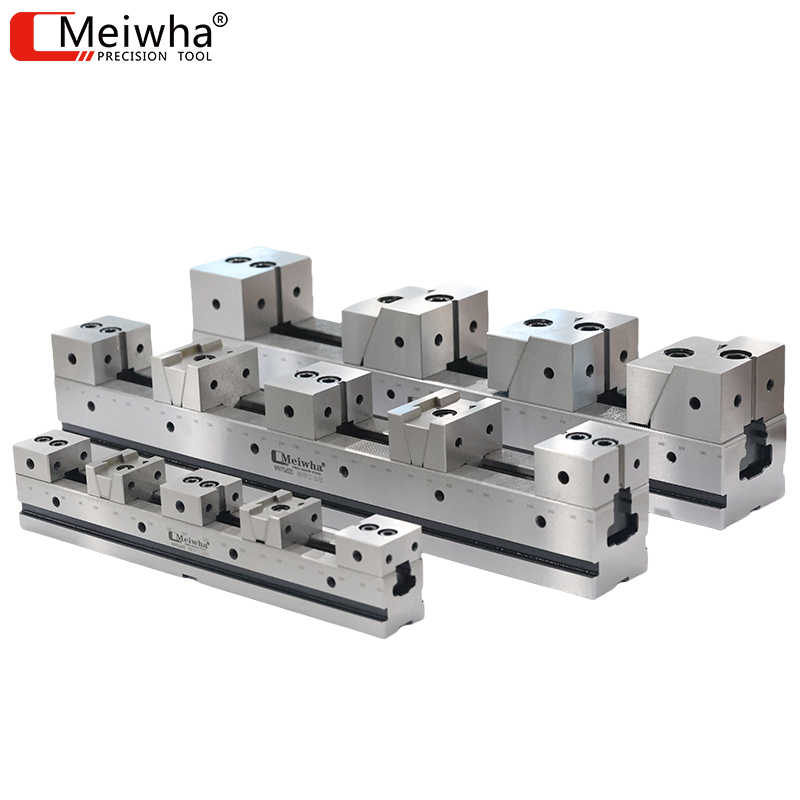 CNC Machining Center Multi-Station Precision Vise Mechanical Vice


-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China