
Featured High-Performance Tooling Solutions
Engineered for maximum rigidity, ultra-low runout, and relentless manufacturing cycles across high-speed spindle operations.
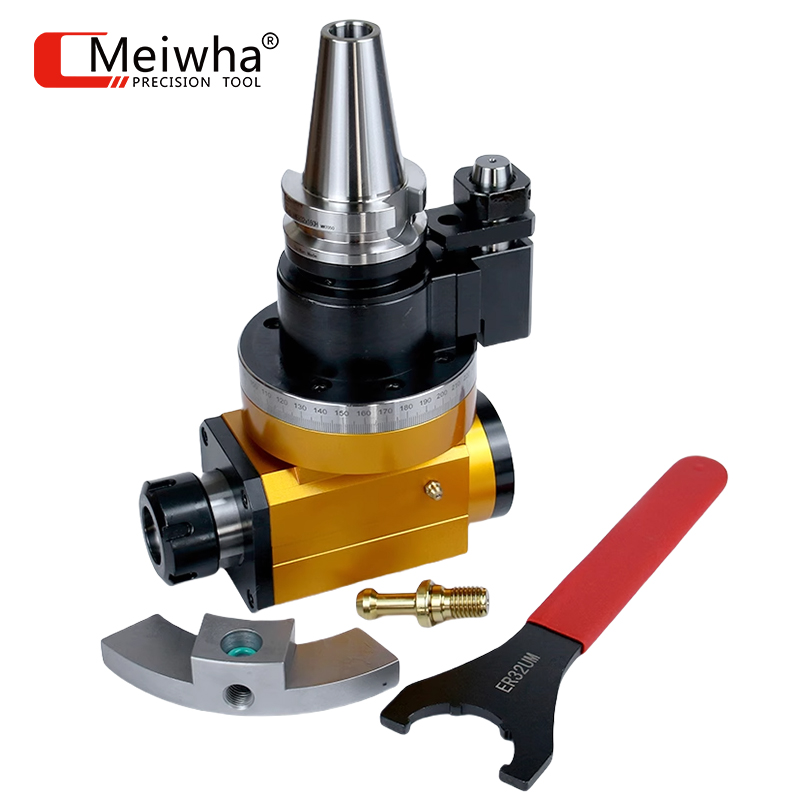
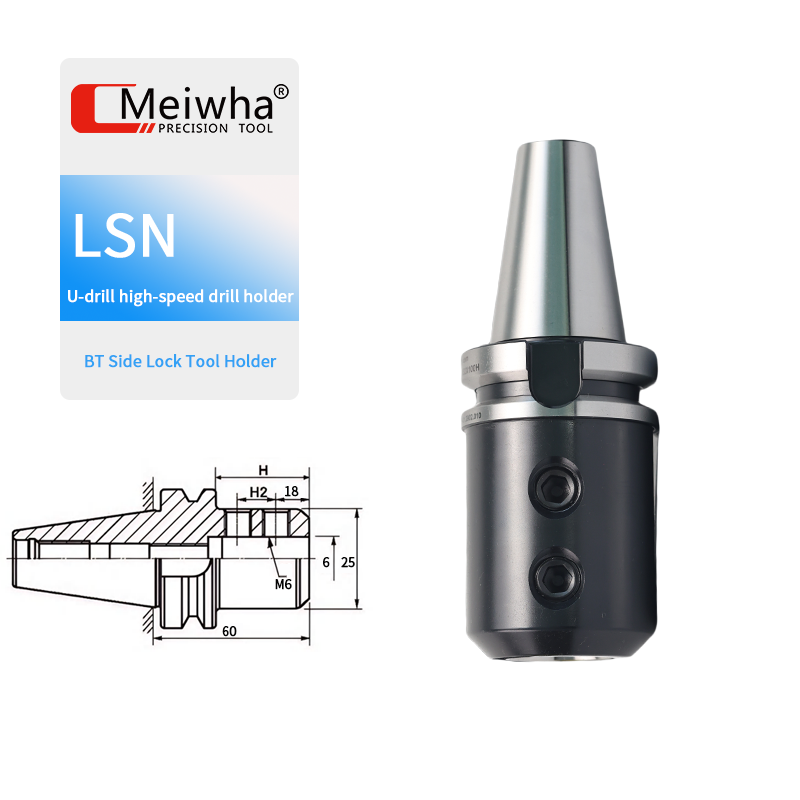
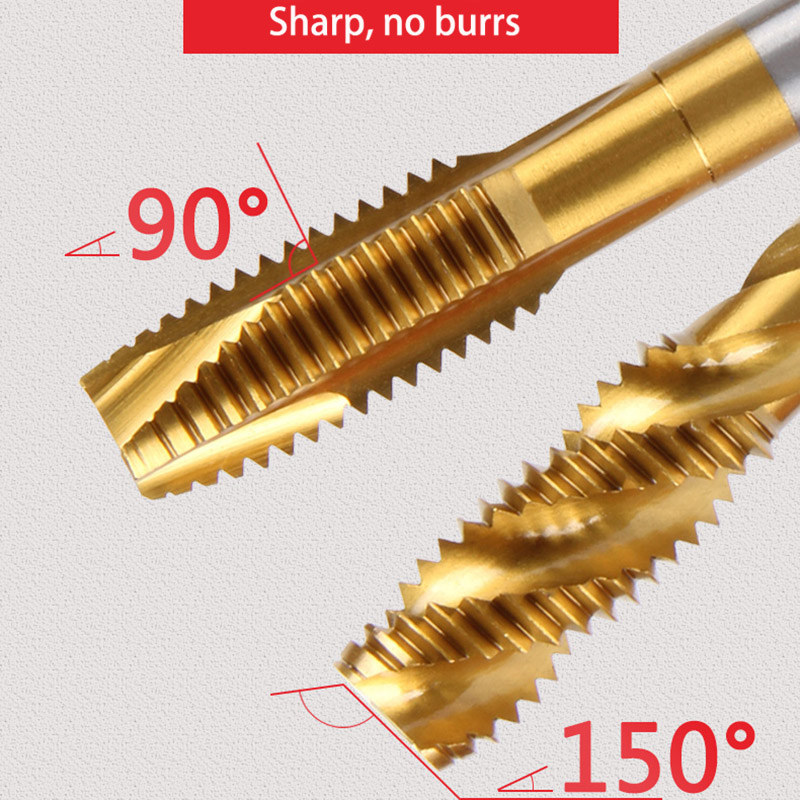
Industrial Landscape of HSK63A Shrink Fit Systems in the United Kingdom
Examining supply chain trends, technical adoption, and regional manufacturing dynamics across British industry hubs.
The Shift Toward HSK-A63 Tool Clamping in Modern British Manufacturing
In the United Kingdom, precision engineering has been experiencing an aggressive transformation under Industry 4.0 paradigms. Among high-speed machining (HSM) centers, the HSK-A63 spindle interface paired with thermal induction shrink fit machines has become the undisputed gold standard. With manufacturing corridors across the West Midlands, South Yorkshire, and the aerospace clusters of the South West (such as Bristol and Filton) demanding higher feed rates and microscopic surface finishes, conventional collet chucks frequently falter due to centrifugal deflection and harmonic vibrations.
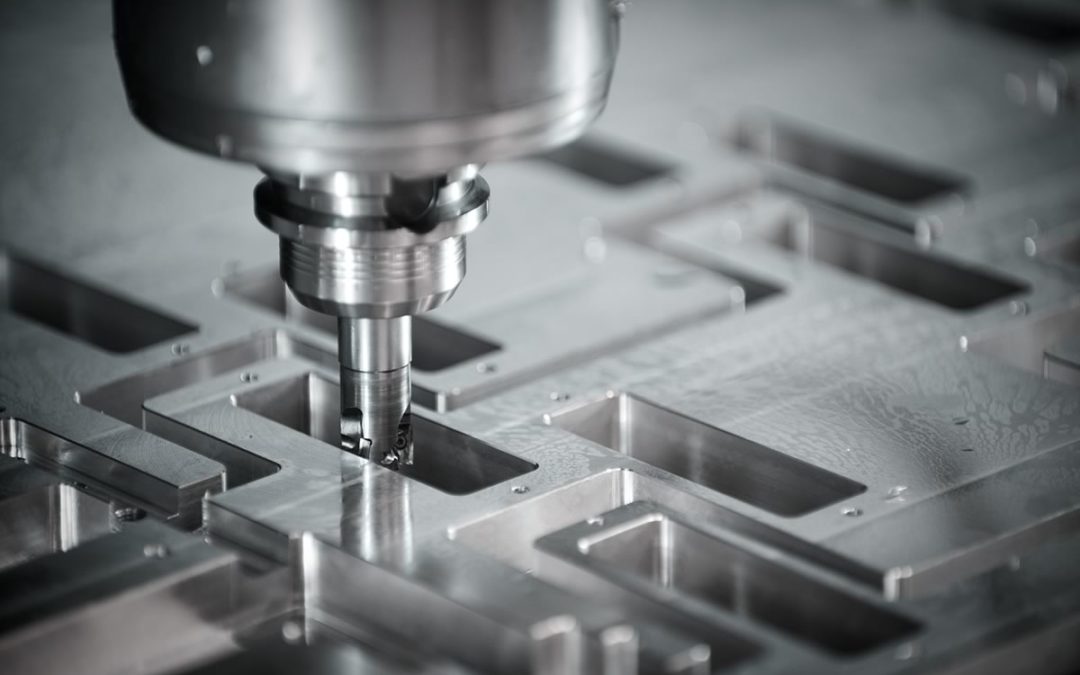
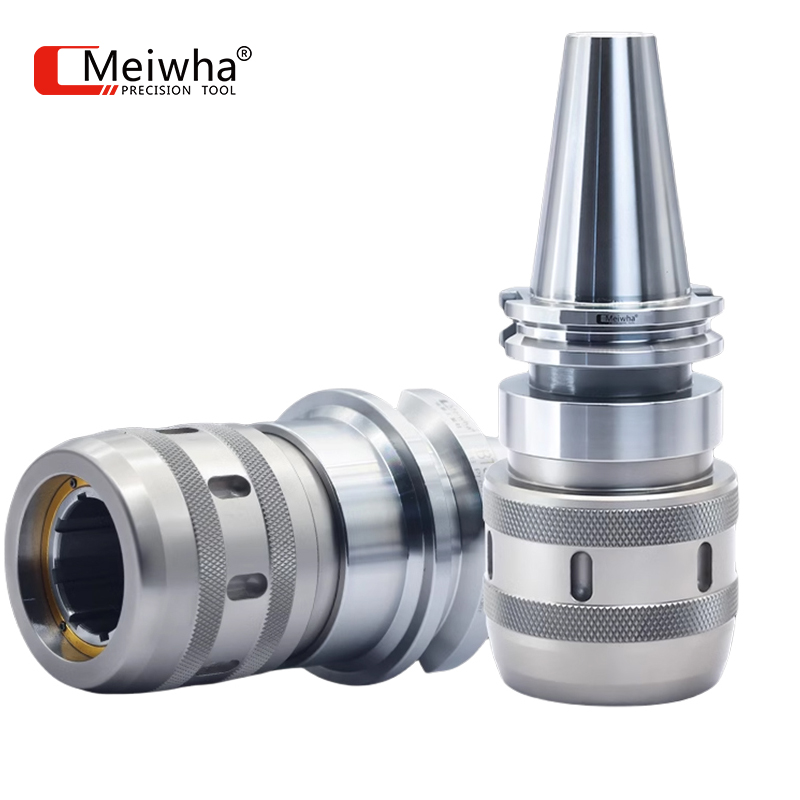
HSK63A tool holder shrinker units utilize high-frequency electromagnetic induction to heat the bore of the tool holder uniformly within seconds. As the holder thermal bore expands, cutting tool shanks—crafted from solid carbide or heavy metal—are seamlessly loaded. Once rapidly cooled via liquid chilled jackets or forced air systems, the holder contracts with tremendous symmetric radial gripping pressure. This process produces concentricity and total indicator reading (TIR) runout below 0.003 mm, allowing British machine shops to run 5-axis DMG MORI, Mazak, and Hermle machines at 20,000+ RPM without chatter.
Micron-Level Runout Precision
Delivers repeatable runout under 3 microns at 3xD overhang, doubling carbide tool life and safeguarding costly machine spindles against unbalanced centrifugal forces.
Induction Speed & Efficiency
Microprocessor-driven heating cycles complete in 3 to 7 seconds, complemented by intelligent cooling stations to ensure immediate tool setup turnaround on the shop floor.
Symmetrical Dynamic Balance
The completely rotation-symmetrical profile of HSK63A shrink fit chucks avoids collet nuts or set-screws, eliminating vibrations at feeds surpassing 18,000 RPM.
Localized Commercial Applications Across Key UK Industrial Hubs
Understanding the UK commercial ecosystem requires analyzing regional industrial specialization where HSK63A shrinkers are deployed:
- Aerospace & Defense (Derbyshire, Lancashire, Bristol): Titanium 6Al-4V airframe ribs, Inconel turbine discs, and structural spars machined on massive multi-axis gantries demand extreme clamping torque to combat tool pull-out under heavy chip loads.
- Motorsport & Formula 1 (The UK Motorsport Valley - Oxfordshire, Northamptonshire): Rapid prototyping of transmission casings, suspension uprights, and aerodynamic molds where cycle times are constrained and tolerances down to ±0.005 mm are non-negotiable.
- Medical Device Manufacturing (Sheffield & Leeds): Orthopedic implants, titanium knee joints, and cobalt-chrome bone plates rely on slender HSK63A shrink contours to prevent fixture interference in compact 5-axis working envelopes.
- Precision Tool & Die (West Midlands): Deep-pocket mould cavitation requiring extended shrink-fit extension rods without losing rigidity or inducing chatter marks.
| Clamping Technology | Typical Runout (TIR @ 3xD) | Max Balance Speed (RPM) | Holding Torque Efficiency | Nose Clearance Profile |
|---|---|---|---|---|
| HSK63A Induction Shrink Fit | < 0.003 mm (3 μm) | Up to 40,000 RPM (G2.5) | Ultra-High (Uniform 360° Friction) | Ultra-Slim Contour / Deep Pocket Access |
| Standard ER32 Collet Chuck | < 0.015 mm (15 μm) | Up to 12,000 RPM | Moderate (Friction-nut dependent) | Bulky nut diameter, fixture collisions |
| Weldon Side-Lock Holder | < 0.020 mm (20 μm) | Up to 8,000 RPM (Unbalanced) | Positive stop (Prone to deflection) | Asymmetrical nose, heavy centrifugal bias |
| Hydraulic Expansion Chuck | < 0.004 mm (4 μm) | Up to 25,000 RPM | High (Fluid chamber bounded) | Moderate (Bulky internal oil bladder) |
Tianjin MeiWha Precision Machinery Co., Ltd.
Global Manufacturing Powerhouse of Advanced NC Cutting Tools, Tool Holding Systems, and Machine Accessories.
Precision Engineering Heritage Since 2005
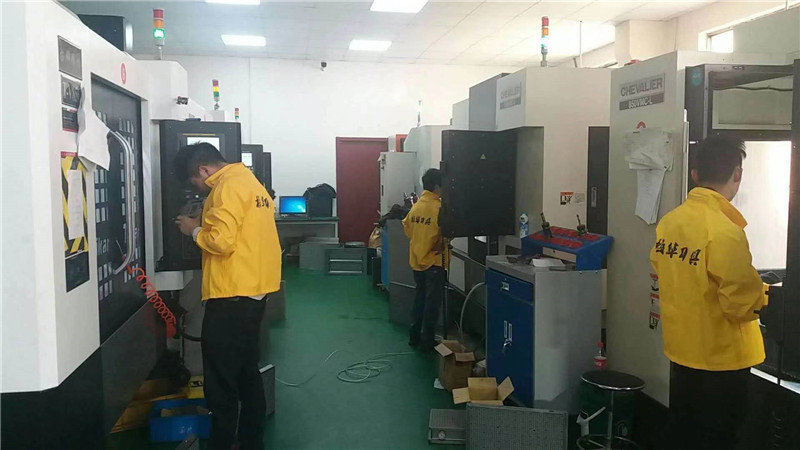
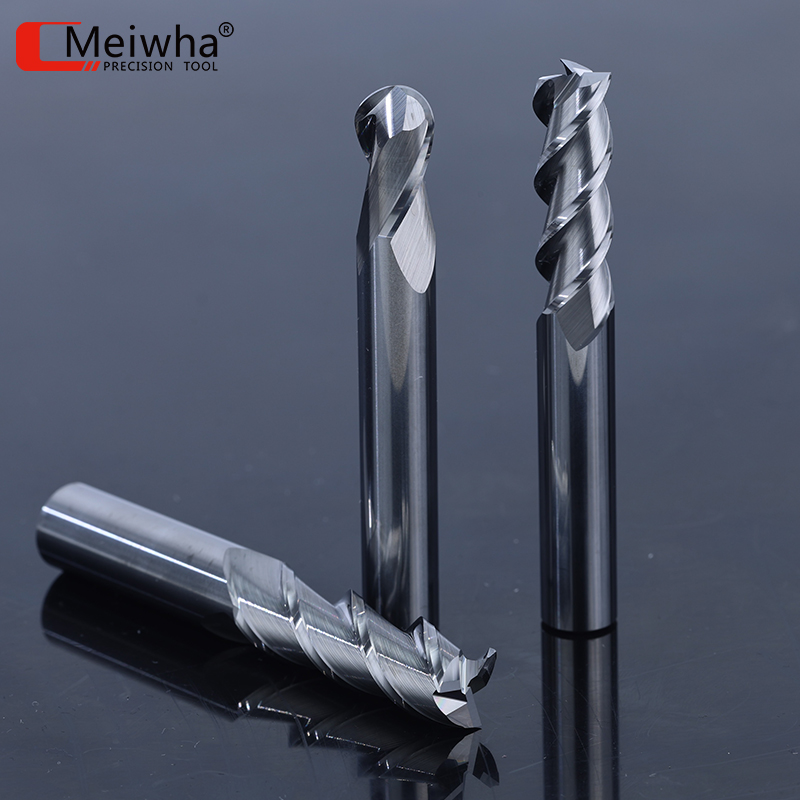
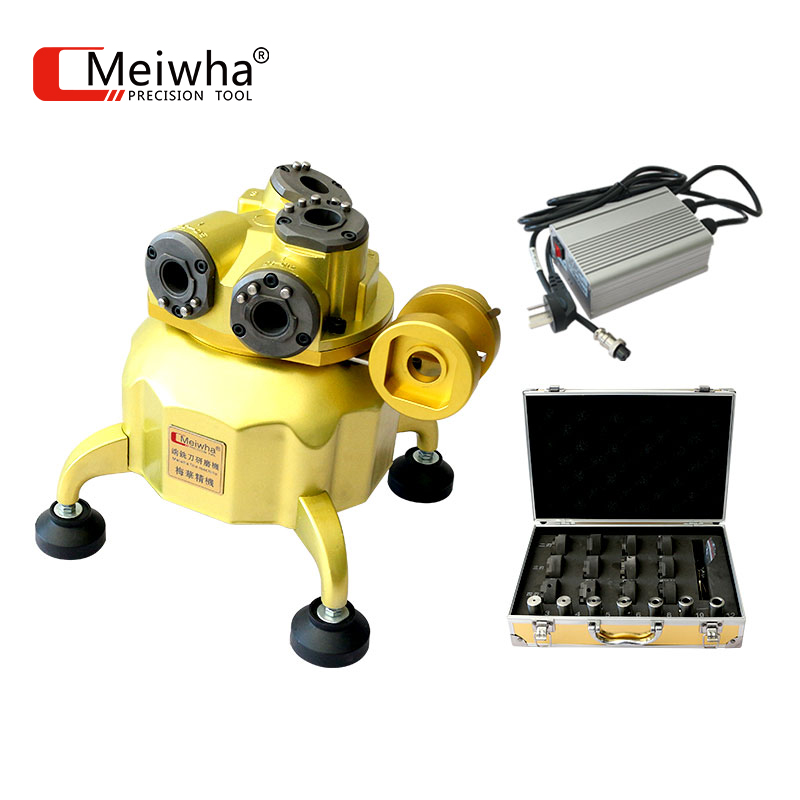
Tianjin MeiWha Precision Machinery Co., Ltd. was established in June 2005. It has developed into a premier specialized factory engaged in all kinds of NC cutting tools, including Milling tools, Cutting Tools, Turning Tools, Tool holder systems, End Mills, Taps, Drills, Tapping Machines, End Mill Grinder machines, Measuring tools, Machine tool accessories, and high-performance HSK clamping units.
Covering an expansive operating area of more than 5,000 square meters with modern research and administrative suites totaling 1,500 square meters, MeiWha delivers industrial reliability to clients throughout the UK, Switzerland, France, the UAE, South Africa, India, and Southeast Asia.
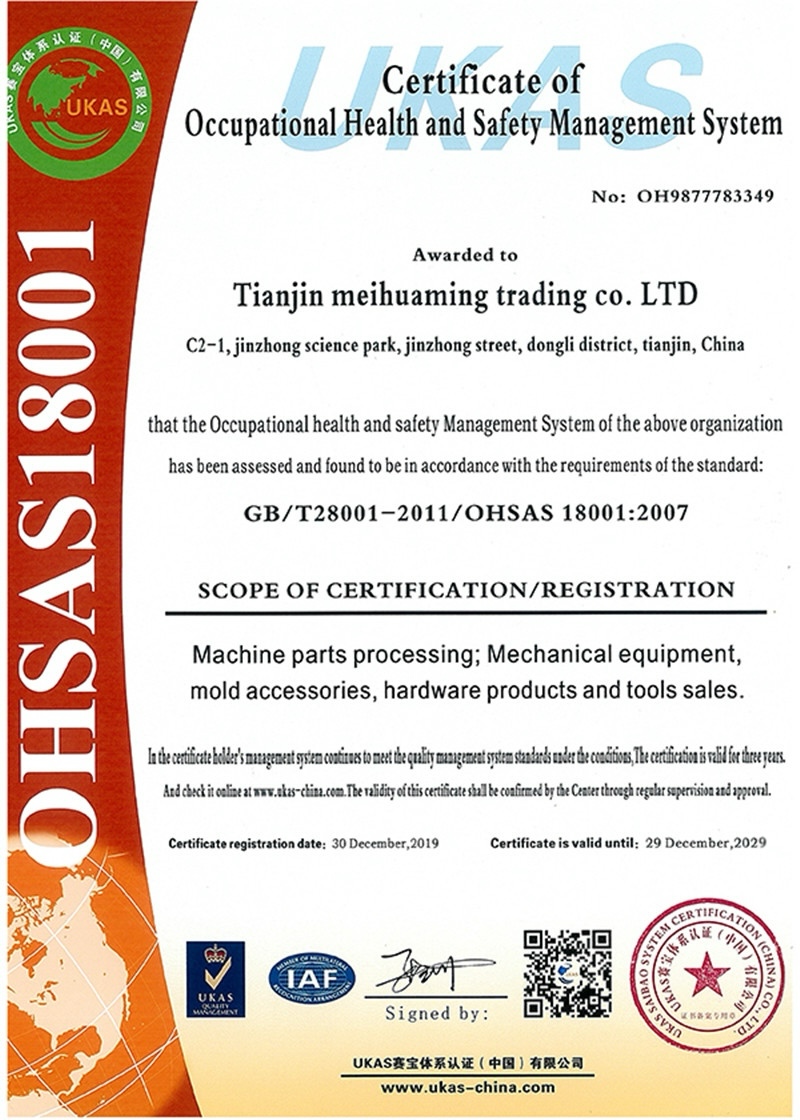
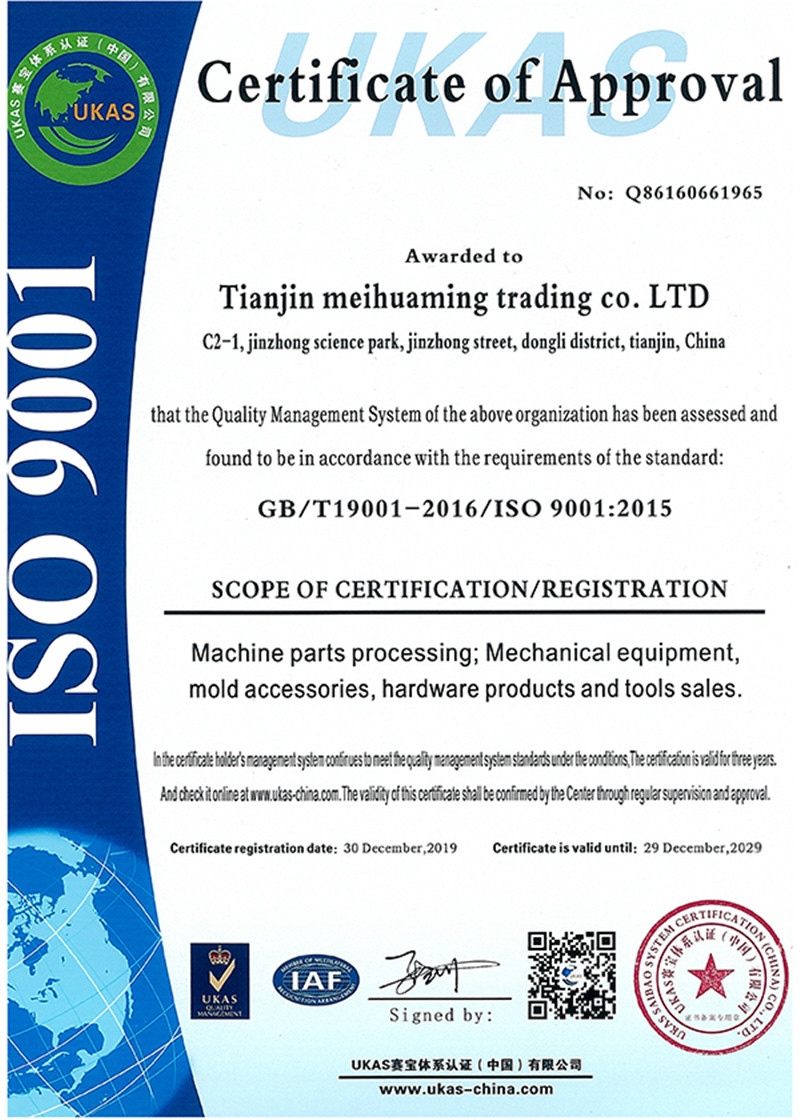
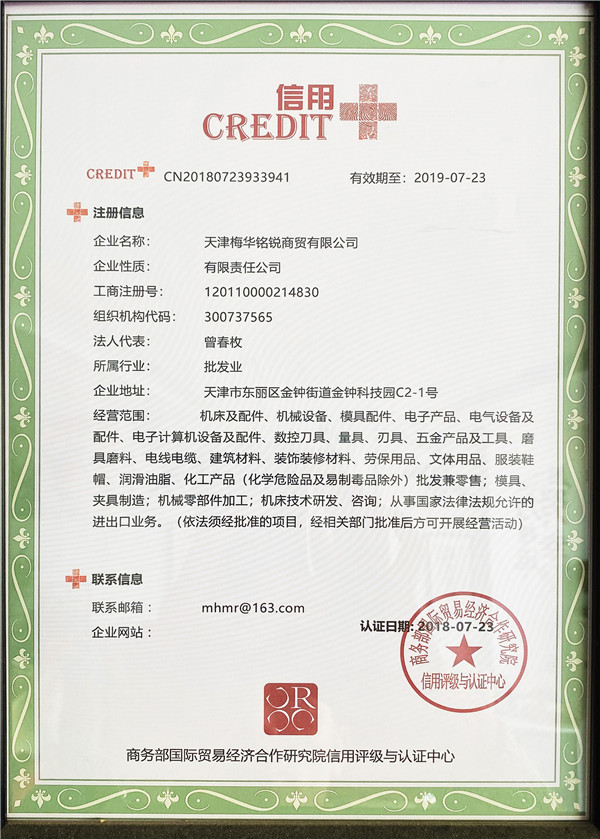
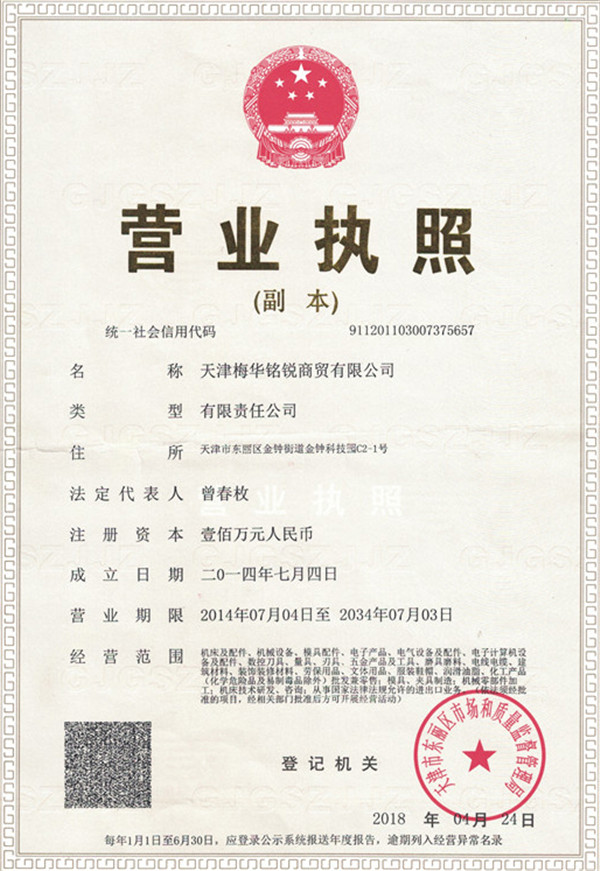
Uncompromising Quality Control & Global Standards
Our standard tools meet the highest international quality standards, which we have been able to prove millions of times to satisfied customers since 2005. With our mature product portfolio we offer complete, robust solutions for tasks surrounding drilling, milling, countersinking, and reaming. With steady dedication and technological ambition, we continue to develop and optimize our solid carbide tool lines and high-precision holder series.
MeiWha combines industry advantages, integrates advanced product resources, and adheres to customer-oriented manufacturing principles—providing clients with one-stop procurement solutions, dependable delivery schedules, and strictly competitive factory-direct pricing. Strategic collaborations with research institutes such as the Tianjin Jinhang Institute of Physics reflect our continuous commitment to innovation.

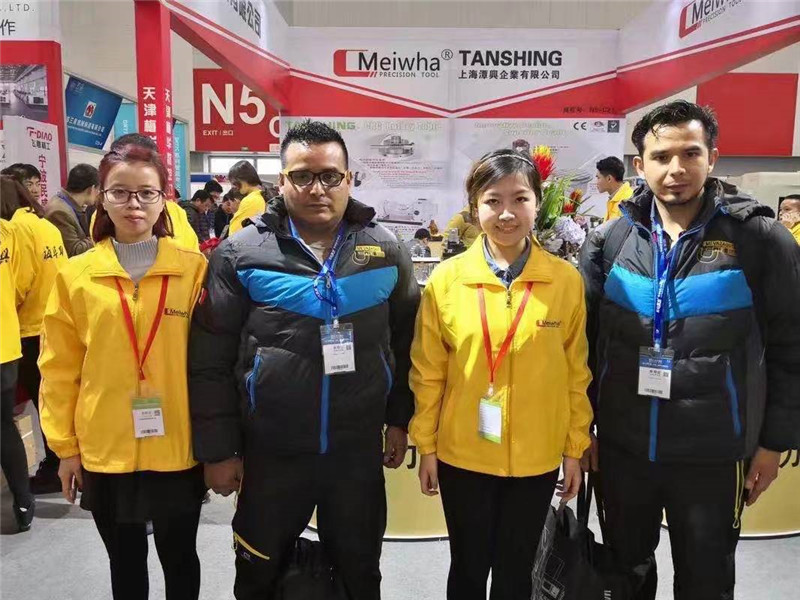
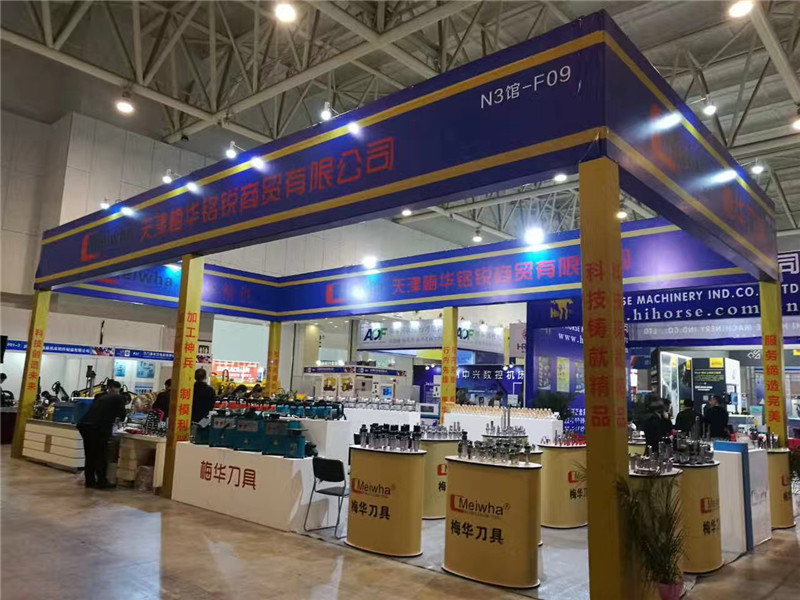
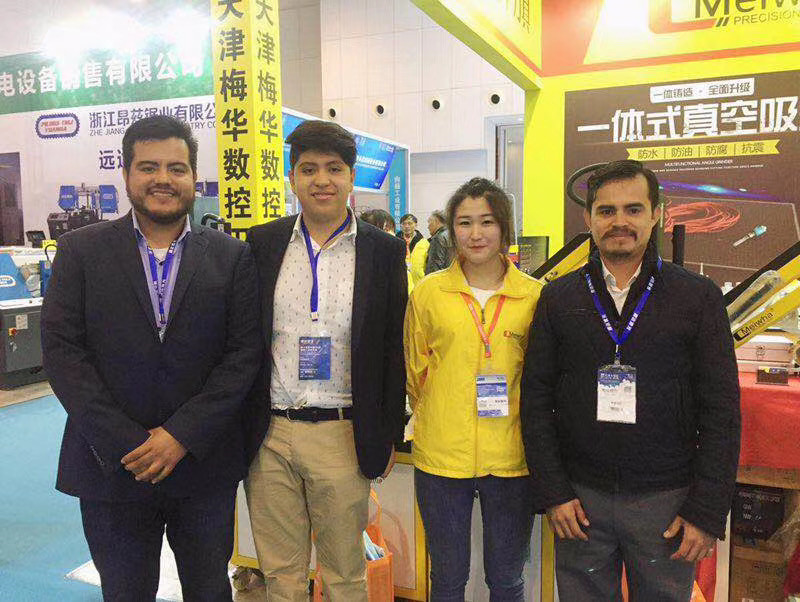
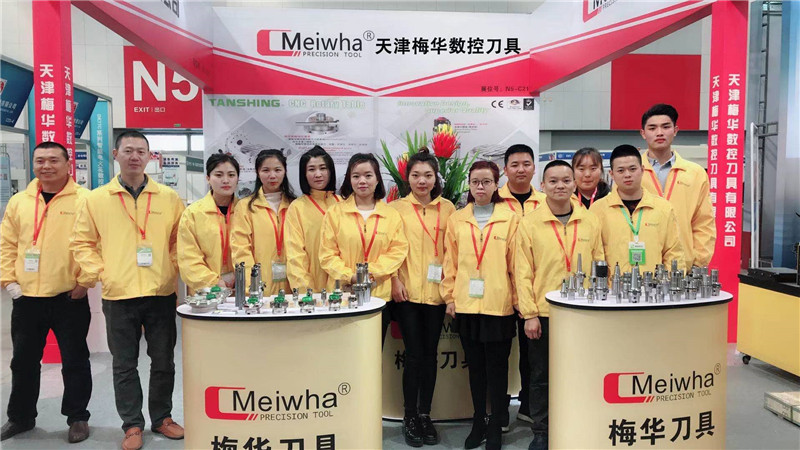
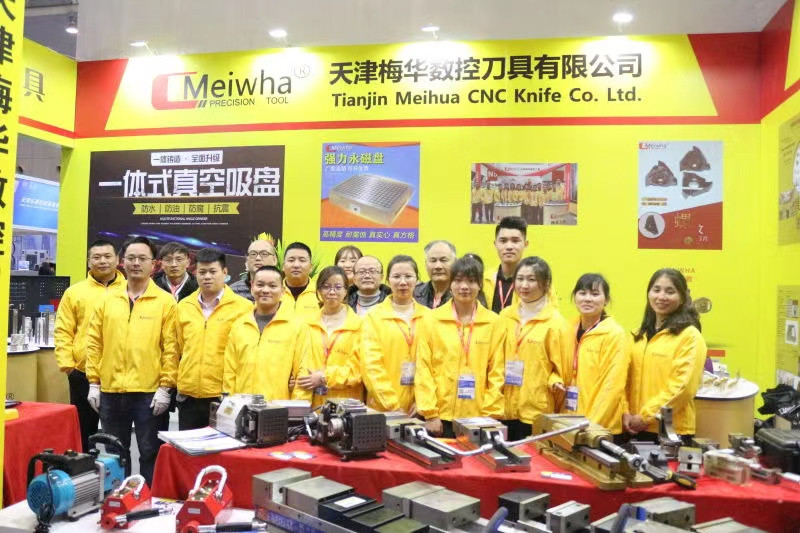
International Industrial Exhibitions & Global Presence
Connecting with European and British partners at premier global tooling expos and manufacturing conventions.
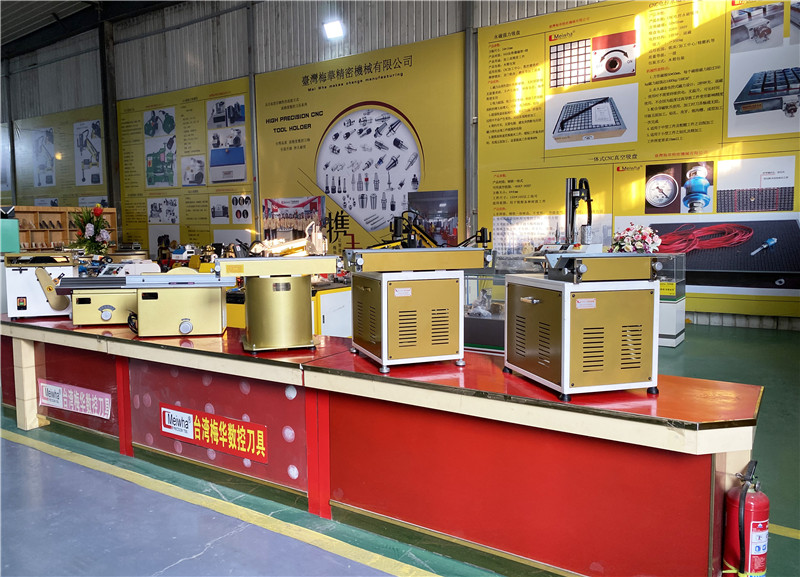
Precision Tooling & Workholding Essentials
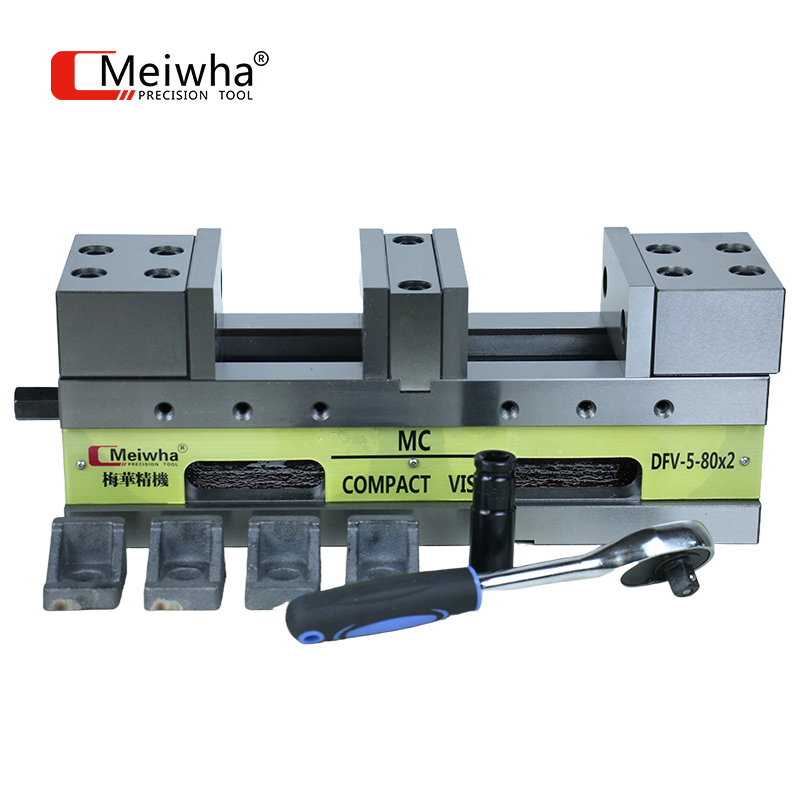
High-precision clamping and cutting solutions complementing modern HSK and CNC spindle applications.
Future Outlook: Smart Induction Shrinking in UK Industry 4.0
Predictive thermal heating, parameter databases, and carbon footprint reduction on the shop floor.
As British engineering operations focus on lean manufacturing, the selection of an HSK63A tool holder shrinker is no longer just an equipment purchase—it is a strategic productivity investment. The UK tooling market is adopting shrink-fit systems engineered with distinct advantages:
1. Intelligent Coil Geometries: Modern shrink machines incorporate adaptable multi-coil inductors that automatically adjust heating parameters to match tool holder shank diameters (ranging from 3 mm to 32 mm). This prevents overheating, preserves the metallurgic temper of tool holders, and extends chuck life past thousands of thermal cycles.
2. Energy Optimization & Operator Safety: British health and safety (HSE) regulations favor induction shrink systems that feature contactless heating and integrated fluid cooling bells, ensuring hot cutting tools cannot be touched inadvertently while slashing overall factory energy usage compared to prolonged hot-air ovens.
3. Closed-Loop Tool Presetting: Combining tool shrinking with optical z-axis presetters allows workshops across the UK to set exact tool projections down to micron accuracy, eliminating manual calibration on machining centers and maximizing spindle uptime.
Our Latest Products & CNC Spindle Tooling Portfolio
Discover our comprehensive range of high-efficiency tool holders, shrink components, driven units, and accessories.




-
Taiwan head office: No. 138-198, Xing'an Road, Zhuangmeili, Dajia District, Taichung City, Taiwan台中市大甲區莊美里興安路138之198號Branch office: No.8 Baisui Science Industrial park,Haihang West Road,Ninghe District,Tianjin,China